Updated: 2026 Tooling Guide · By Sailwin Blow Mold Division
PET Bottle Blow Mold: Aircraft Aluminum 7075 vs Stainless Steel S136
Selecting the wrong mold alloy for stretch blow molding leads to severe production compromises: choose heavy steel for high-speed water bottles and your blowing cycle time increases by 1.2 to 2.0 seconds per bottle due to sluggish thermal transfer; choose low-grade aluminum for 40-bar carbonated beverage containers and cavity parting lines deform after barely a million cycles. When beverage converters procure pet blow molds, balancing thermal conductivity against mechanical wear resistance is the central engineering decision.
At Sailwin, our toolroom engineers have fabricated over 3,000 cavity sets for rotary and linear stretch blow molding machines across 0.2L to 20L containers. We understand the precise operational trade-offs between aircraft-grade 7075-T6 aluminum and vacuum-hardened S136 stainless steel—and how hybrid composite designs combine the thermal velocity of aluminum with the indomitable lifespan of hardened steel.
This technical guide provides manufacturing directors and packaging plant managers with a comprehensive metallurgical breakdown—evaluating thermal dissipation rates, cycle time optimization, surface coatings, and lifecycle total cost of ownership.
Key Takeaways
- 5x Higher Thermal Conductivity in 7075 Aluminum: At 130 W/m·K versus 26 W/m·K for tool steel, 7075-T6 aluminum freezes molten PET against cavity walls in under 0.8 seconds, boosting daily machine output by 15% to 22%.
- Steel S136 Delivers 15M+ Ultra-Long Lifecycles: For continuous round-the-clock lines requiring zero parting line maintenance over a decade, vacuum-hardened S136 (HRC 52) provides unbeatable abrasion resistance.
- Hybrid Composite Construction Wins ROI: Combining a 7075 aluminum cavity shell with a hardened stainless steel base insert delivers maximum thermal speed with indestructible petaloid wear resistance.
Designing a new PET bottle shape or sizing blow molds?
Sailwin engineers custom 1 to 8-cavity blow molds compatible with Sidel, Krones, and linear blowers.
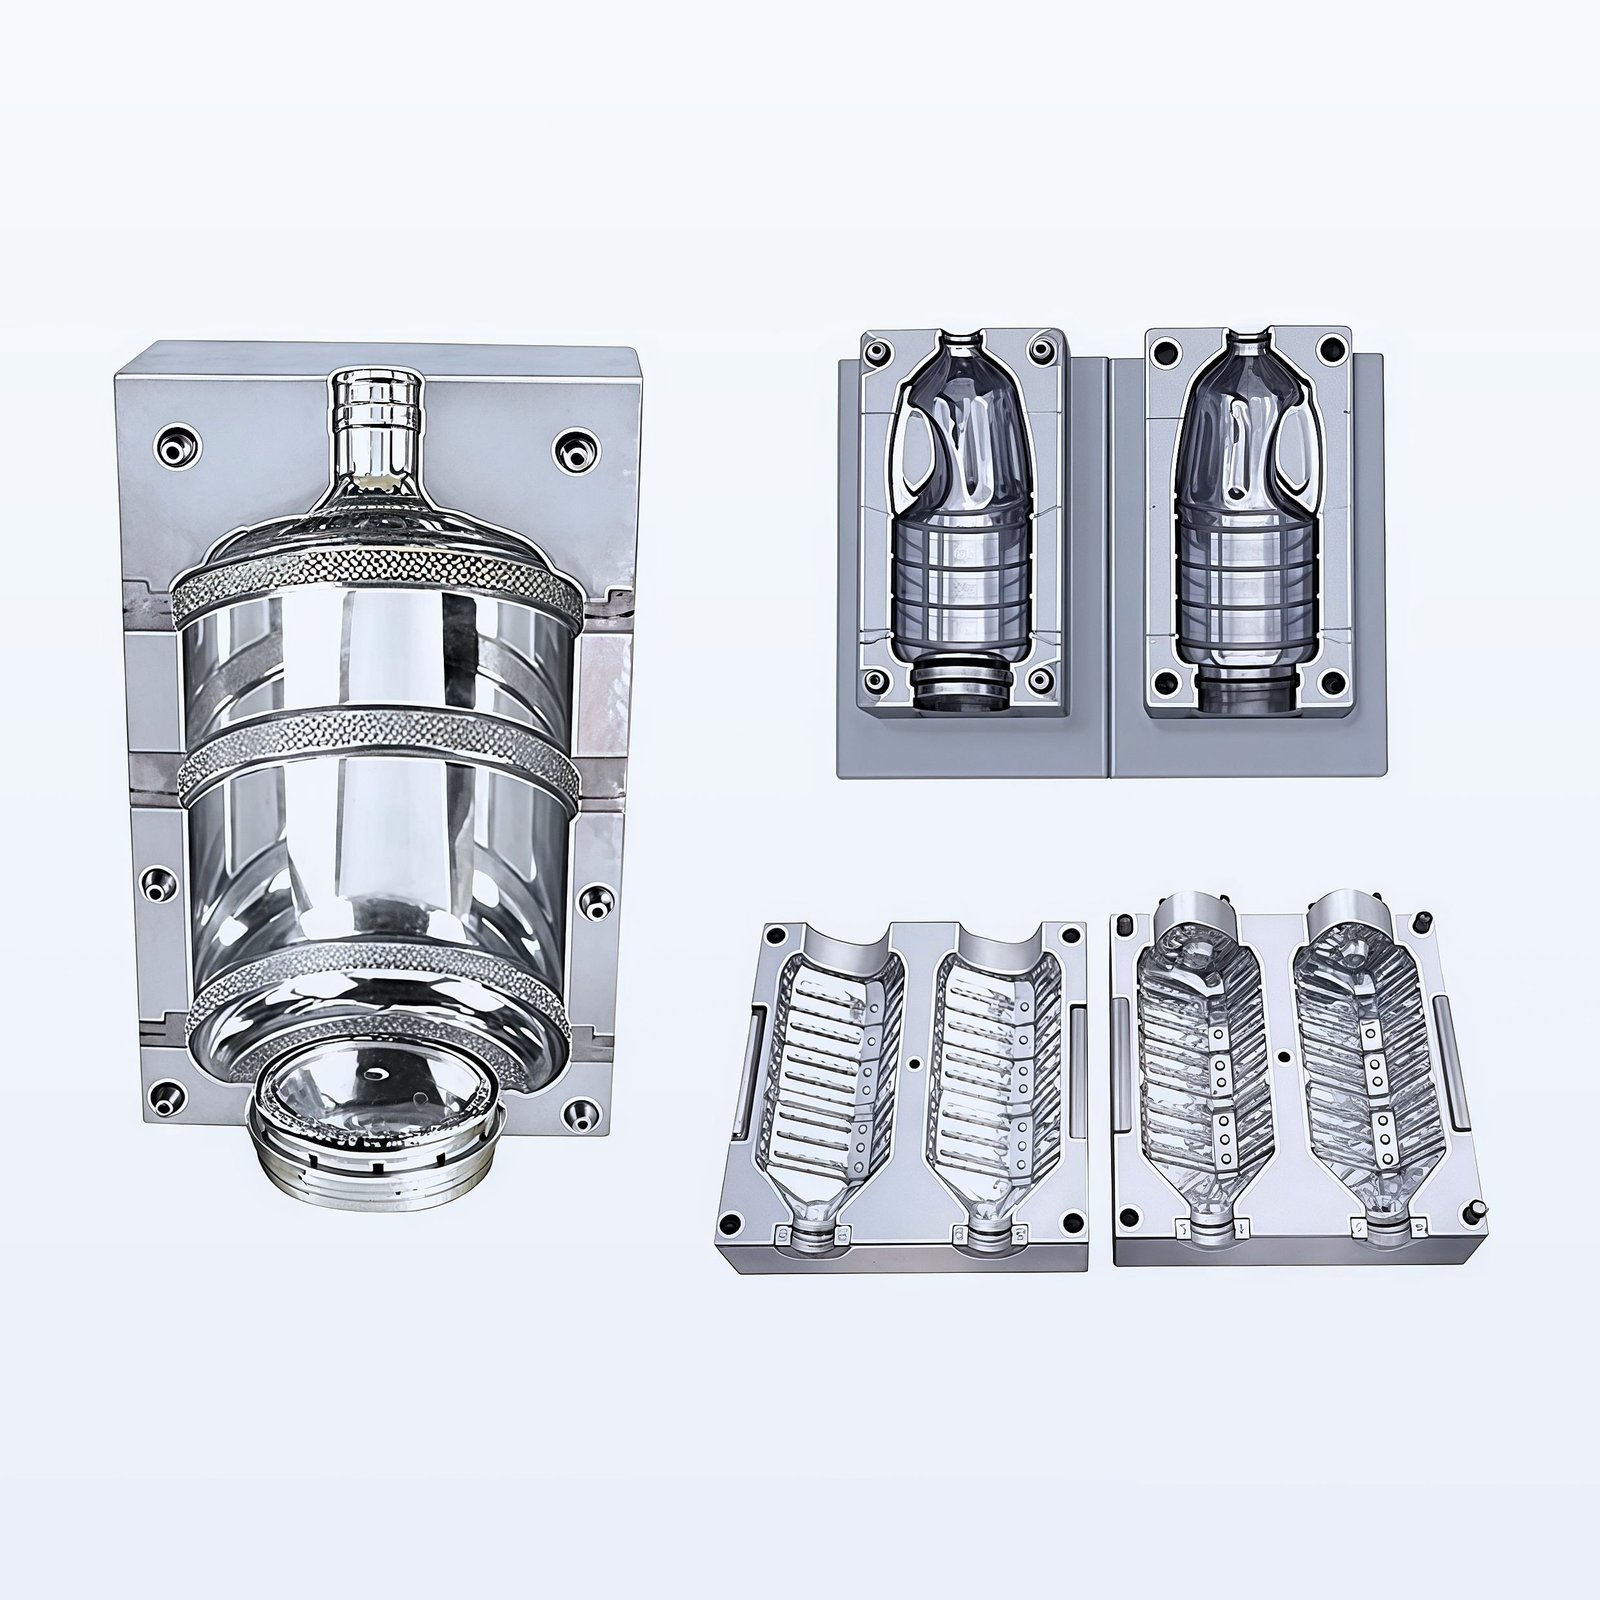
1. Metallurgical Comparison: 7075-T6 Aluminum vs S136 Tool Steel
In stretch blow molding, preforms reheated to 105°C are stretched axially and inflated under 35-bar air pressure. The bottle must chill below its glass transition temperature (78°C) before mold opening to prevent structural collapse.
Thermal conductivity is the governing physical property in blow molding. Because PET is an organic polymer with low internal thermal diffusivity, the mold steel must draw heat away instantly upon contact:
| Property | Aircraft Aluminum 7075-T6 | Stainless Steel S136 ESR |
|---|---|---|
| Thermal Conductivity | 130 W/m·K (Ultra-Fast) | 26 W/m·K (Standard) |
| Density (Weight) | 2.81 g/cm³ (Lightweight, fast changeover) | 7.80 g/cm³ (Heavy) |
| Surface Hardness | HB 150 (HV 450 with Hard Anodize) | HRC 50 – 54 (Extremely Hard) |
| Average Tool Life | 5,000,000 – 8,000,000 Shots | 15,000,000+ Shots |
| CNC Machining Time | 50% Faster Spindle Feeds | Standard Milling Speeds |
Need custom blow molds for your bottle blowing machines?
Sailwin supplies linear and rotary stretch blow molds compatible with all international machine models.
2. Hybrid Composite Molds: The Best of Both Worlds
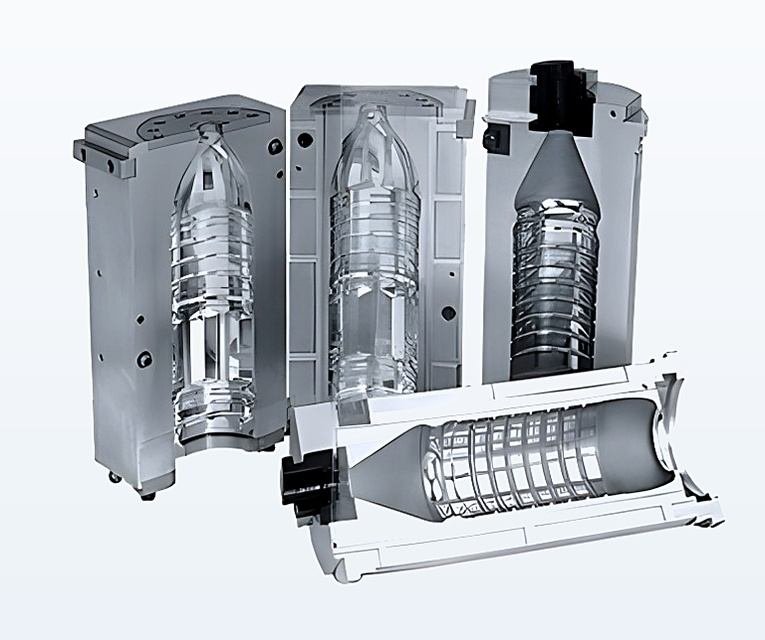
To overcome the wear vulnerability of aluminum at moving joints while retaining maximum thermal cooling speed, Sailwin pioneered hybrid composite pet blow molds.
In this architecture, the main bottle body halves are precision machined from certified 7075-T6 aluminum and treated with 50-micron hard anodizing. However, the base cup assembly—which moves upward under hydraulic cylinder force on every cycle and experiences severe mechanical impact—is crafted from hardened stainless steel S136 or wear-resistant beryllium copper. This ensures 10,000,000+ shot durability with zero base alignment wear. Explore preform matching requirements in our preform mold engineering guide.
3. Sailwin Case Study: Beverage Plant Boosts Output by 18% With 7075 Molds
A water bottler in Vietnam converted six linear stretch blow molding machines from older P20 steel molds to Sailwin 7075-T6 aluminum tooling, slashing bottle cooling time from 2.1s to 1.3s.
- Client: Contract packaging bottler running 500ml mineral water bottles at 12,000 BPH on 6-cavity linear blowers.
- Problem: Older P20 steel blow molds suffered from thermal bottlenecking; bottles ejected warm and developed base rocking.
- Throughput Penalty: Machine speed was throttled back to 9,800 BPH to prevent bottle deformation.
- Tooling Replacement: Fabricated Sailwin 6-cavity 7075-T6 aircraft aluminum blow molds with hard-anodized cavities.
- High-Flow Cooling: Redesigned internal water channels for turbulent flow at 10°C chiller input.
- Steel Petaloid Inserts: Installed hardened S136 stainless steel inserts in the petaloid base cups for maximum impact life.
- Cycle Velocity: Cooling dwell dropped by 0.8 seconds, enabling full 12,000 BPH line speed (22.4% output increase).
- Rocking Base Eliminated: 100% of bottles passed hot-fill and vertical perpendicularity drop testing.
- Tooling Weight: Molds were 62% lighter, cutting mold changeover times from 90 minutes to under 35 minutes.
Data source: Sailwin Operational Log #BLW-2025-07. Molds: SW-BLW-6CAV 7075-T6 Water Bottle Blow Tooling.
Looking to accelerate blow molding cycle times?
Send your container volume and machine model to Sailwin for a custom aluminum blow mold proposal.
4. Frequently Asked Questions: PET Bottle Blow Mold Materials
Need fast-turnaround blow molds for an upcoming product launch?
Sailwin delivers pilot sample blow molds in 7 to 10 calendar days with full bottle blow verification.
5. Summary: Selecting the Optimal Blow Mold Material
For standard high-output beverage bottling, aircraft 7075-T6 aluminum provides unmatched thermal cooling advantages that reduce cycle times and maximize machine hourly return. When combined with hardened steel base cups in a composite construction, converters achieve maximum speed with lifelong tooling durability.
- Choose 7075-T6 aluminum for water, juice, and CSD containers to achieve 15% to 25% faster cooling.
- Specify S136 stainless steel for cosmetic mirror finishes or long-life production exceeding 15,000,000 bottles.
- Consult Sailwin for custom blow molds engineered with high-speed CNC precision and certified aerospace alloys.
SAILWIN TOOLING · BLOW MOLD EXCELLENCE
Ready to Accelerate Your Bottle Blowing Cycles?
Upload your 2D bottle prints or 3D CAD files. Our blow mold engineering specialists will deliver a customized mold drawing, thermal simulation, and competitive quotation within 24 hours.
Explore Precision Blow Tooling & Mold Systems:
• pet blow molds – Turnkey aircraft aluminum 7075 and stainless blow molds.
• water bottle blow mold – 0.2L to 2.5L mineral water container tooling.
• 5 gallon bottle blow mold – Heavy-duty 5-gallon water dispenser drum tooling.
• valve-gate preform molds – High-speed multi-cavity preform molds.
• bottle cap injection mold – 1881 & 3025 closure molds.
• Need dedicated technical advice? Contact our blow mold engineers for custom bottle tooling consultation.

