Precision Plastic Molds Manufacturer: Blow, Extrusion & Injection Tooling
Industrial-grade custom plastic mold maker specializing in three core categories: PET stretch bottle blow molds, heavy-duty extrusion blow molds (EBM), and high-cavity PET preform & bottle cap injection molds. CNC 5-axis accuracy to ±0.005mm, 100% factory trial testing before dispatch.
Request Custom Mold Proposal
Submit your container requirements or CAD drawings. 24-hour engineering response & free DFM analysis.
Trusted by Global Industry Leaders & Fortune 500 Converters
Three Core Plastic Mold Engineering Series
Factory-direct engineering solutions covering high-speed stretch blow molds, heavy-duty industrial extrusion blow molds, and multi-cavity PET preform & bottle cap injection molds.
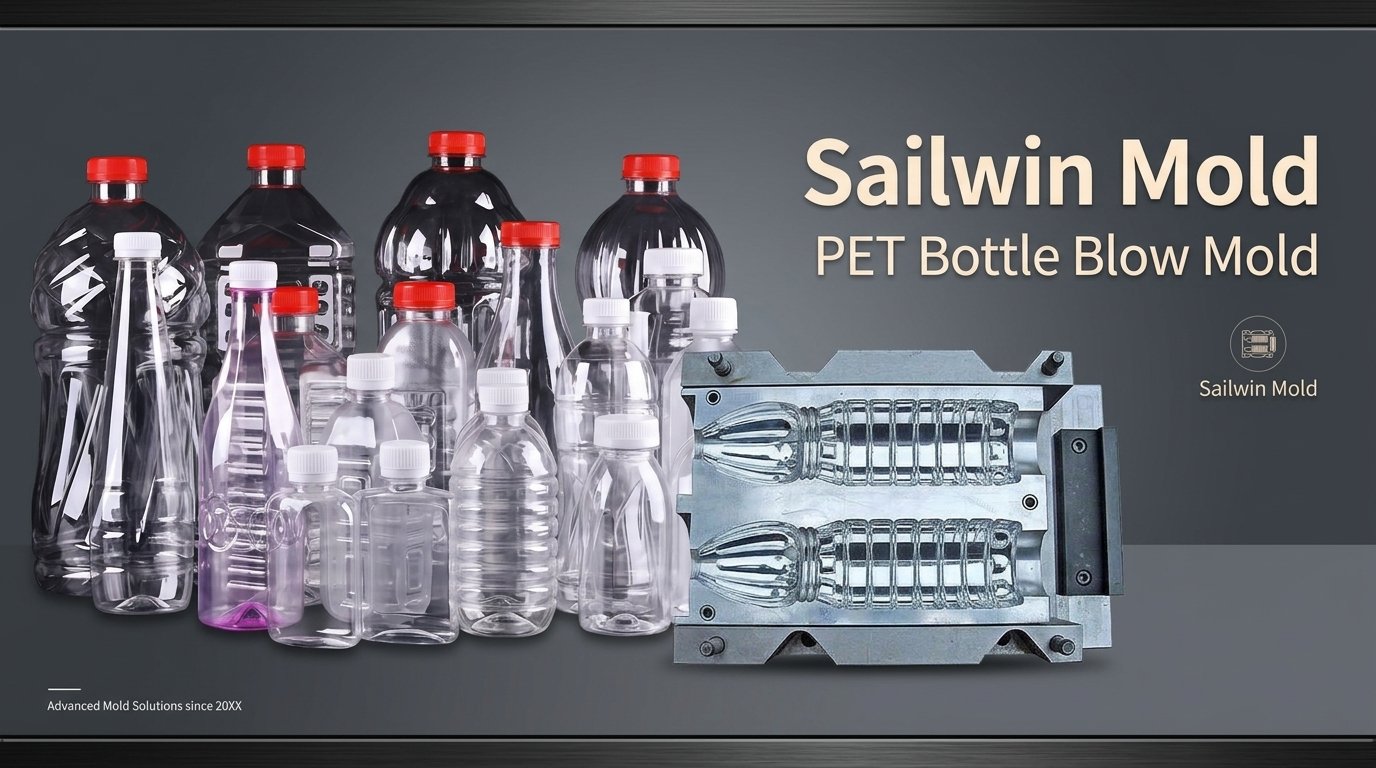
1–16 CAVITIESPET Bottle Blow Molds
High-speed linear and rotary stretch blow molds for mineral water, CSD, juice, edible oil & wide-neck jars. Aviation 7075-T6 aluminum cavities with S136 stainless steel base inserts.
- Output: Up to 24,000 BPH on rotary machines
- Air Pressure: 10–35 Bar blow air compatibility
- Quick Change: <5 min single-cavity slide mechanism
- Compatibility: Sidel, Krones, SMI, Tech-Long
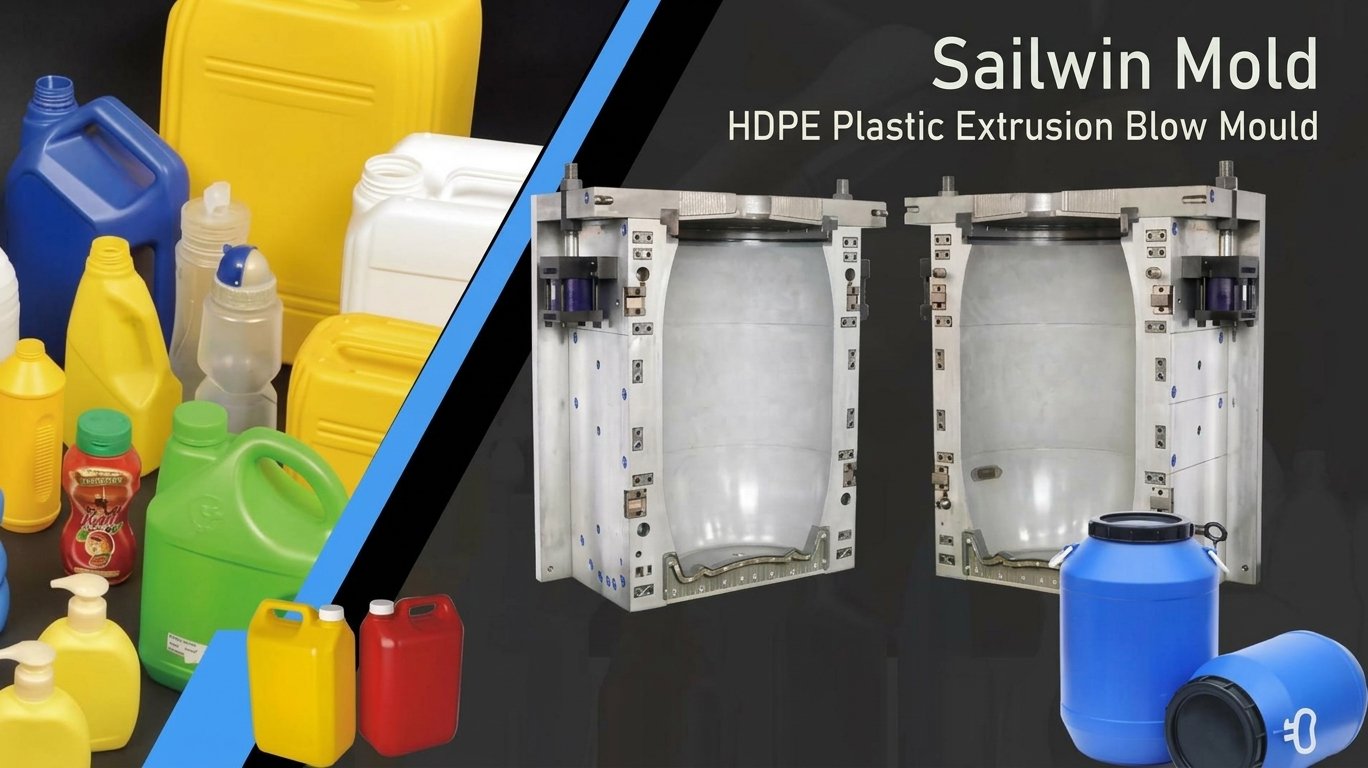
10ML – 1,000LExtrusion Blow Molds (EBM)
Industrial-grade molds for HDPE/PP jerry cans, lube oil bottles, chemical drums, agrochemical bottles & automotive air ducts. Beryllium copper pinch-offs for clean deflashing.
- Pinch-Off: Japanese Be-Cu C17200 inserts
- Jerry Can: Hydraulic core-pulling handles
- Steel Grade: Pre-hardened P20 / 718H / S136
- Deflashing: Automatic in-mold shear cutoff
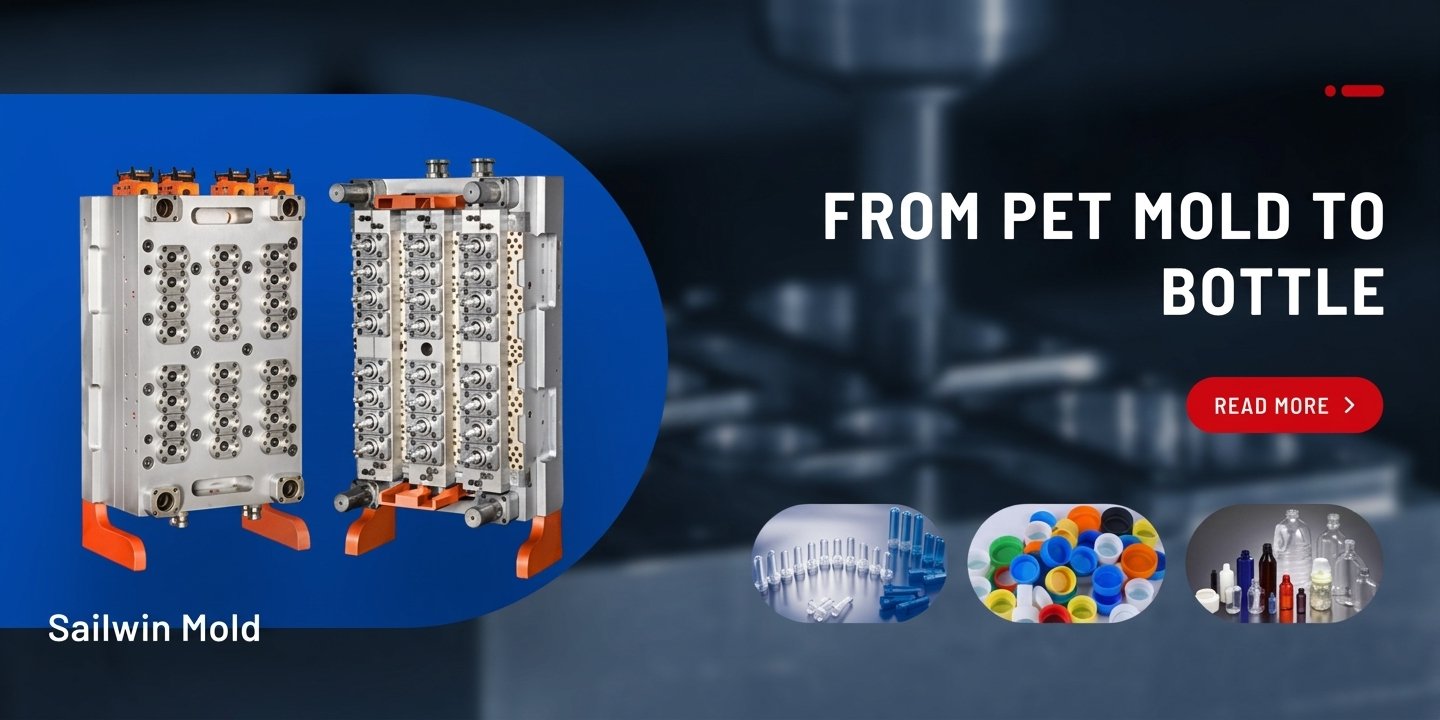
8 – 96 CAVITIESPreform & Cap Injection Molds
Multi-cavity PET preform tooling with balanced valve-gate hot runners and 9 specialized bottle cap molds: water caps, oil pull-ring caps, flip-top, CRC, sauce valves, and 2K cosmetic closures.
- Preform Tooling: 8 to 96 cavities valve-gate
- Cap Series: 1881 / 29/25 / 38mm / Flip-top / CRC
- Core Steel: Swedish ASSAB S136 (HRC 52-54)
- Interchangeability: 100% single-cavity drop-in
END-TO-END ENGINEERING EXCELLENCE
Turnkey Molding Solutions: From Concept to Production
Whether you provide a physical sample, an idea sketch, or a 3D CAD model, Sailwin provides a seamless, transparent 3-step engineering pipeline to transform your packaging concept into mass-production tooling.
STEP 013D Mold Design & Mold Flow Analysis
Our R&D engineers utilize UG (Siemens NX), Pro/E, and AutoCAD to construct fully parametric 3D bottle geometry, cavity parting lines, and slide mechanisms. We conduct comprehensive Mold Flow simulation to calculate preform expansion ratios, wall thickness distributions, and resin stress points before metal cutting starts.
Precision CNC 5-Axis Machining
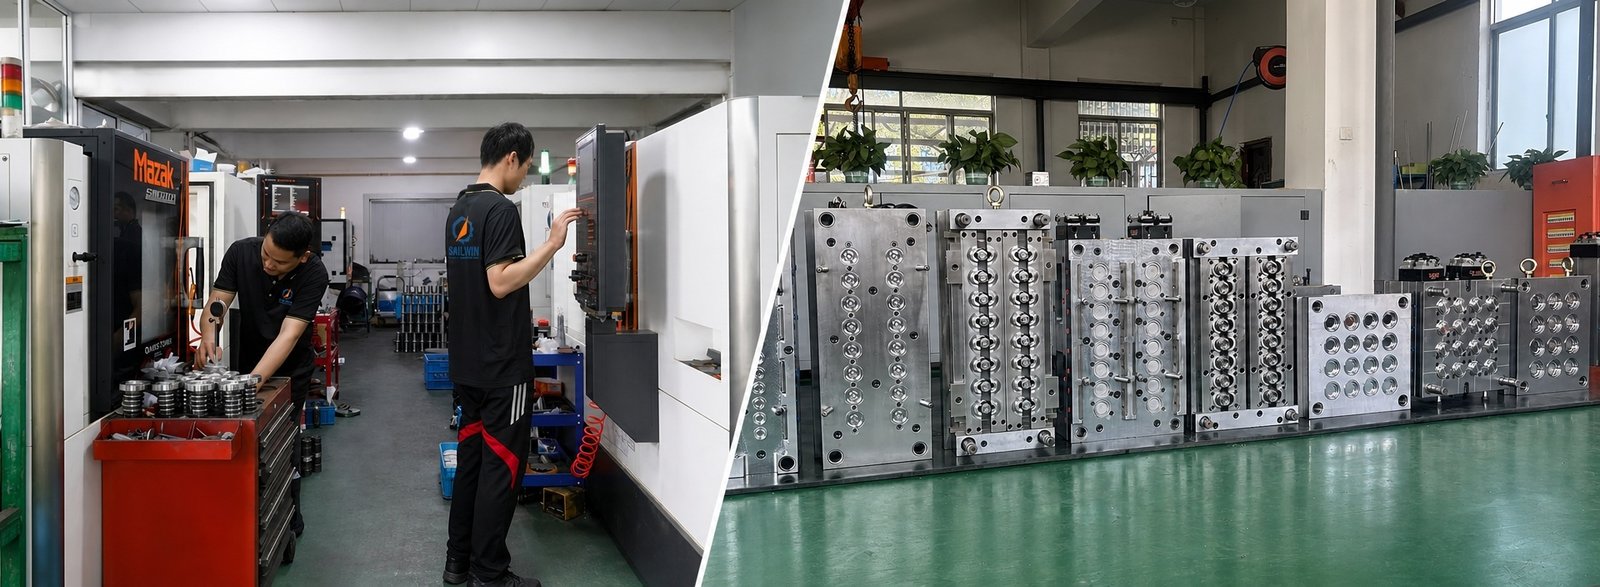
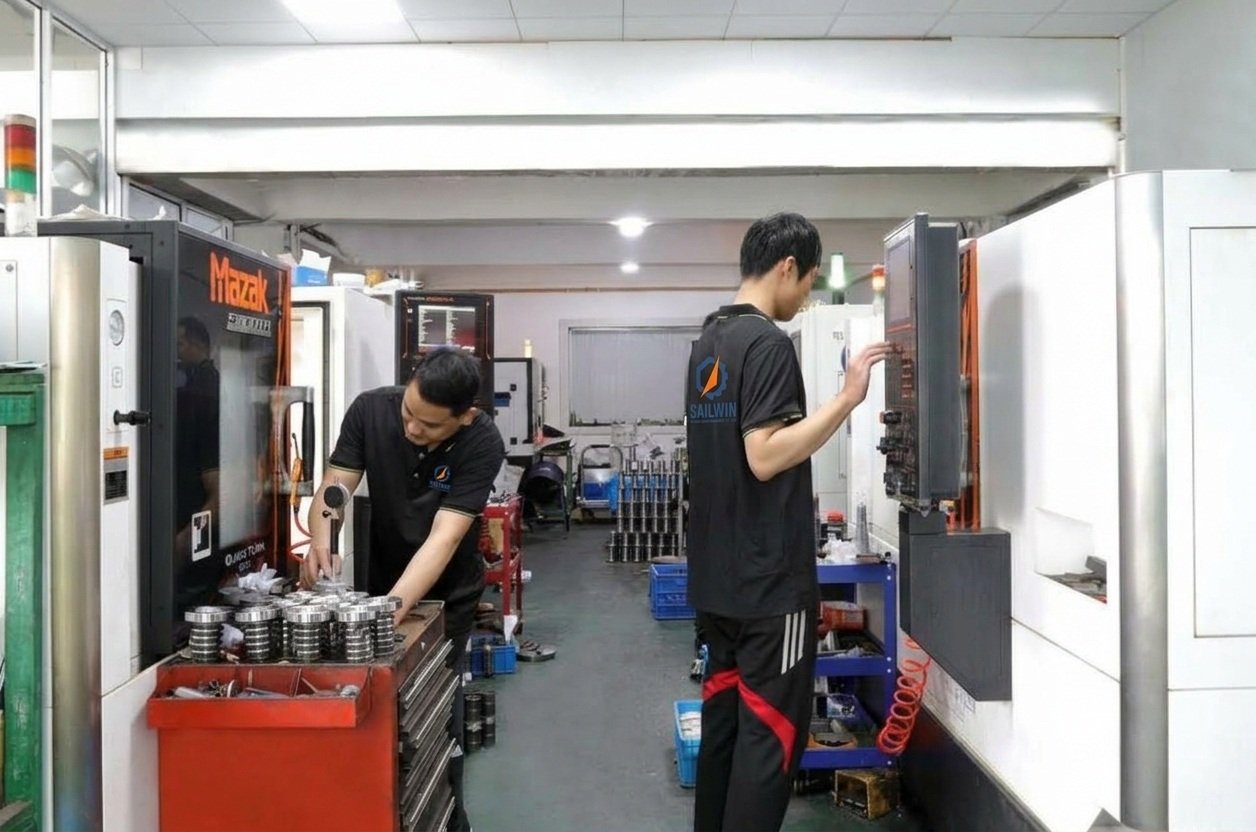
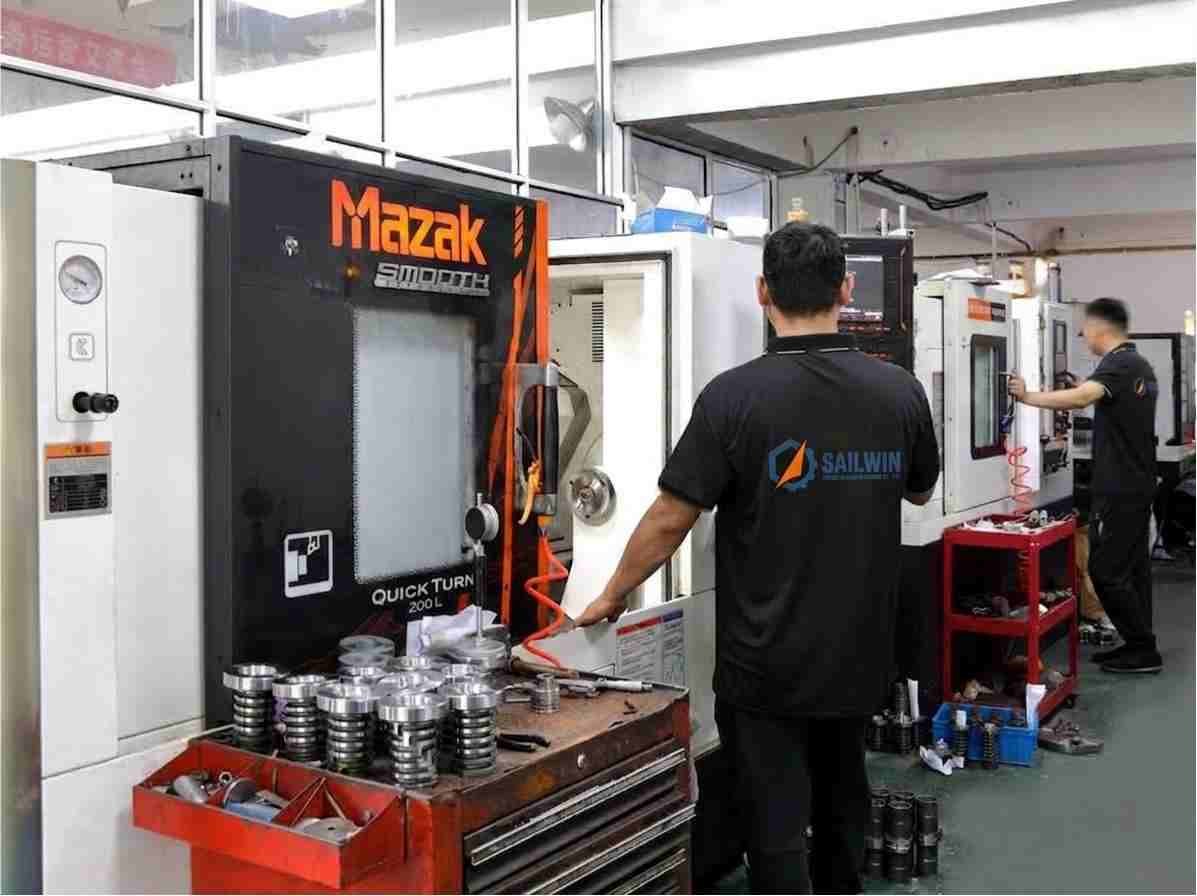
Tool paths are executed on DMG MORI 5-axis machining centers (24,000 RPM) and Mazak precision milling fleets. Aviation 7075-T6 aluminum cavity blocks and ASSAB S136 stainless steel inserts are machined within ±0.005mm tolerances. Mirror EDM and precision grinding yield an optical mirror surface finish of Ra 0.02μm for flawless container clarity.
STEP 02
STEP 03Trial Testing & Sample Inspection
Every mold undergoes full-pressure test runs on our in-house production blow molding and injection presses. We measure bottle burst pressure, perpendicularity, weight variance (<0.1g), and seal torque. 50–100 molded sample containers are express-couriered to your plant for physical sign-off before mold shipment.
DIRECT MANUFACTURER POWER
Why Choose Sailwin: True Precision Factory Direct
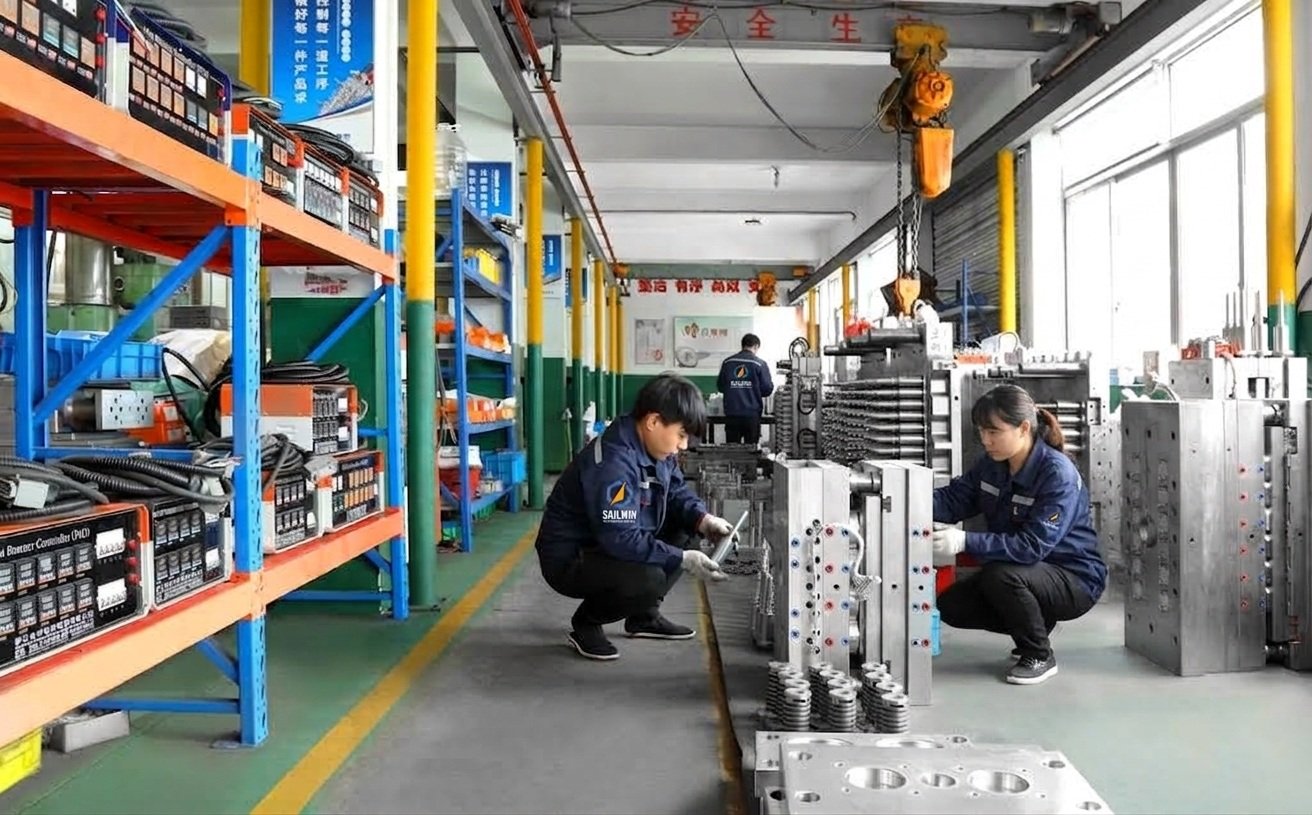
We are not an export trading broker. Sailwin owns a 3,500m² modern CNC machining facility in Taizhou, Zhejiang, equipped with imported 5-axis centers, Mazak precision lathes, mirror-spark EDMs, and optical coordinate metrology.
High Precision & Long Life
100% genuine aerospace 7075-T6 aluminum and Swedish S136 steel. Mirror finish Ra 0.02μm with vacuum hardening to HRC 52-54 guarantees 5,000,000 to 10,000,000 shots without flash.
Fast Mold Lead Time (20–35 Days)
Integrated CAM programming and standardized material stocking compress lead times: standard blow molds delivered in 20–25 days; high-cavity preform molds in 35–45 days.
Strict Quality Assurance (Zero-Defect CMM)
Zero-tolerance inspection via Hexagon 3D CMM ruby scanning. Prussian-blue contact rate >90% ensures zero parting flash and 100% single-cavity drop-in interchangeability.
Global On-Site & Lifetime Support
Field engineers available for overseas mounting, trial tuning, and operator training. Free wearable spare parts package included plus lifetime at-cost replacement supply.
QUALITY ASSURANCE & WORLDWIDE FOOTPRINT
Zero-Defect Quality Control for Every Molded Part.
Strict ISO 9001:2015 quality control principles govern our entire production cycle. From raw forging steel spectral verification to our prominent presence at the world's leading packaging expos, Sailwin stands for verifiable industrial accountability.
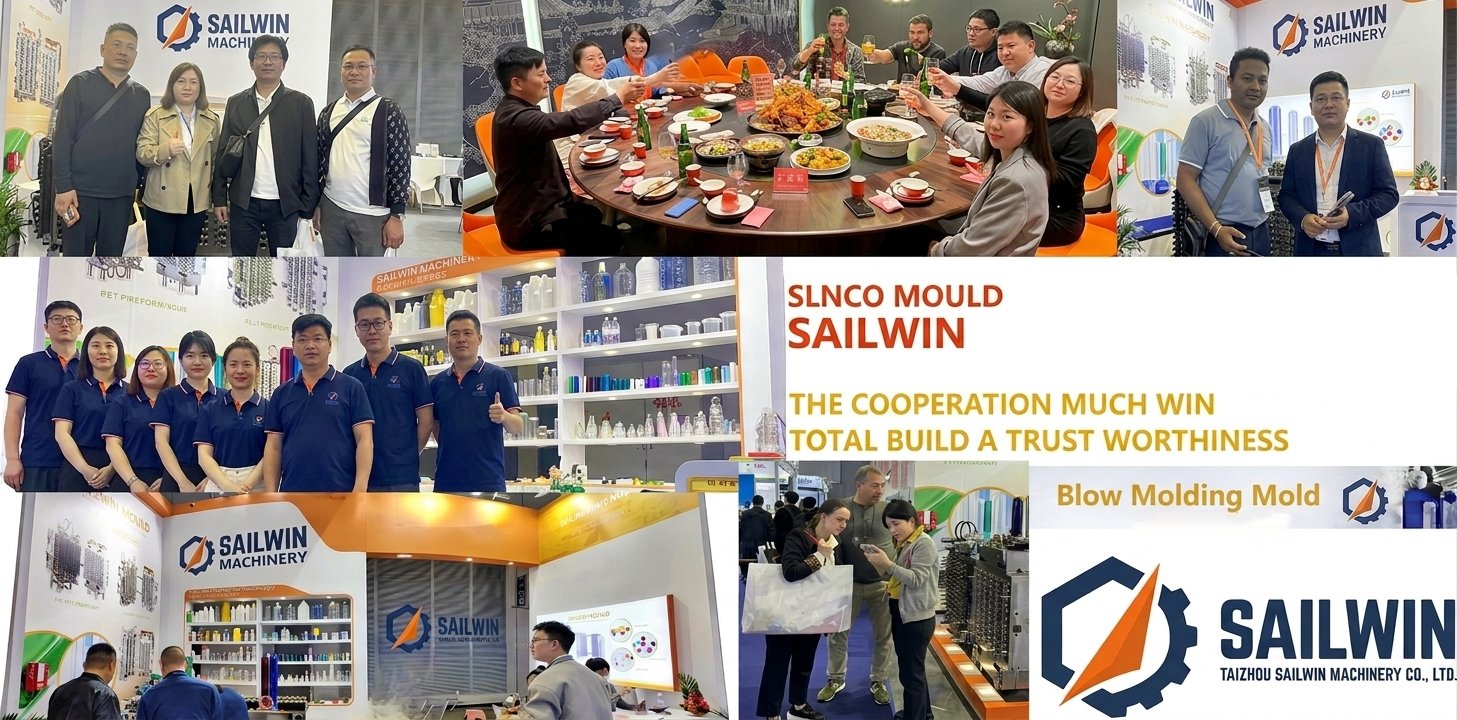
Meeting Global Bottling & Packaging Partners Face-to-Face
Regular exhibitor at premier international packaging expositions: Chinaplas, NPE (USA), K-Show (Germany), and Gulfood Manufacturing (Dubai).
International Quality System Certification & Metrology
Spectral analysis of incoming 7075-T6 aluminum and ASSAB S136 stainless steel for density, hardness, and ultrasonic crack detection.
On-machine optical probe measurement during 5-axis milling ensures cavity profile concentricity stays strictly within ±0.005mm.
Manual red lead spotting fit-up on mold parting surfaces ensures >90% contact area, eliminating micro-flash and air loss.
Full-pressure production machine trial; 50–100 sample containers couriered to client for lab burst and drop sign-off before dispatch.
Mineral Water Bottling
16-Cavity rotary blow mold delivered 24,000 BPH. Gram weight cut from 13.0g to 9.8g (24.6% resin cost savings).
Edible Cooking Oil
4-Cavity 5L square oil bottle mold with integrated handle. Passed 1.8m drop test with zero corner stress cracks.
Chemical Packaging
25L Jerry Can mold passed severe UN 1.9m -18°C drop impact and pneumatic pressure testing.
High-Cavity Preforms
48-Cavity preform mold achieved eccentricity <0.03mm, reducing bottle blowing rejection rate by 90%.
Tailored Tooling for Every Bottle, Jar & Closure Application
Whether you produce ultra-lightweight water bottles at 24,000 BPH, heavy-duty 5L edible oil jugs with integrated handles, or child-resistant pharmaceutical jars, Sailwin delivers optimized cavity geometry and short cycle times.
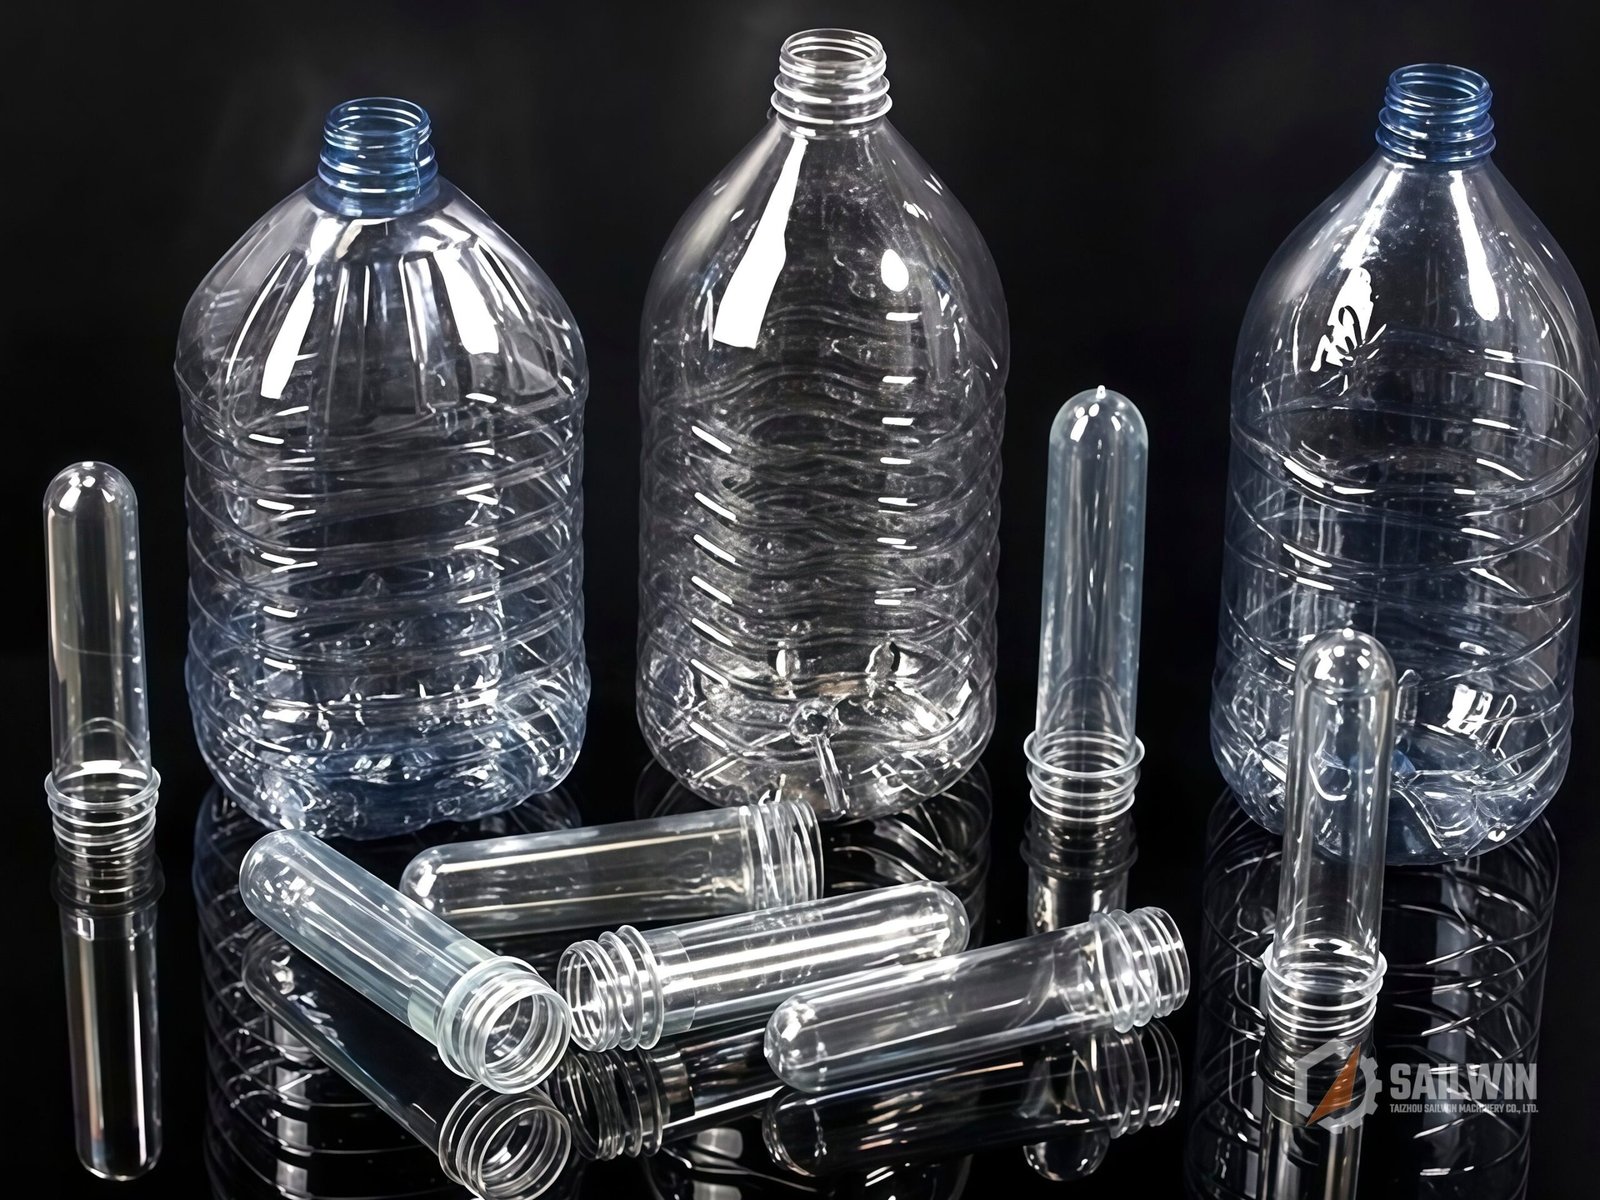
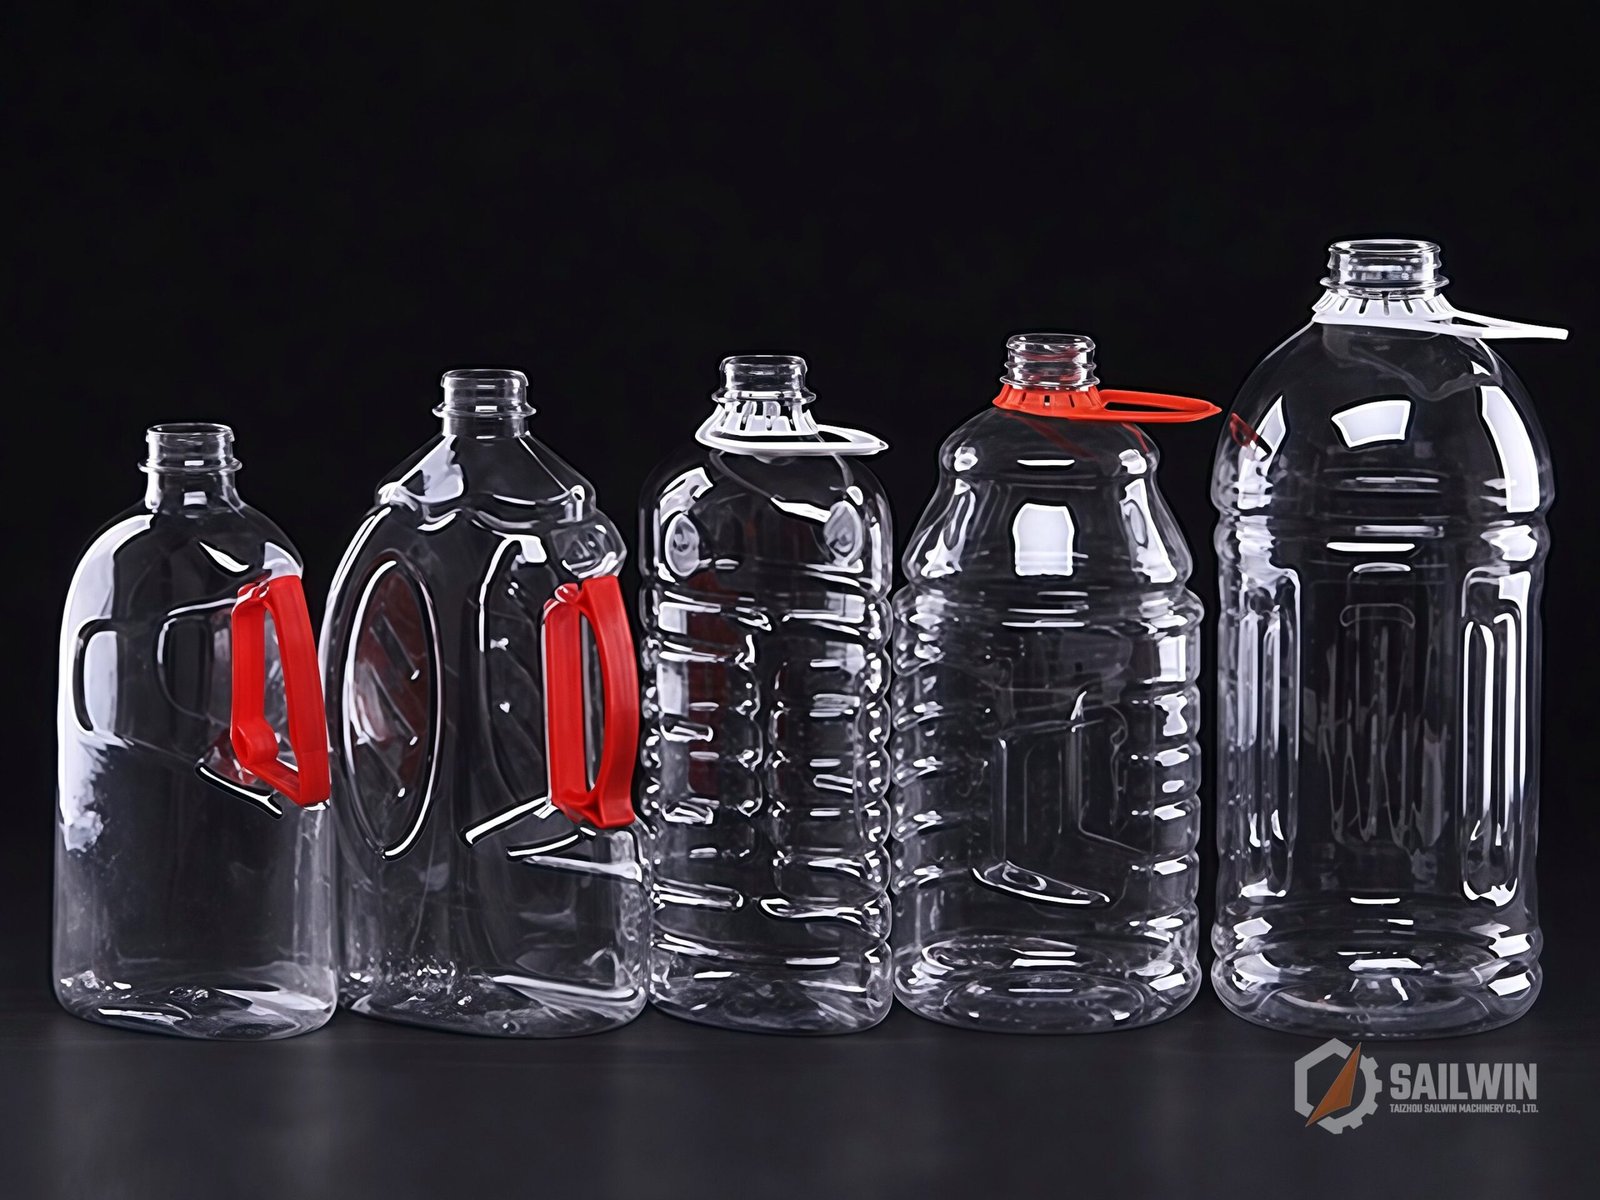
Water & Beverage Bottles
Lightweight mineral water, CSD carbonated drinks, juices & functional beverages. Petaloid base withstands 10–14 Bar pressure with high blow stretch consistency.

Edible Oil & Sauce Jugs
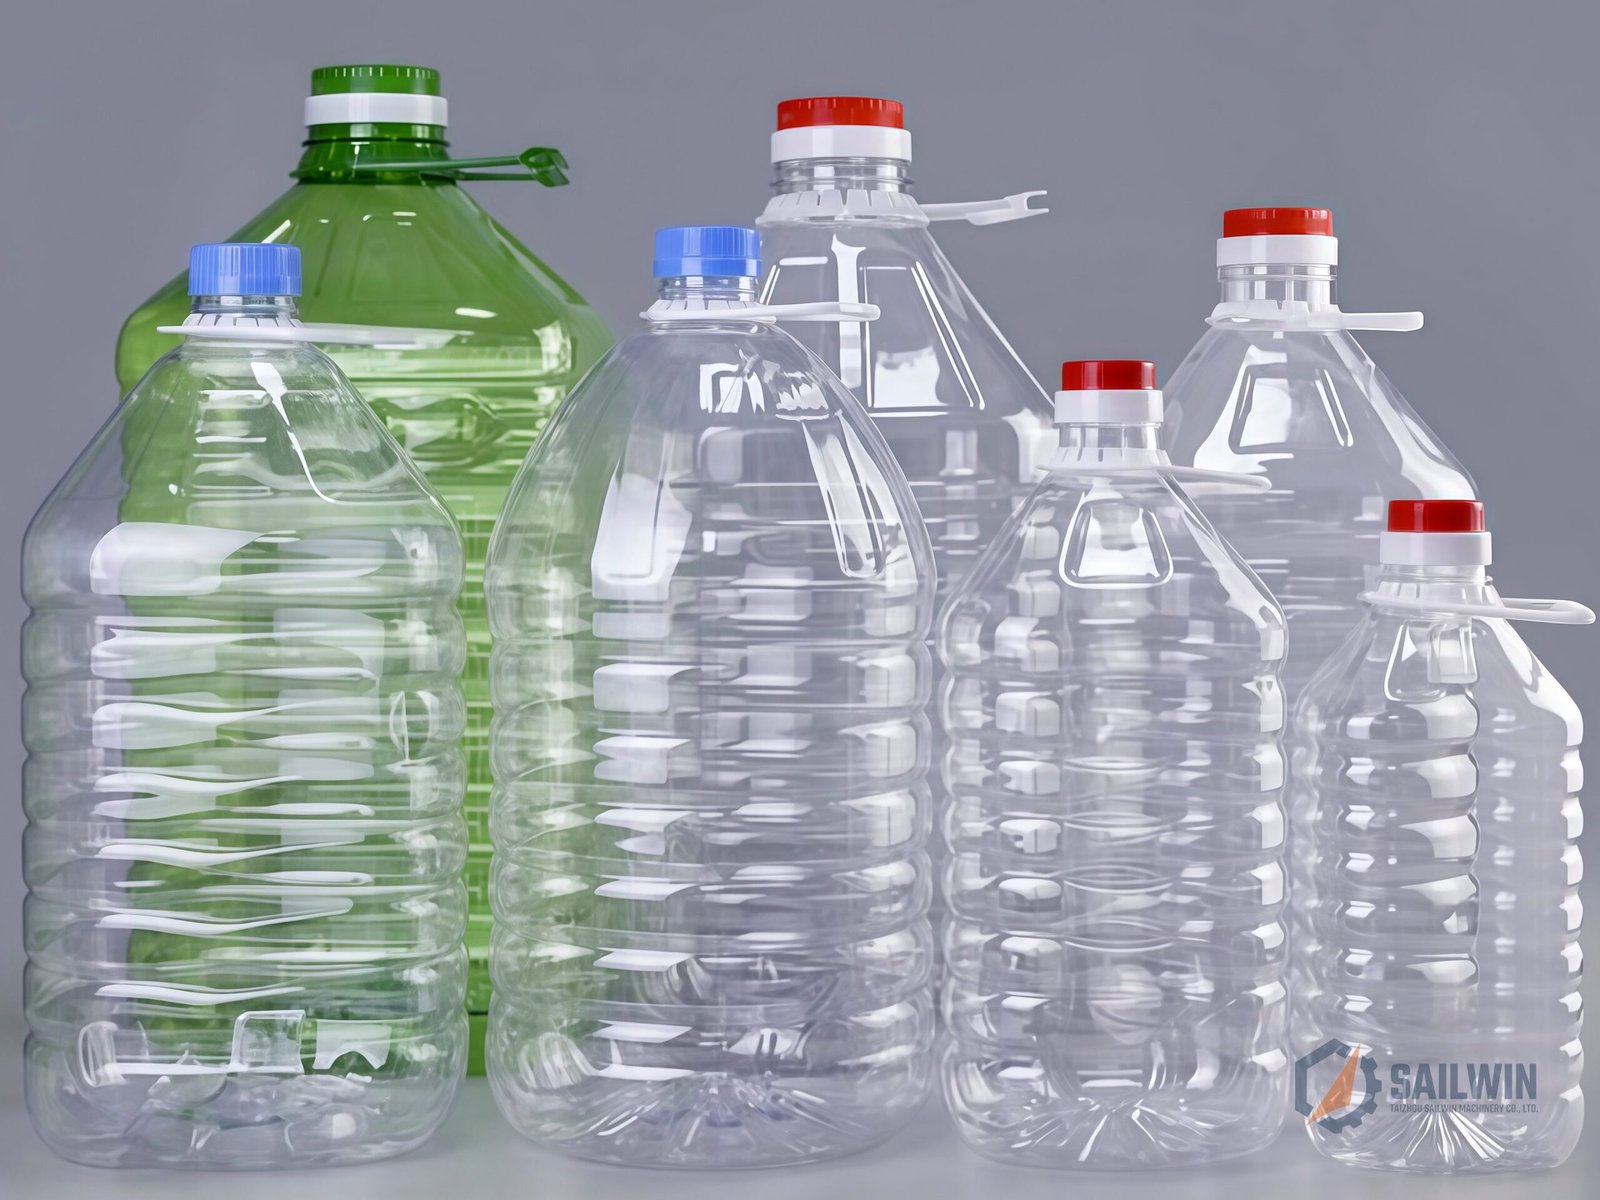
Square and round cooking oil bottles and condiment containers with integrated sturdy side handles or snap-on bail handles, preventing corner drop fracture.

Wide-Mouth Food Jars
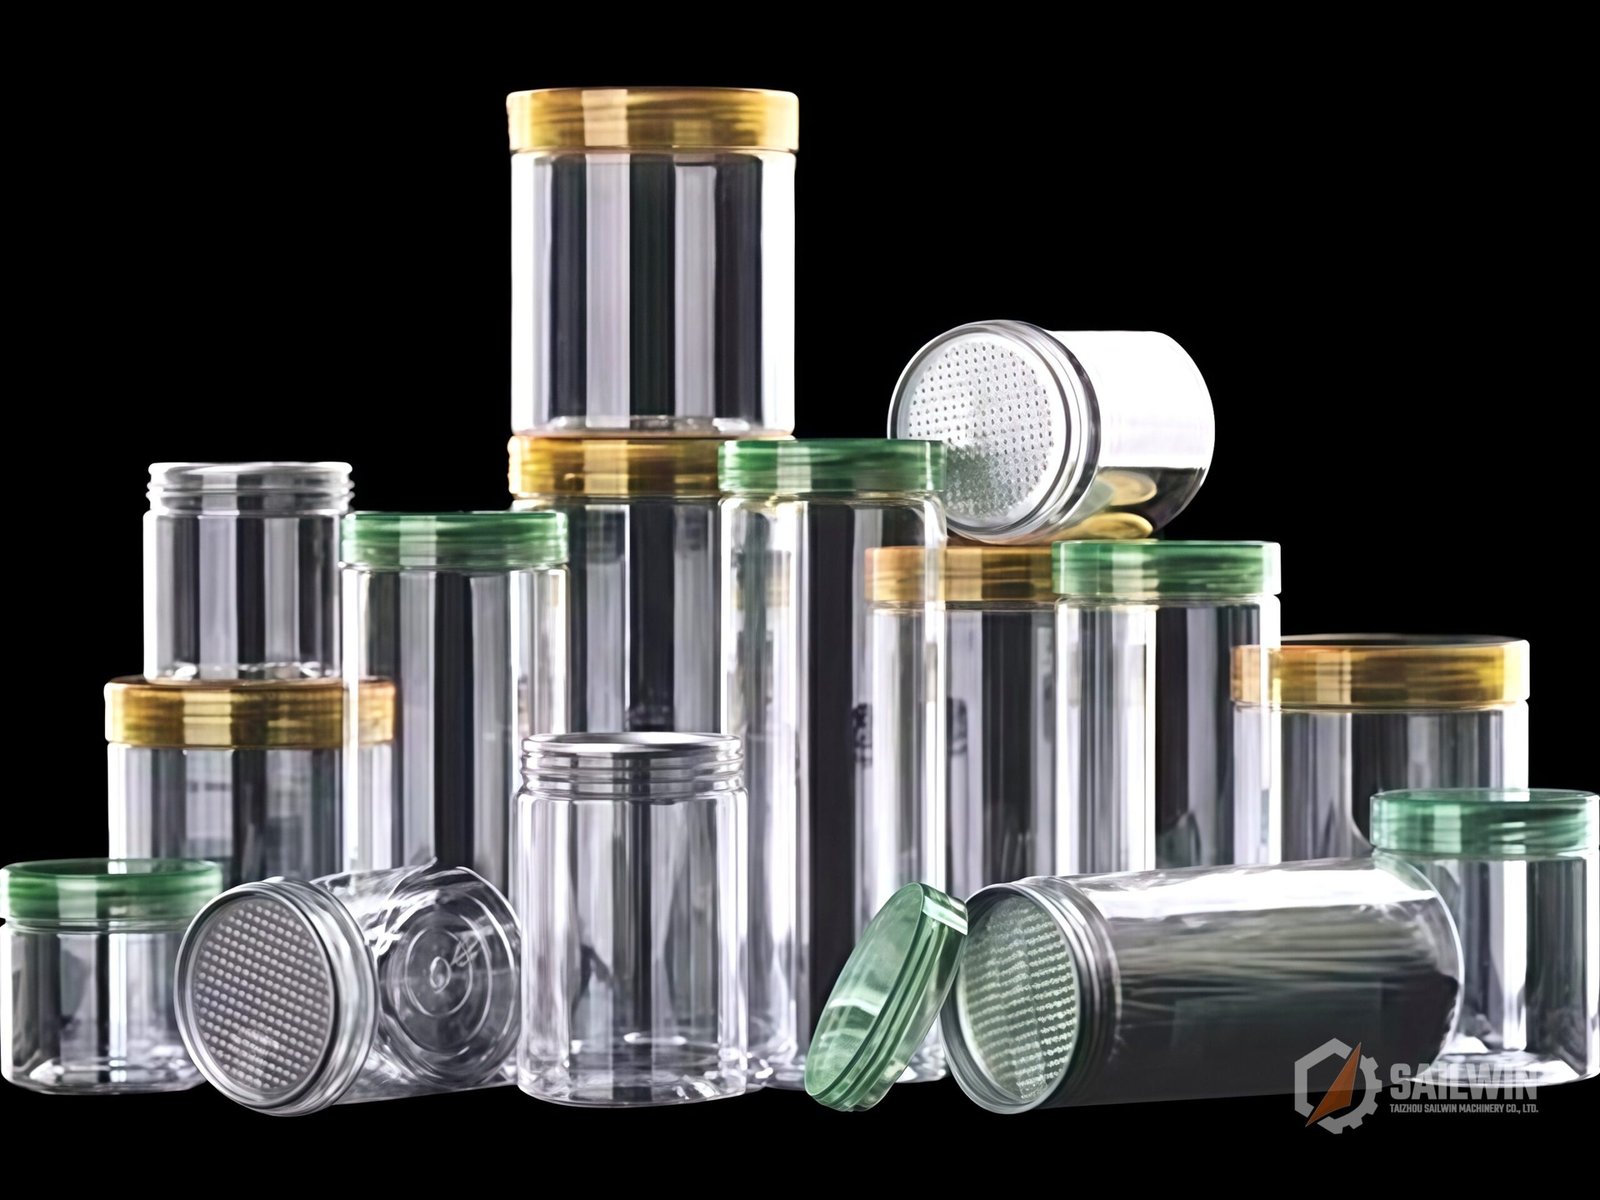
Crystal-clear jars for peanut butter, honey, candy, cookies, dried fruits, and spice containers with flat leakproof bases and precision screw neck splits.

Pharmaceutical & CRC Bottles
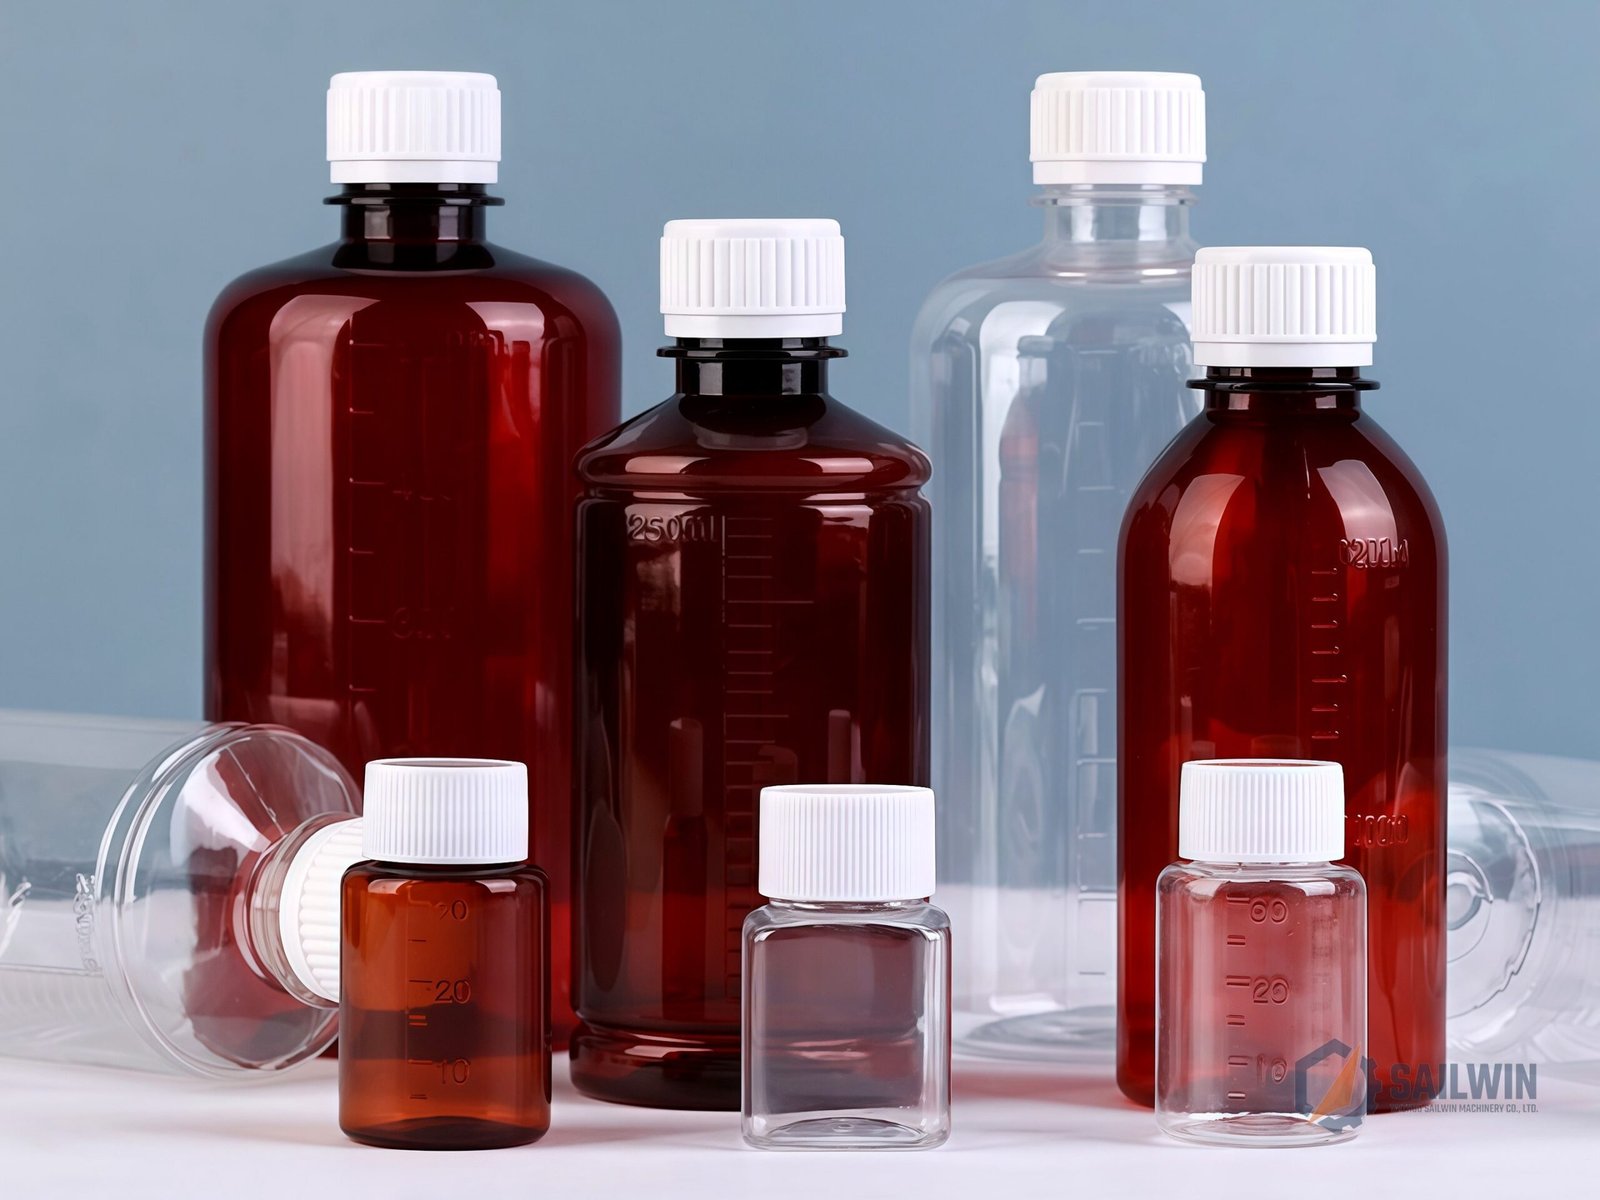
Amber and clear syrup bottles, tablet containers, and cosmetic lotions paired with child-resistant (CRC) or flip-top closures complying with ASTM standards.

5-Gallon Water Jugs
Heavy-duty PET 5-gallon water dispenser carboys with integrated handle recess or handle inserts, engineered for high clamp force and zero leakage.
Explore Specialized Plastic Mold Solutions & Guides
Instant access to high-cavity PET stretch blow molds, heavy-duty EBM tooling, closure injection systems, and engineering design guides.
PET Stretch Blow Molds 1-16 Cav
Extrusion Blow Molds EBM Series
Preform & Cap Molds Injection
ENGINEERING CLARITY
Frequently Asked Questions About Plastic Molds
Technical answers from Sailwin's chief tooling engineers regarding machine compatibility, steel metallurgy, cycle optimization, and turnkey mold warranties.
Can Sailwin molds be installed directly on Sidel, Krones, SMI, Tech-Long, or other blow machines? +
Yes, 100% physically and pneumatically compatible. We manufacture stretch blow molds tailored to your specific machine mounting standard — including Sidel Matrix/Universal, Krones Contiform, SMI, Tech-Long, Newamstar, and Chinese linear blowing systems. We verify backplate pin holes, bottom mold lifting cams, quick-disconnect cooling couplings, and high-pressure air manifold dimensions before fabrication.
How does 7075-T6 aviation aluminum compare to S136 stainless steel for blow molds? +
Aviation-grade 7075-T6 aluminum provides nearly 3x the thermal conductivity of tool steel, drastically reducing blowing cycle times and bottle cooling duration while reducing overall mold weight for faster machine indexing. Its surface is hard-anodized (HB 150+) to prevent scratching. For mold bases that endure repeated 35-bar impact, we utilize S136 stainless steel (HRC 48-52) to deliver a 10-million-shot operational lifespan.
What mold steel grades do you recommend for different resin types (PET, HDPE, PP, PVC)? +
Material selection depends strictly on the chemical properties and abrasive nature of your plastic resin:
- PET Stretch Blow Molds: 7075-T6 aviation aluminum cavities with S136 stainless steel base inserts.
- HDPE / PP Extrusion Blow Molds (EBM): Pre-hardened P20 / 718H steel mold plates with Be-Cu (beryllium copper C17200) pinch-off inserts for rapid neck/handle cooling.
- PET Preform & Cap Injection Molds: Swedish ASSAB S136 vacuum-quenched stainless steel (HRC 52-54) for complete acid corrosion resistance and optical Ra 0.02μm polish.
- PVC Blow Molds: Special hard-chrome or electroless nickel-PTFE plating to resist corrosive hydrochloric gas release.
How do you achieve bottle lightweighting without sacrificing drop or top-load strength? +
Lightweighting is achieved through scientific rib placement and axial stretch ratio balancing in our 3D CAD modeling. By reinforcing bottle corners and shoulder contours while reducing wall thickness in non-load-bearing areas, we have helped beverage bottlers reduce 500ml water bottle weights from 13.5g to 9.8g while maintaining required vertical top-load compressive strength and ASTM 2-meter drop standards.
Can individual cavity components on preform and cap molds be replaced independently? +
Yes. 100% CNC interchangeability. All Sailwin preform cores, cavity sleeves, neck splits, and cap core inserts are precision ground on Swiss Mikron and Okamoto machines within ±0.005mm tolerance. If a single cavity ever wears down or sustains accidental damage, you can insert a replacement spare part directly on-site without manual fitting, grinding, or re-matching.
What is the standard lead time, and do you supply sample molded bottles before dispatch? +
Standard lead times are 20–25 days for PET blow molds, 30–40 days for EBM extrusion blow molds, and 45–55 days for high-cavity preform & cap injection molds. Under our strict Factory Acceptance Test (FAT) policy, we mount each mold on our in-house production machines, blow/inject actual plastic resin, and express-airship 50–100 trial sample containers for your laboratory approval before commercial mold dispatch.
Can you reverse-engineer a custom mold if we only have a physical bottle sample? +
Yes. You can courier your physical sample bottle, jar, or cap to our technical center. Our optical metrology team conducts 360° blue-light 3D scanning, recreates parametric 3D CAD models (STEP/IGES), analyzes preform expansion ratios, and optimizes neck threads and parting lines for modern high-speed production.
Have a specific bottle or closure tooling inquiry?
START YOUR MOLD PROJECT TODAY
Get Your Free 24-Hour DFM & Mold Flow Analysis
Submit your 3D container CAD drawing (STEP, IGES, DXF) or bottle specifications. Our tooling engineers will analyze axial stretch ratios, parting line placement, and optimal cooling circuits to deliver a factory-direct quote and DFM report within 24 hours.
Request a Custom Mold Proposal
Direct engineering consultation · NDA protected · 100% confidential.