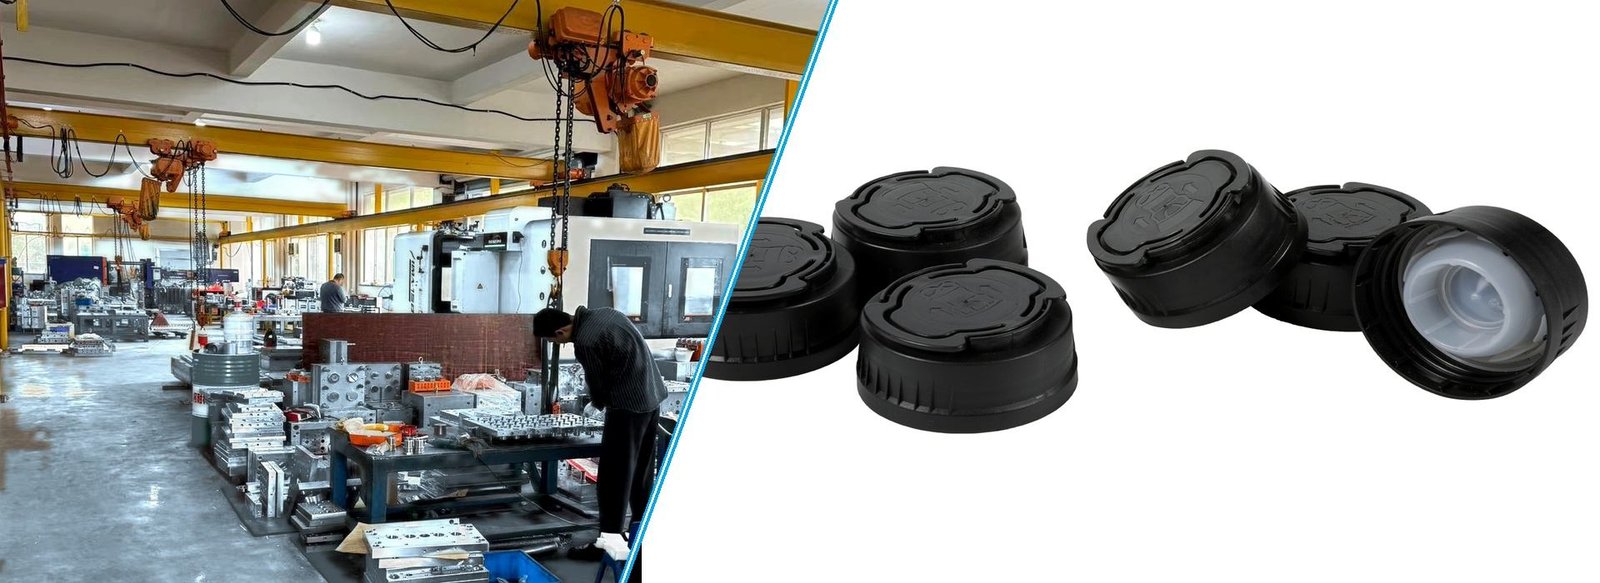
High-Precision Motor Oil Cap Mold & Telescopic Spout Tooling
Engineered for automotive motor oil, synthetic lubricant, and transmission fluid container packaging. Sailwin multi-cavity motor oil cap molds incorporate synchronized dual-threaded core unscrewing, flexible PE bellows spout demolding, and Swedish ASSAB S136 stainless steel, guaranteeing anti-counterfeit tamper-evident ring integrity, zero-leakage inverted funnel pouring, and high-speed 9.5s injection cycles.
Precision Motor Oil Cap Mold Portfolio
Explore our multi-part tooling systems for telescopic pull-out spouts, anti-theft locking rings, and flexible pouring funnels engineered for 1L, 4L, and 5L automotive lubricant jugs.
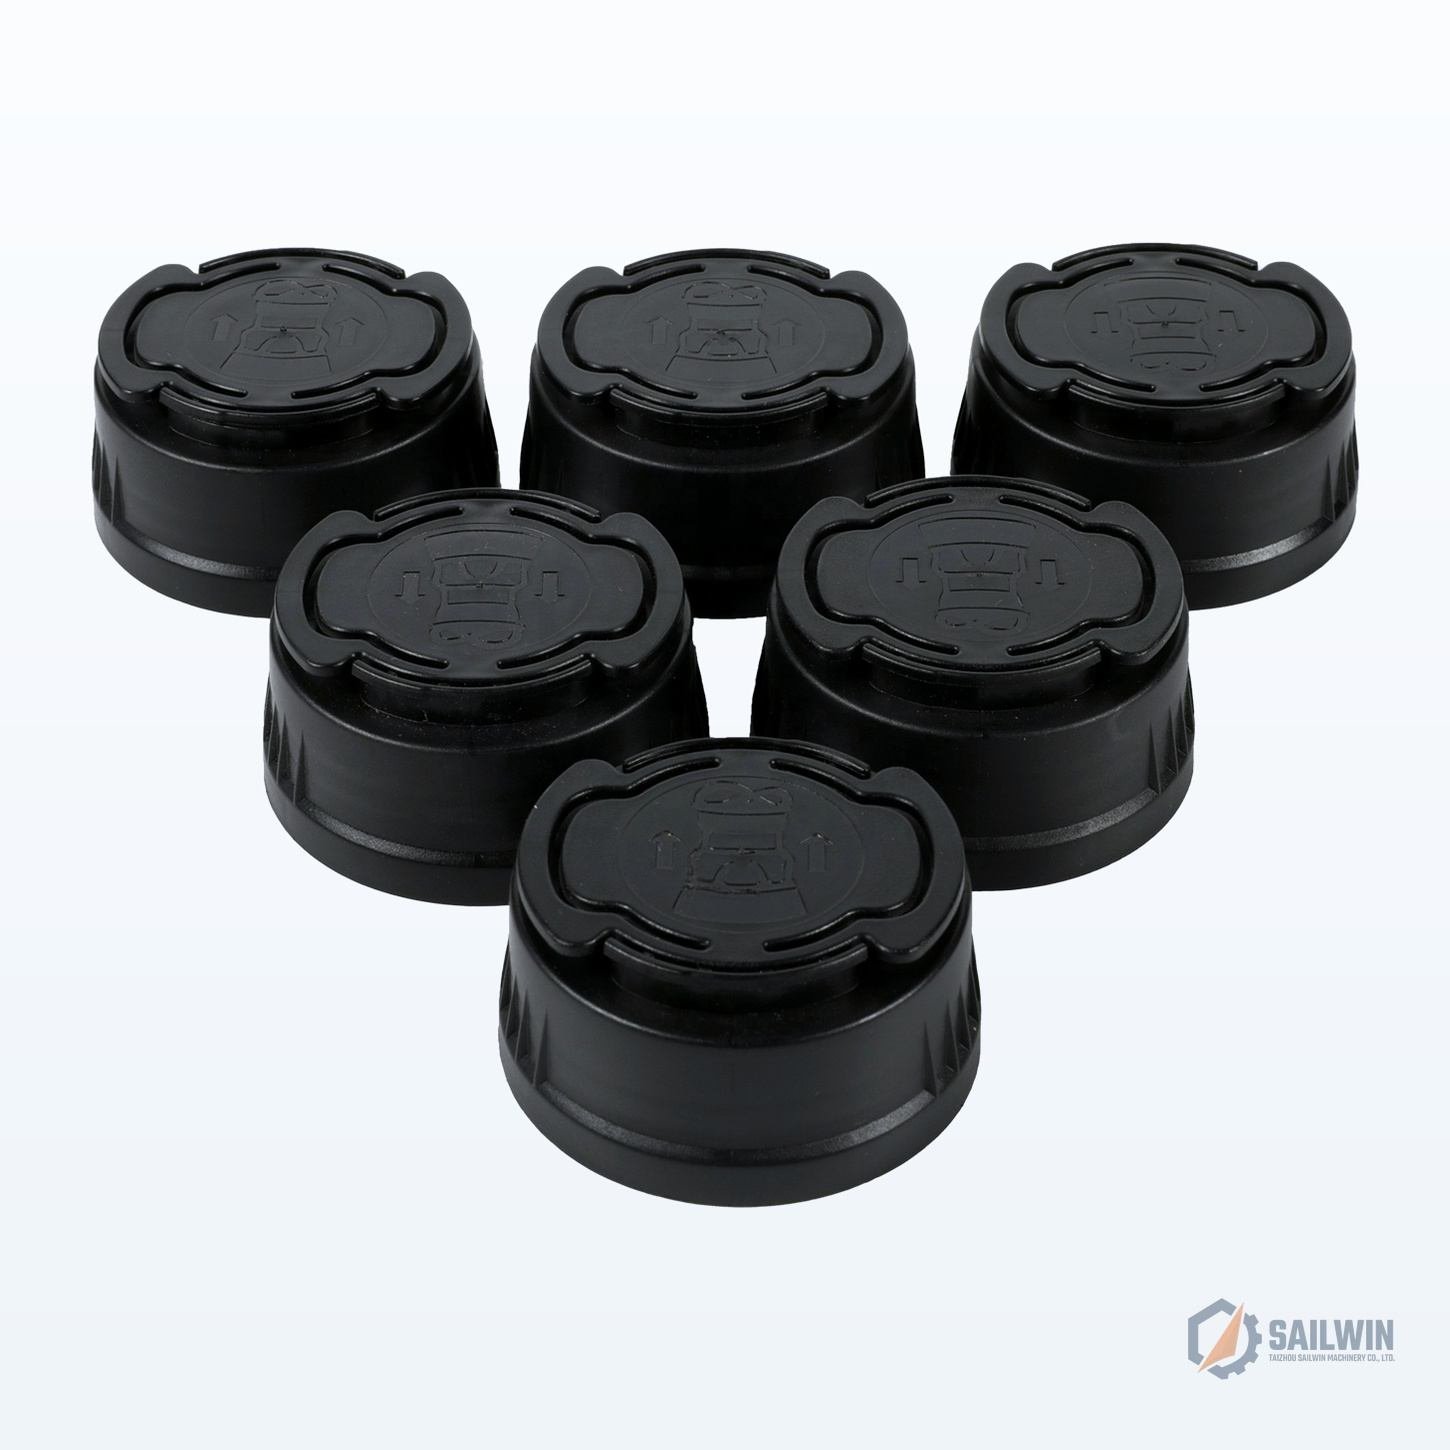 DOUBLE-EAR · 38MM / 42MM
Anti-Theft Double-Ear Telescopic Caps
The global benchmark for passenger car motor oil (PCMO) jugs. Features dual ergonomic finger pull rings and an integral anti-counterfeit snap teeth ring.
- Neck Standards: 38mm / 42mm Ratchet Snap-On Finish
- Telescopic Stroke: 42mm flexible corrugated pull-out tube
- Tamper Proofing: 100% irreversible bridge fracture on opening
- Tooling Cavities: 12, 16, 24 Cavities with unscrewing cores
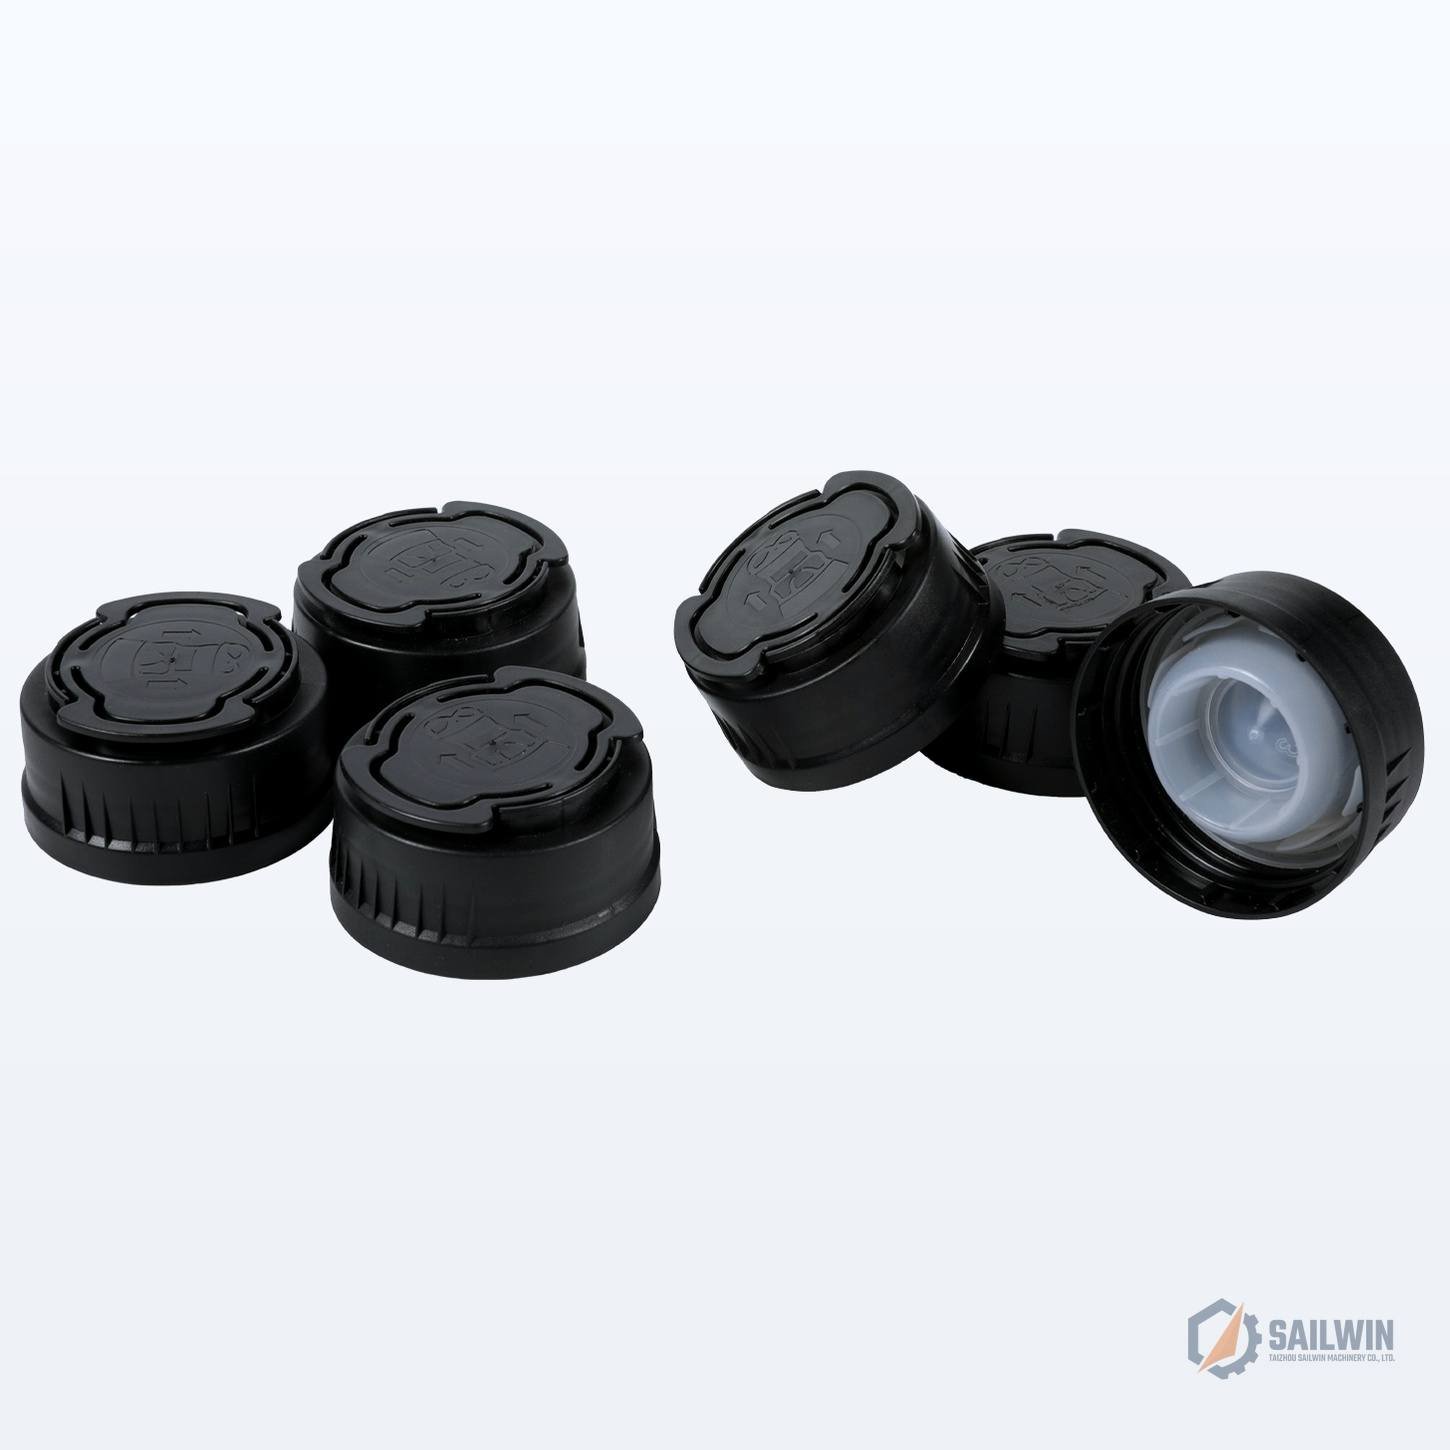 FLEXIBLE TUBE · 42MM / 45MM
Flexible Bellows Pouring Funnel Caps
Engineered with a high-flexibility virgin PE/EVA bellows tube that extends into automotive engine filler necks without requiring an external funnel.
- Anti-Gargle Vent: Dual-channel air compensation eliminates surging
- Induction Seal Flange: Supports hermetic foil heat sealing
- Molding Cycle: 9.8s – 11.2s on high-speed servo presses
- Oil Resistance: Certified for 0W-20 to 15W-40 synthetic lubricants
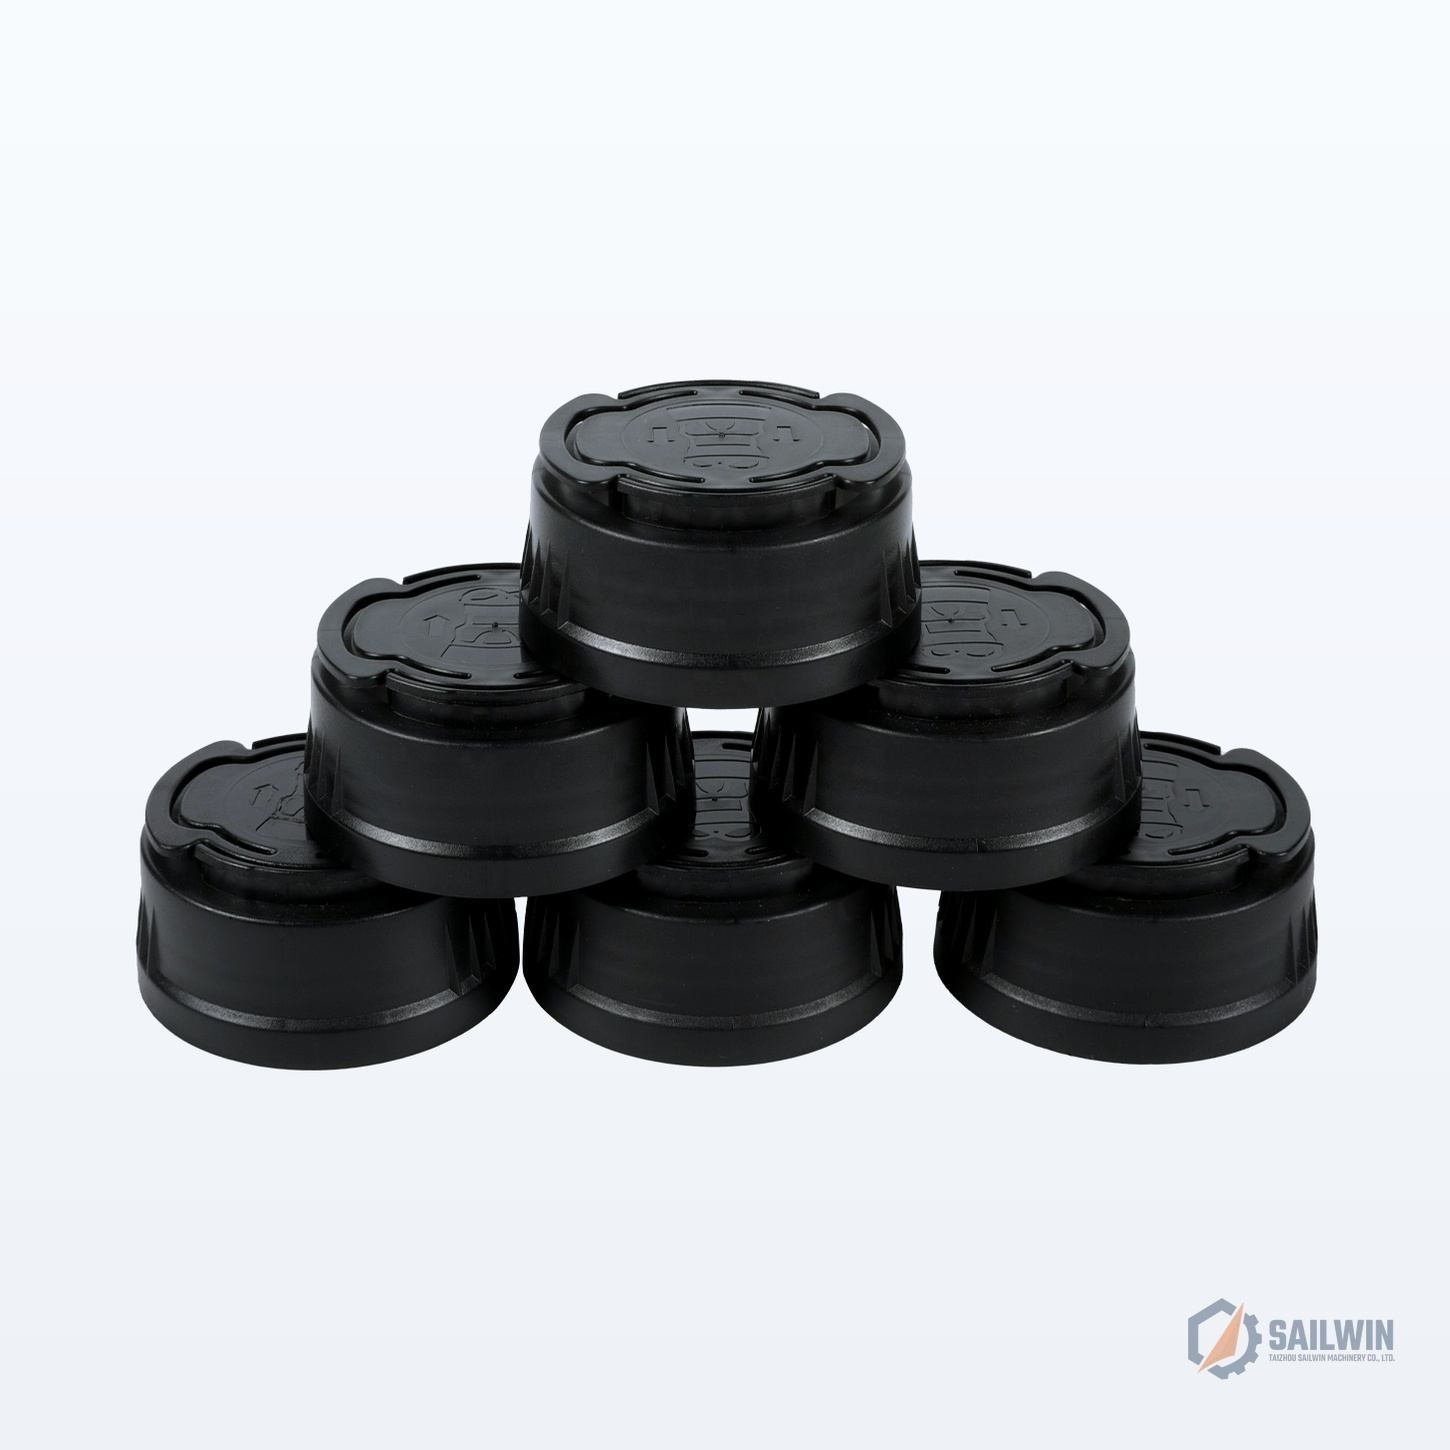 HEAVY DUTY · DIN 45 / 51
Heavy-Duty Lube Oil Spout Closures
Reinforced outer screw skirt designed for 4L–5L heavy-duty diesel engine oil bottles and industrial gear oil containers. Supports high pallet stacking loads.
- Neck Standard: DIN 45 / DIN 51 / 45mm Screw Threads
- Sealing Geometry: Conical bung seal withstands 50°C hot oil
- High-Torque Ribs: 36 perimeter ribs for automatic capper chucks
- Tooling Cavities: 8, 12, 16 Cavities with slide strippers
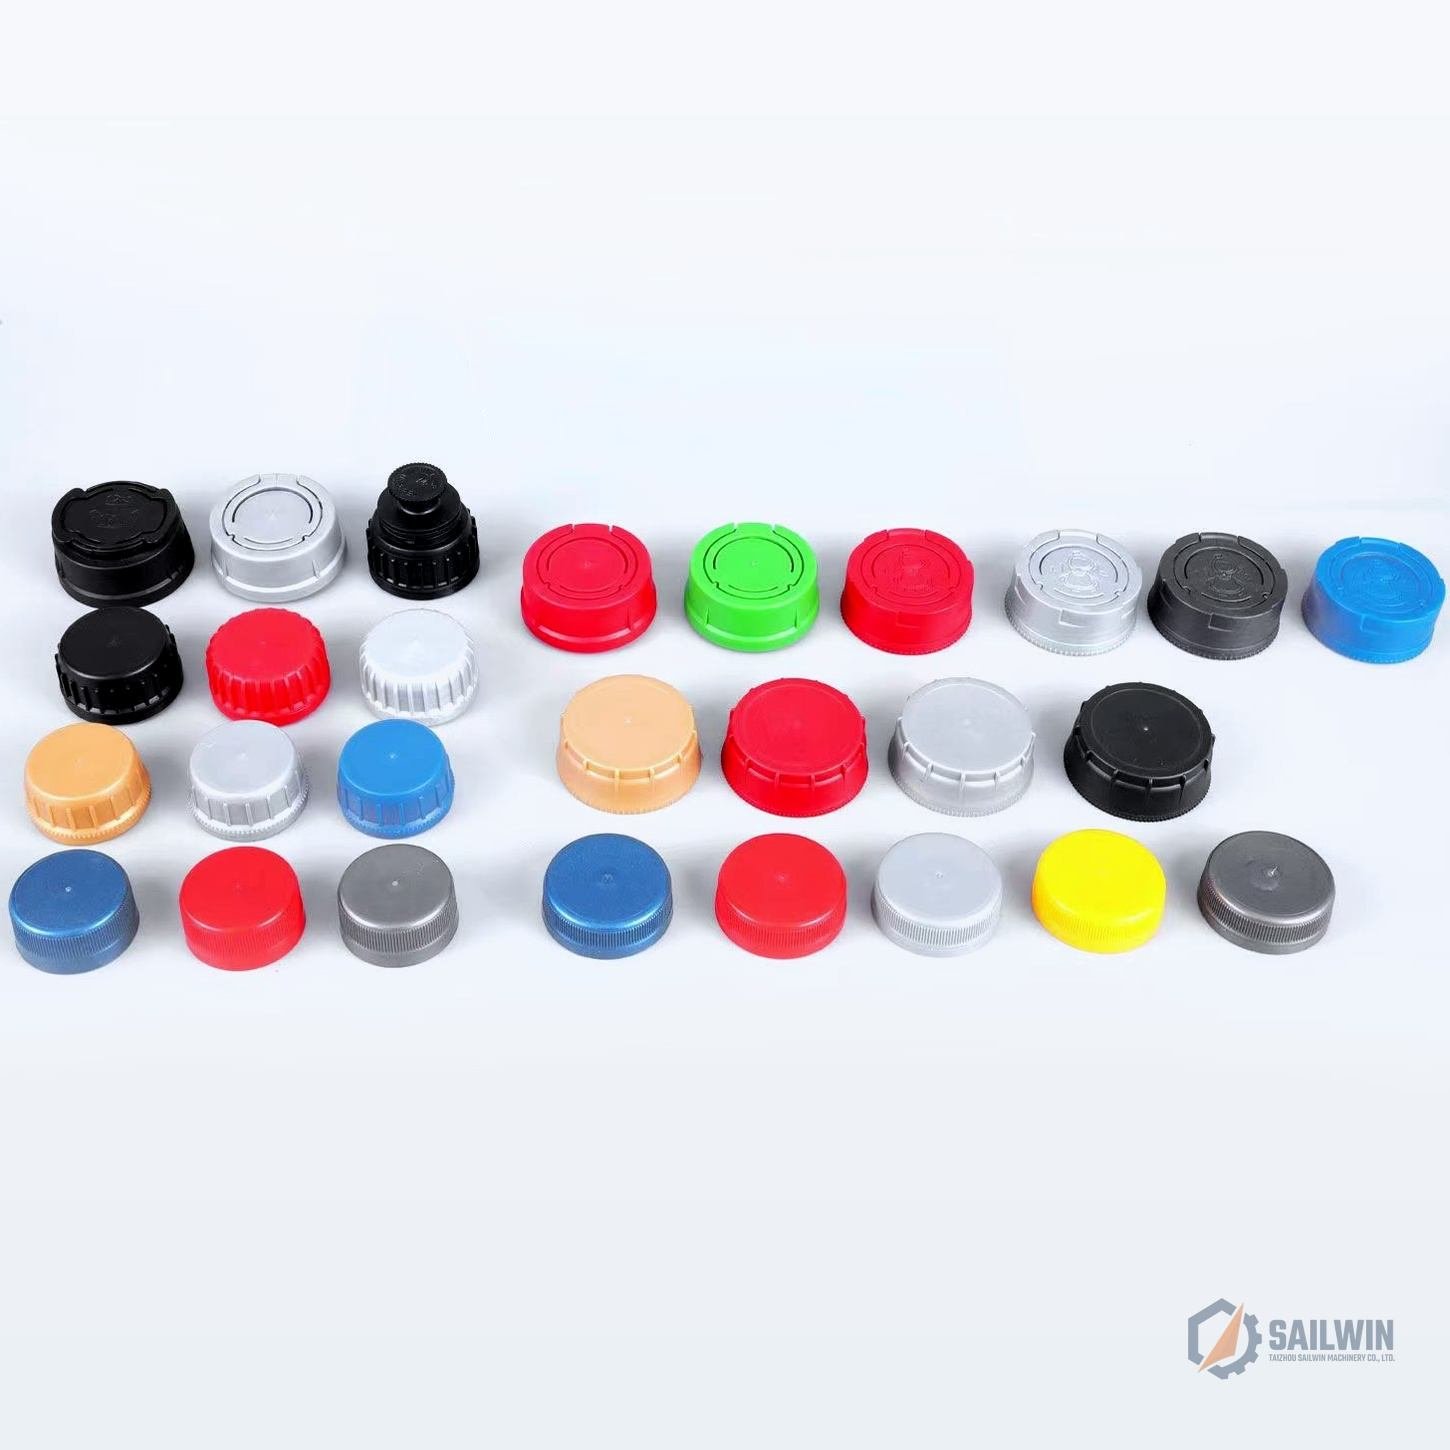 COLOR MATRIX · MULTI-PART
Multi-Color Multi-Piece Closure Matrix
Modular multi-cavity tooling producing matching outer caps, flexible pull-out spouts, and inner tamper seals in metallic gold, red, silver, and blue colors.
- Component Match: Outer Cap (PP) + Flexible Spout (PE) + Seal Plug
- Assembly Speed: 6,000–12,000 caps/hour on rotary assembly line
- Logo Embossing: Laser engraved cavity inserts for 3D brand logo
- Cycle Time: 9.2s – 10.5s for outer shell; 8.5s for spout
| Cavity Count | Closure Component | Neck Standards | Cap Weight (g) | Cycle Time (s) | Rec. Machine Tonnage | Annual Output (8000h) | Action |
|---|---|---|---|---|---|---|---|
| 8 Cavities | Heavy 5L DIN 51 Pull-Out Spout Cap | DIN 51 / 45mm Screw | 18.5g – 24.0g | 11.5s – 13.0s | 180T – 220T | 18 Million pcs | |
| 12 Cavities | Complete 38mm Telescopic Cap Assembly | 38mm Ratchet Snap-On | 14.0g – 17.5g | 10.2s – 11.8s | 220T – 260T | 32 Million pcs | |
| 16 Cavities | Double-Ear Telescopic Outer Cap Shell | 38mm / 42mm Ratchet | 8.5g – 11.2g | 9.5s – 10.5s | 250T – 300T | 46 Million pcs | |
| 24 Cavities | Flexible Corrugated PE Inner Pouring Spout | Universal 38/42mm Core | 4.2g – 6.0g | 8.5s – 9.6s | 200T – 250T | 80 Million pcs | |
| 16 Cavities | Anti-Theft Tear-Off Base Retaining Ring | 38mm / 42mm / DIN 45 | 2.8g – 3.8g | 7.8s – 8.8s | 160T – 200T | 58 Million pcs |
Need Matching Lube Bottle Neck Thread Drawings or 3D Cap Scans?
Our closure tooling directors verify ratcheted anti-theft teeth engagement with your extrusion blow-molded bottle necks within 24 hours.
Engineering Precision: Telescopic Spouts & Unscrewing Cores
Motor oil pull-out caps demand complex internal corrugations, anti-theft ratchet teeth, and leak-proof foil sealing. Explore our field-proven kinematic slide and unscrewing tooling architectures.
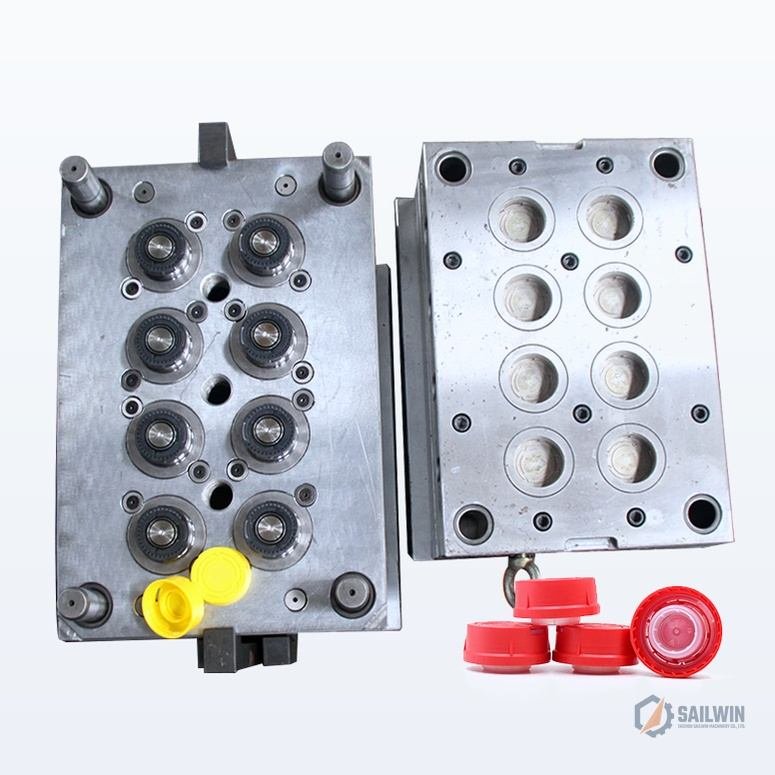 8-CAVITY TELESCOPIC SYSTEM
Synchronized Telescopic Core & Cavity Halves
Telescopic motor oil caps require deep cylindrical cavity draw and precise slide cam guidance to mold the outer knurled shell and inner retaining shoulders without parting line flash.
- • Precision Taper Interlocking: Dual-angle taper guide locks eliminate core shifting under high injection pressure.
- • Micro-Gap Flash Control: Parting line tolerance strictly maintained within 0.015mm.
- • Balanced Needle Valve-Gate: High-speed shut-off leaves a smooth, recessed sub-0.2mm gate vestige.
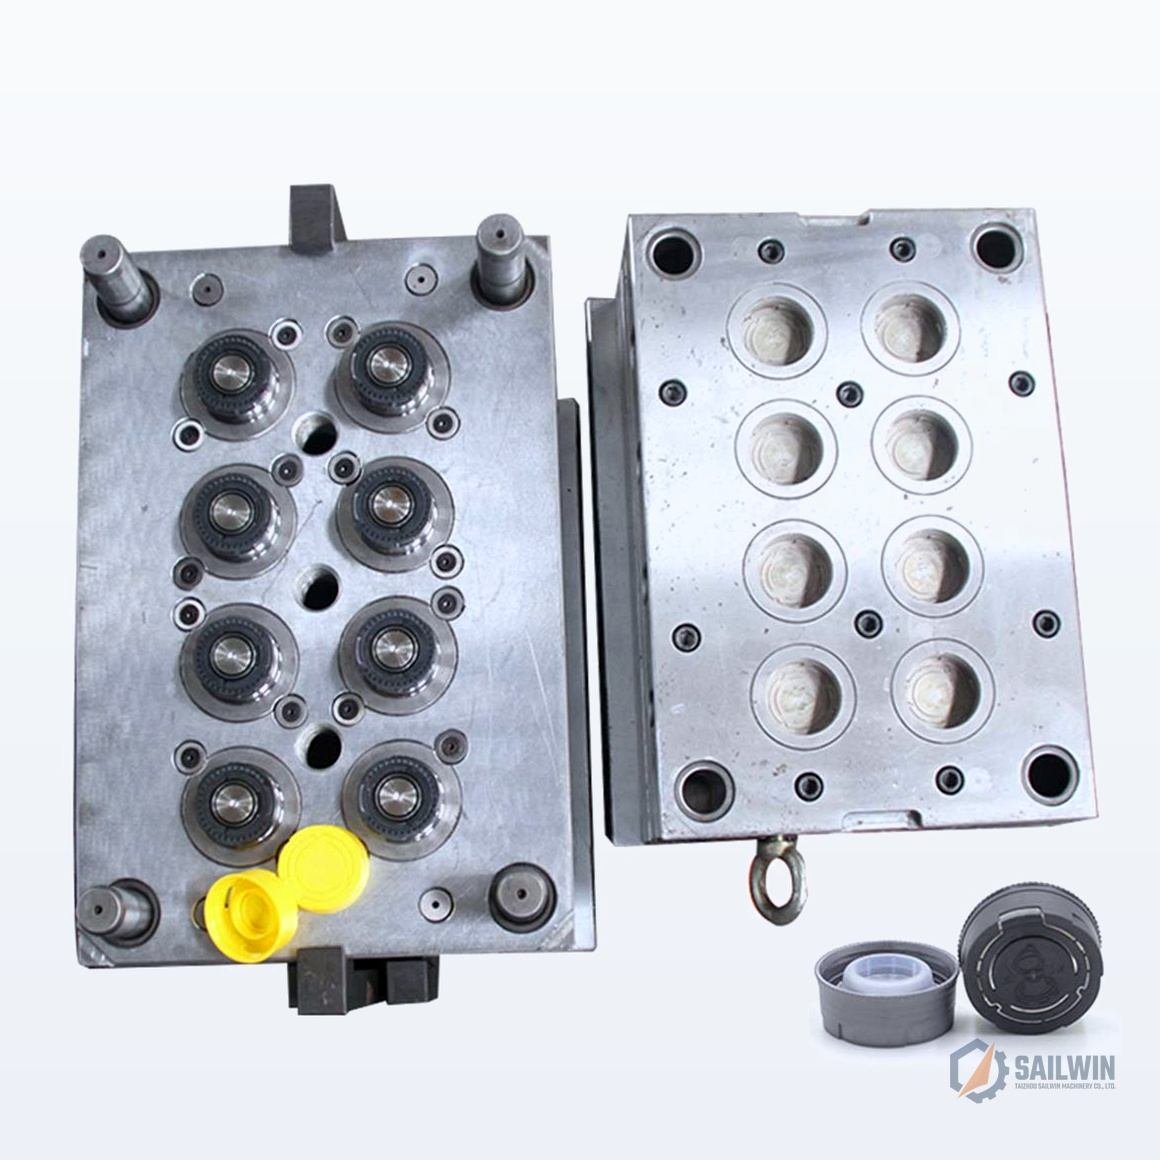 DUAL-THREAD UNSCREWING
Heavy-Duty Dual-Threaded Unscrewing Cores
For continuous-thread heavy lube closures, stripped ejection damages thread crests. Sailwin engineers high-torque hydraulic rack-and-pinion or electric servo rotary unscrewing systems synchronized with machine platen opening.
- • Thread Accuracy: 100% distortion-free pitch profiles compliant with DIN 45/51/60 standards.
- • Rotary Spline Gears: Hardened 20CrMnTi alloy gears running inside oil-bath lubrication chambers.
- • Tamper Band Protection: Retaining ring teeth preserved intact during unscrewing stroke.
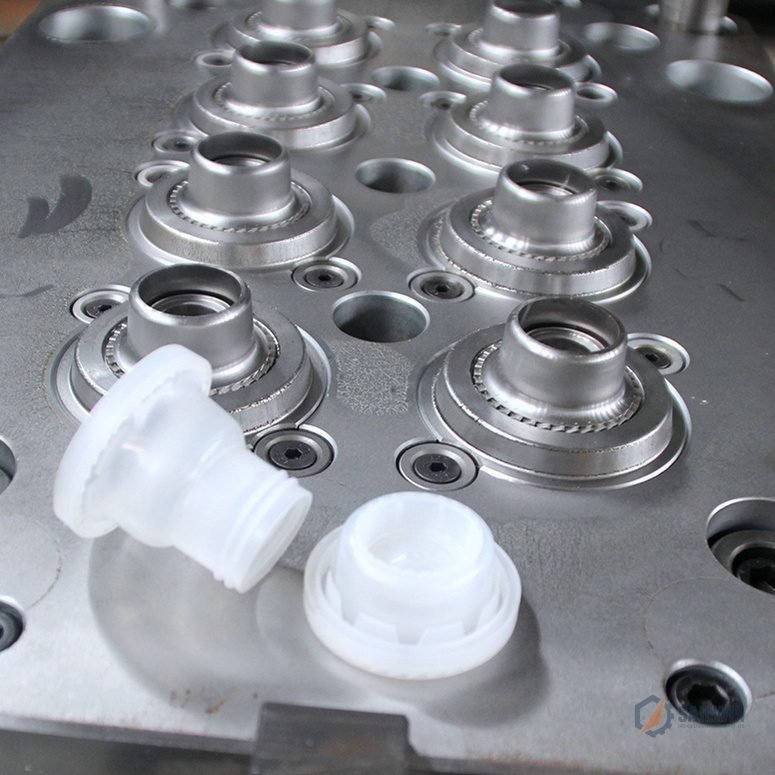 PE BELLOWS SPOUT TOOLING
Flexible PE Corrugated Bellows Tooling
The inner flexible spout features multi-tier corrugated bellows that must collapse flat for shipping and stretch outward smoothly during pouring. Our core tooling incorporates sub-micron sliding segments that demold deep convolutions without tearing.
- • Resin Compatibility: Optimized for food-grade virgin LDPE and EVA copolymer formulations.
- • Zero Corrugation Pinholes: Precision air venting prevents localized air traps in thin bellow walls.
- • Pull-Out Stroke: Smooth telescopic elongation extending 42mm beyond the cap rim.
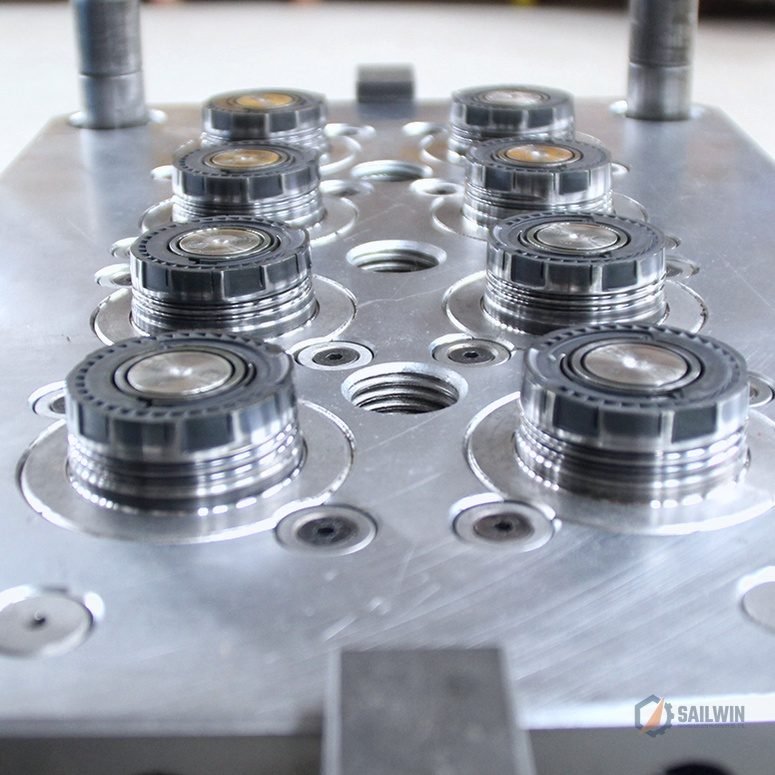 BERYLLIUM COPPER COOLING
Beryllium Copper Core Inserts & Fast Cycles
Deep core cavities in pull-out oil caps trap heat, leading to sink marks and extended cooling delays. Sailwin inserts Japanese C17200 beryllium copper crowns into every core tip, multiplying heat dissipation speed by 300% compared to tool steel.
- • Cycle Reduction: Heavy 16g lube caps achieve rapid 9.5s–10.5s injection cycle times.
- • Sink-Mark Free: Eliminates thermal shrinkage dimples around thick internal seal flanges.
- • Direct Tip Baffling: Bubbling water circuits deliver 10°C chilled water directly to copper crowns.
Imported S136 Metallurgy & Heavy Plate Precision
Motor oil pull-out caps involve sliding ratchets, internal threads, and flexible PE bellows. Sailwin ensures zero cavity deflection, flash-free parting lines, and 3,000,000+ shots tool longevity.
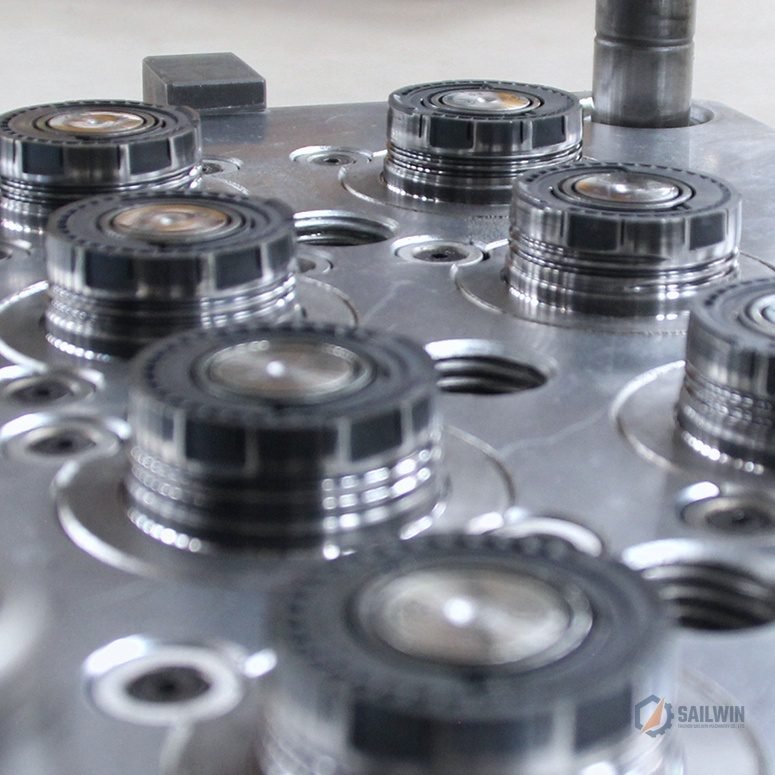
8-Cavity Core Plate & Heavy Guide Pillars
Equipped with 4 oversized hardened 20Cr guide pillars and graphite-bronze self-lubricating bushings. Stripper ring travels smoothly to demold deep telescopic internal ribs.
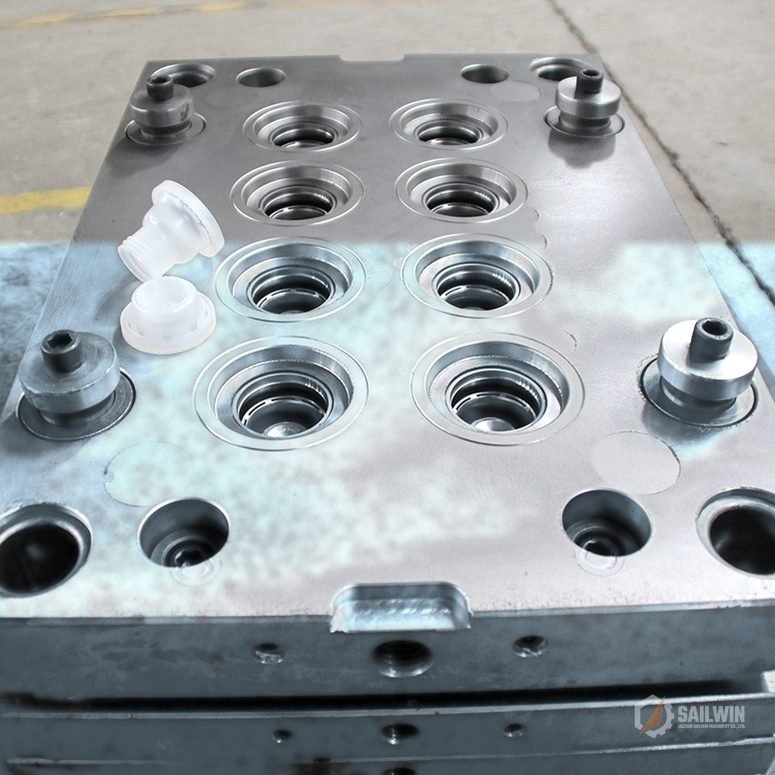
8-Cavity Cavity Plate with Molded Nozzles
Shown with molded translucent PE flexible pouring nozzles on our clean workshop floor. Cavities are diamond mirror polished to Ra 0.05μm to ensure pristine outer cosmetic finish.
Swedish ASSAB S136 Stainless Steel
Premium electroslag remelted (ESR) stainless steel vacuum heat-treated to HRC 50–52. Resists synthetic ester motor oil and chemical lubricant additives with zero corrosion pitting.
- Vacuum Quenching: HRC 50 – 52
- Cavity Mirror Finish: Ra 0.05 μm (SPI A1)
- Guaranteed Tool Life: 3,000,000+ Shots
- Synthetic Oil Proof: 100% Non-Corrosive
Japanese Daido NAK80 Tool Steel
Pre-hardened mirror-grade steel used for side slide cams and stripper blocks. Delivers superior dimensional stability and high thermal conductivity to accelerate cap thread cooling.
- Hardness Delivery: HRC 38 – 42
- Slide Precision: ±0.003mm Fit
- Thermal Conductivity: 41.3 W/m·K
- Wear Surface: DLC / TiN Coated
High-Rigidity Mold Base Plates
High-tensile structural tool steel normalized and stress-relieved to prevent plate deflection under 300T clamping pressure. Preserves micro-gap flash control across all cavities.
- Base Hardness: HRC 32 – 36
- Plate Flatness: ≤ 0.015mm / Meter
- Guide Bushings: Bronze with Graphite
- Tensile Strength: 1020 MPa High Rigidity
Tooling Assembly Bays & Live Machine FAT Trials
Take a virtual tour of our 15,000m² specialized closure tooling campus in Taizhou, China. Over 30 CNC machining centers, high-tonnage trial presses, and heavy crane assembly floors dedicated to multi-cavity lube cap tooling.
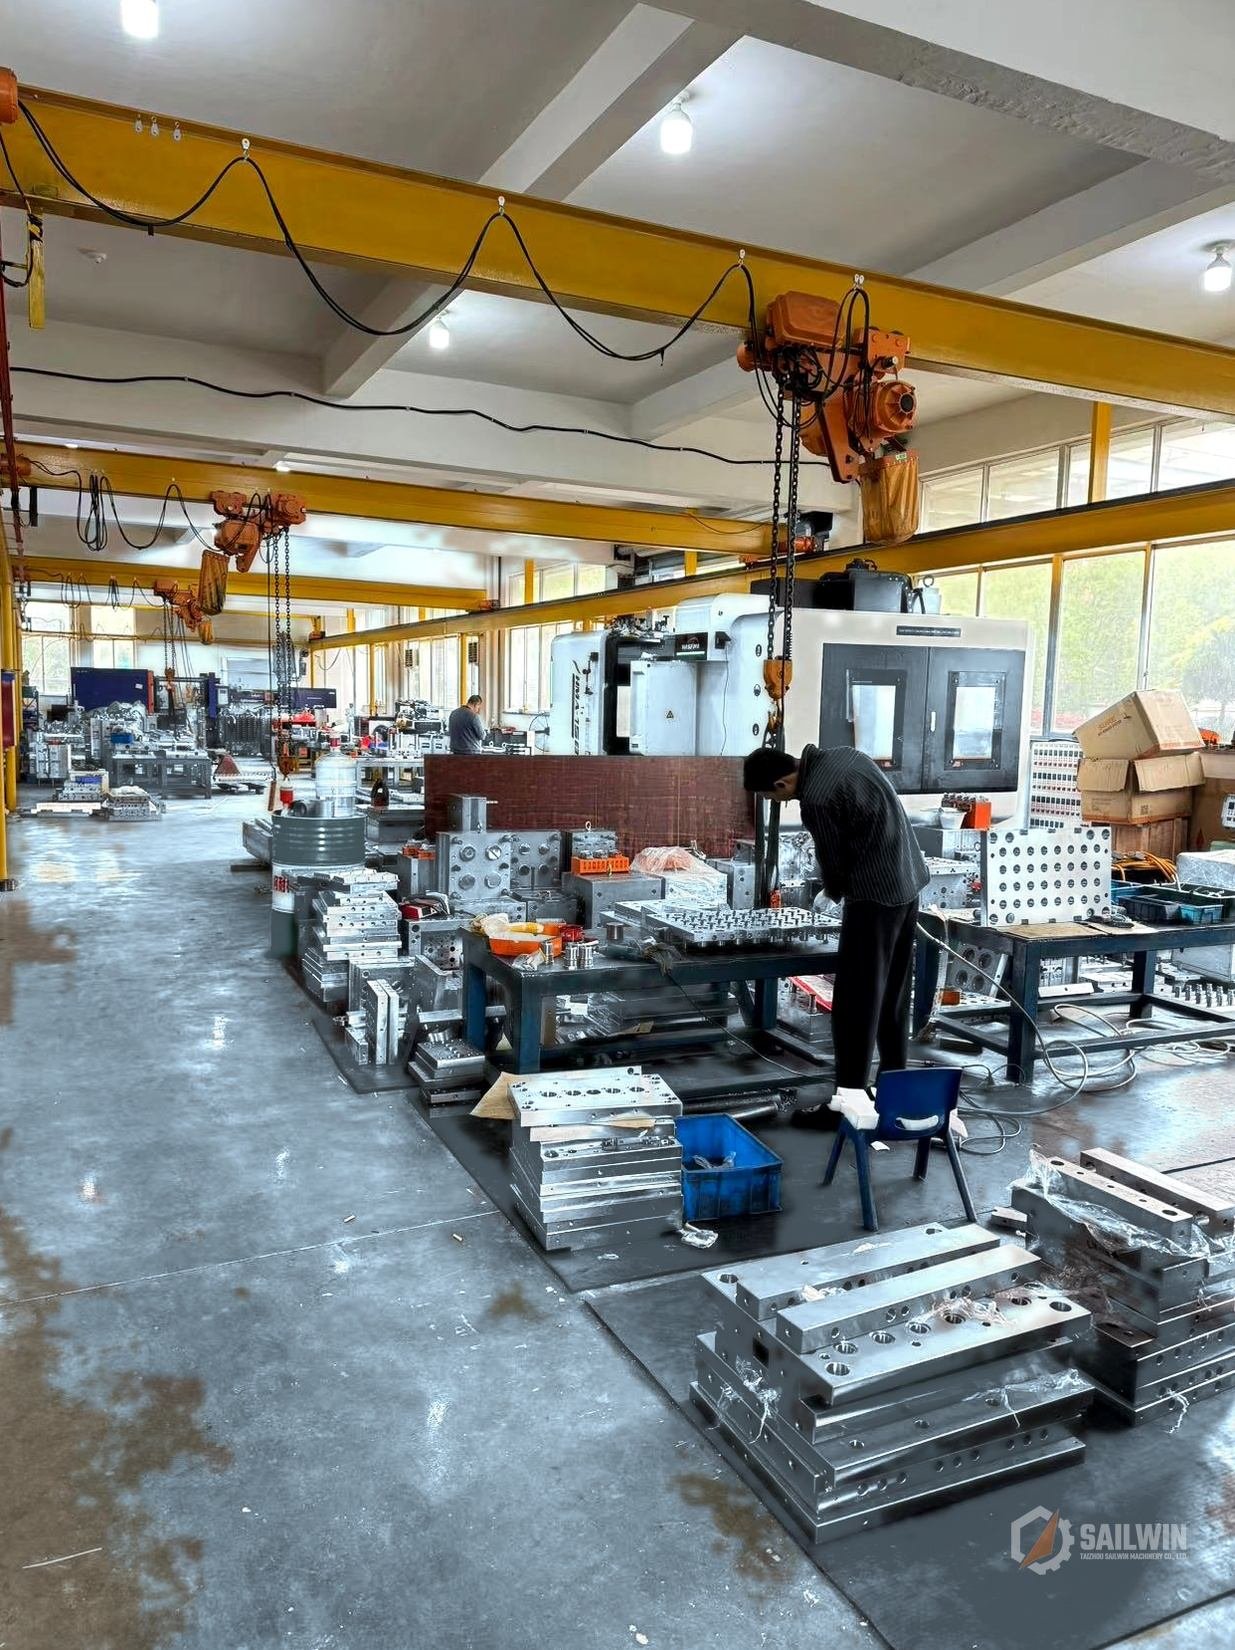
Heavy Tooling Fitting & Crane Rigging
Equipped with distressed sky-blue epoxy flooring, high-tonnage hydraulic mold spotting presses, and dual 15-ton overhead traveling cranes. Experienced master fitters ensure 100% blue lead spotting across slider locking wedges.
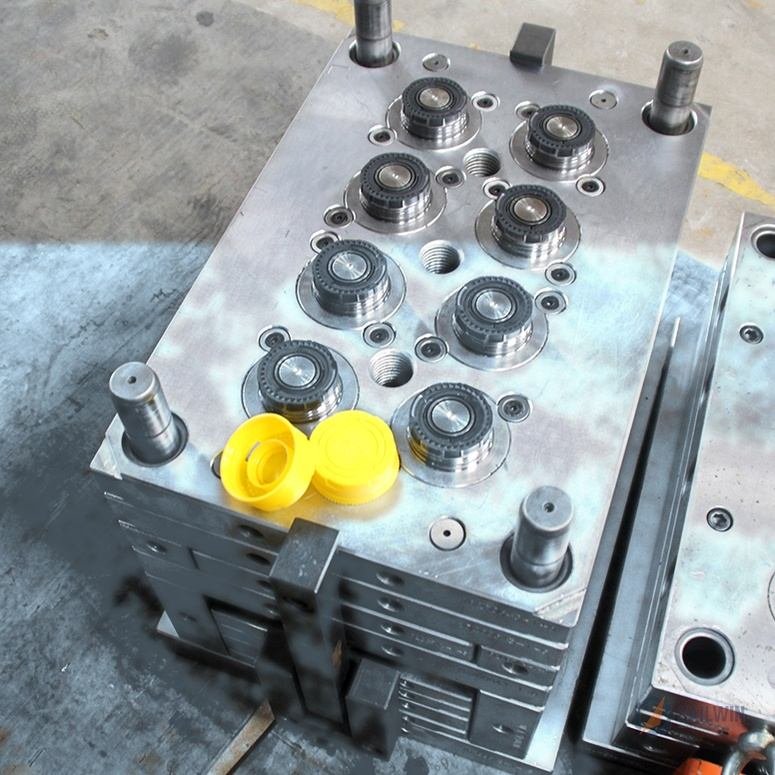
Core Plate Final Bench Fitting
8-cavity pull-out spout cap core plate resting on our clean workshop floor following precision slider alignment and hydraulic unscrewing rack calibration.
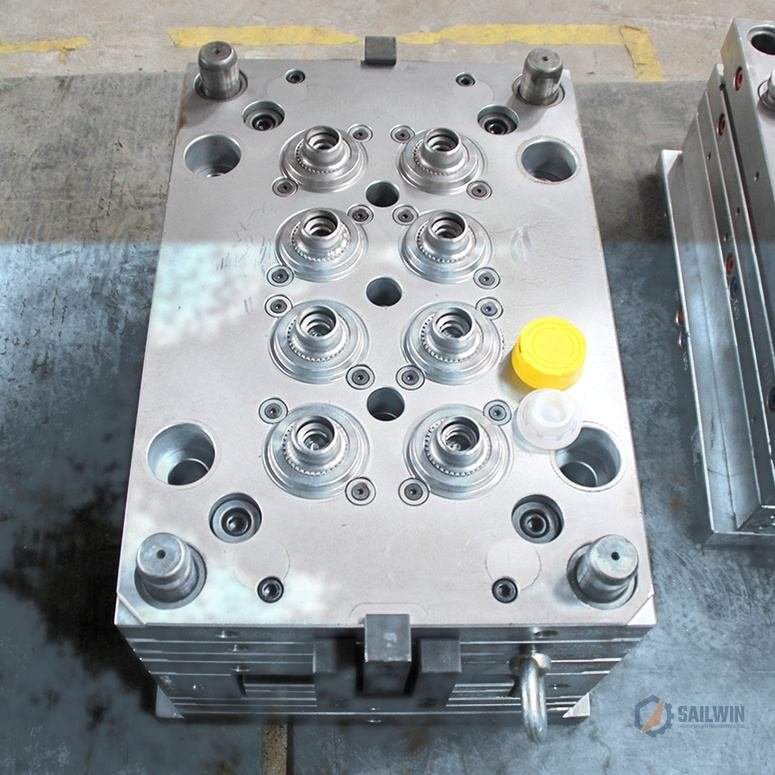
Completed Mold Assembly & Cap Samples
Assembled mold tooling displayed with molded yellow safety pull-out spout caps on our blue floor, ready for crating and customer witness sign-off.
Product Showroom & Tooling Navigation Hub
Explore our comprehensive range of anti-counterfeit motor oil telescopic spout caps, plus direct gateways to matching blow molds and drum tooling.
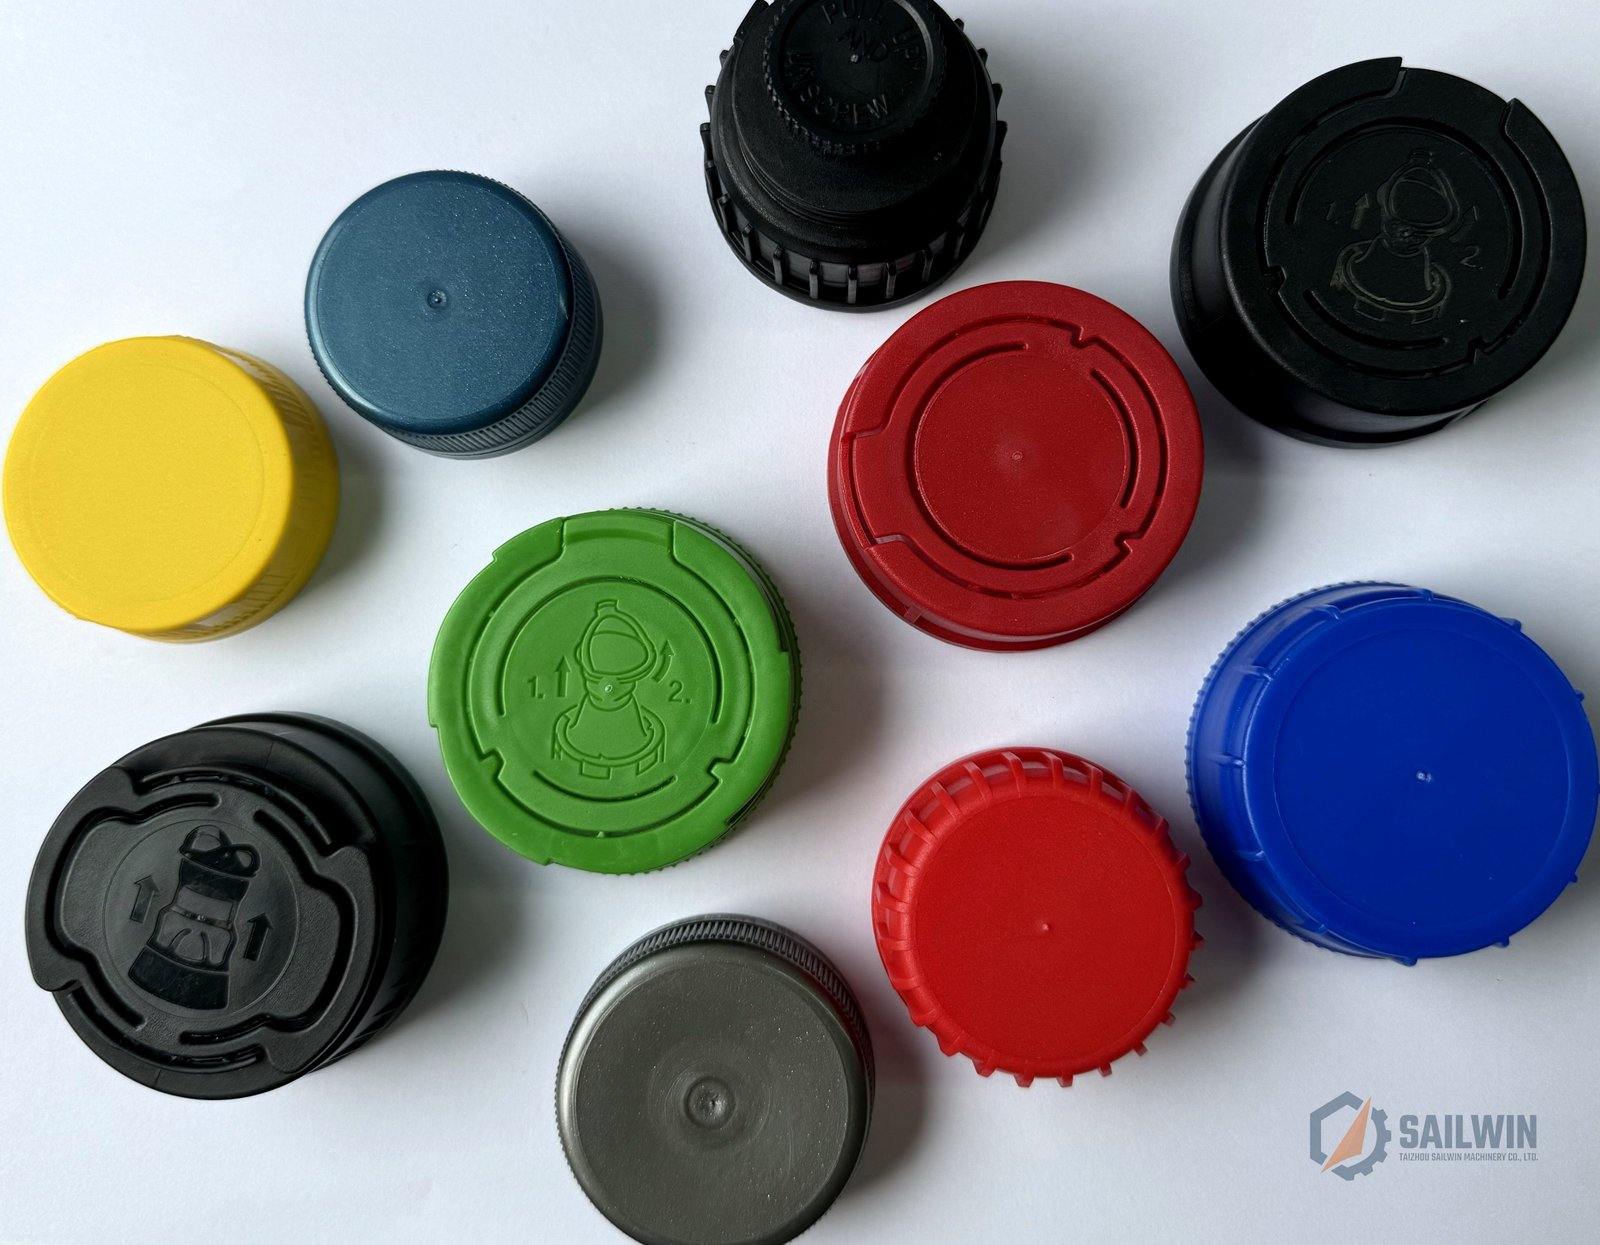
Tier-1 Lubricant Packaging Tooling
Custom engineered for global oil majors. Multi-part closure tooling integrating tamper-evident tear rings, telescopic flexible pouring funnels, and precision induction foil seal flanges for 1L to 5L lubricant jugs.
Closure Macro Details & Multi-Color Portfolio
6-piece multi-color lube closures, top directional pull-rings, and knurled anti-slip skirts.
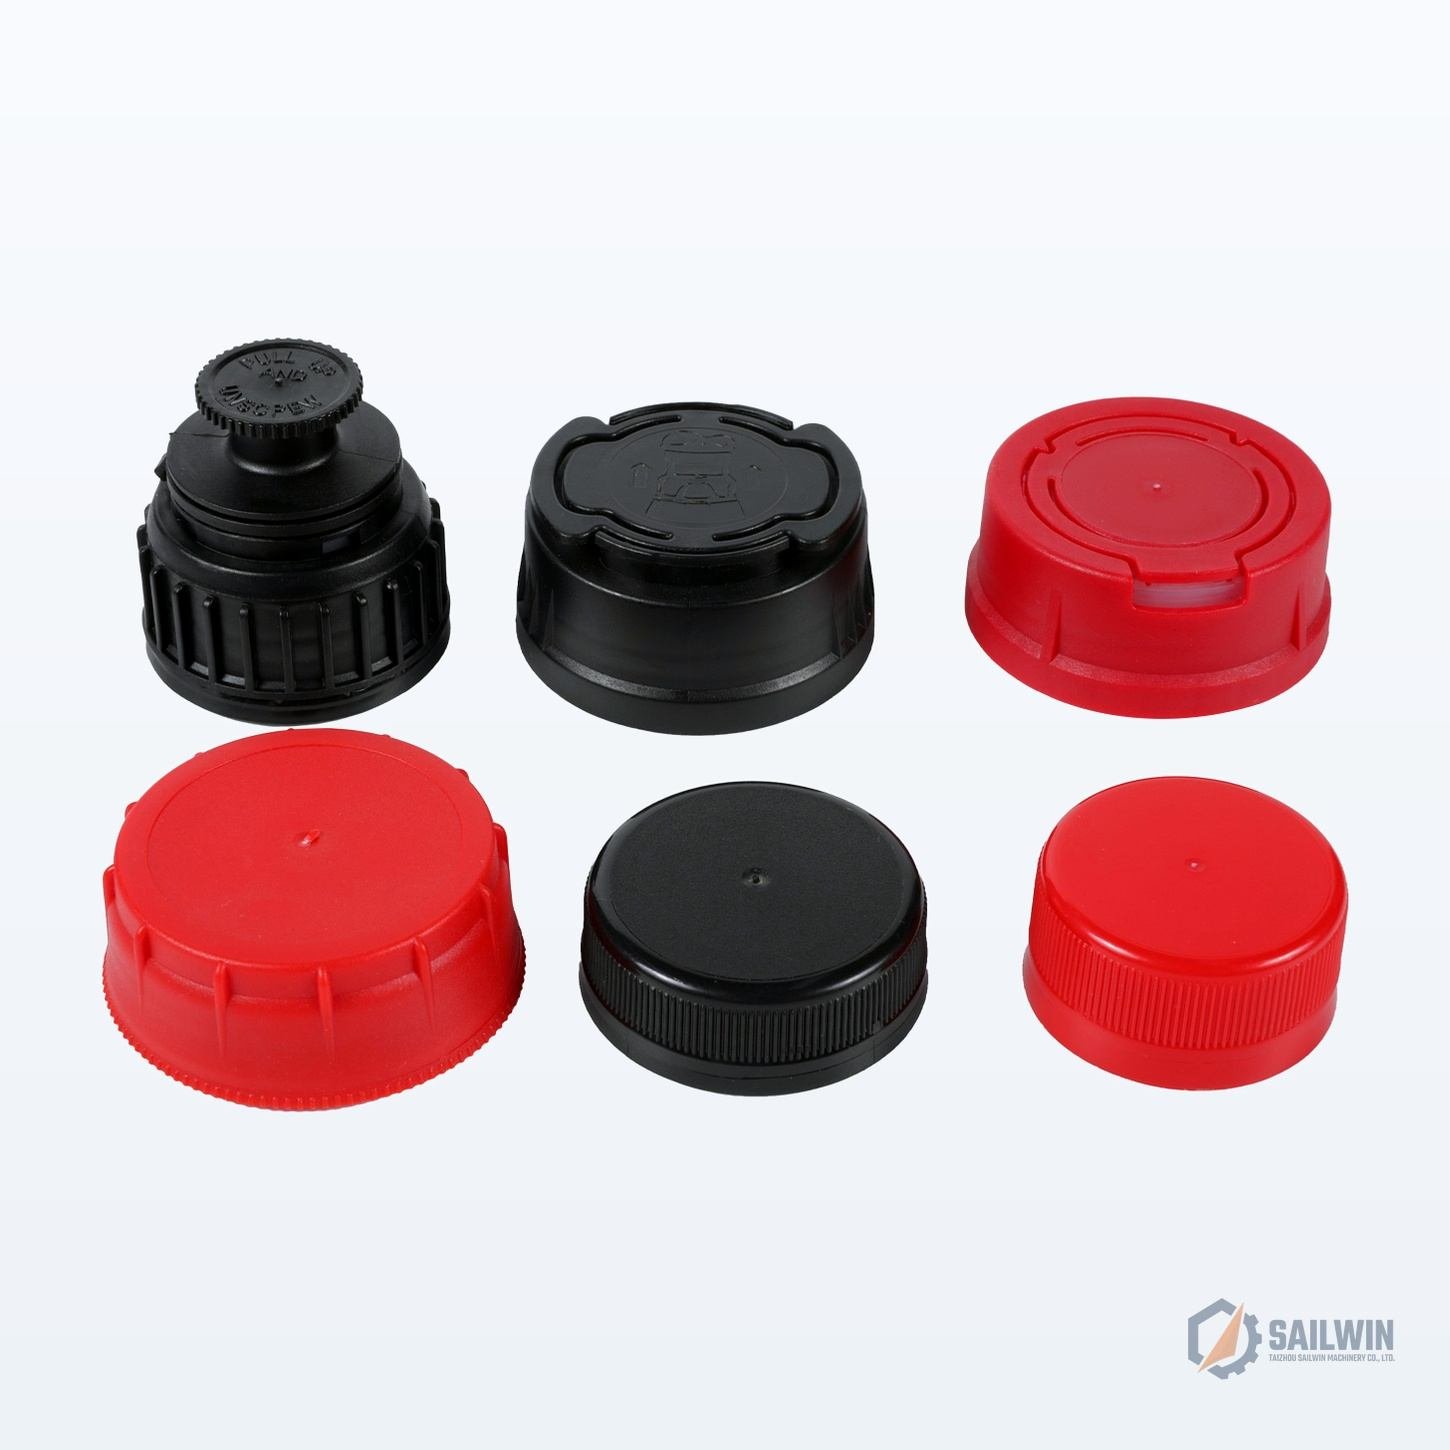
6-Color Lubricant Cap Lineup
Custom masterbatch formulation matching brand corporate colors in silver, red, gold, blue, and black with high UV stability.
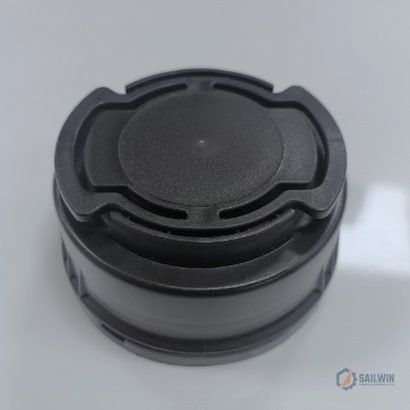
Embossed Directional Pull-Ring
Ergonomic double-ear pull ring with laser-etched directional arrows, ensuring effortless 35N tear opening for end users.
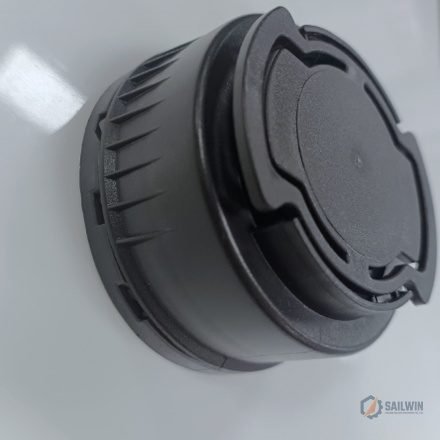
Knurled High-Torque Skirt
36 perimeter vertical knurls provide high friction grip for high-speed capping chucks without galling or plastic deformation.
Zero-Counterfeiting & Zero-Leakage for Top Lube Brand
A leading synthetic motor oil packaging converter installed 16-cavity telescopic pull-out cap molds from Sailwin. Operating at 9.8 seconds cycle time, the converter produced over 60 million cap assemblies annually with 100% anti-counterfeit ring fracture upon initial opening and zero sea-freight leakage complaints across 40 countries.
Turnkey Downstream Tooling & Sub-Pages
Explore matching blow molds, jerry cans, drum molds, and parent category collection hubs.
Lube & Motor Oil Bottle Blow Molds
HDPE multi-cavity extrusion blow molds with view stripe liquid indicators and calibrated neck threads.
Jerry Can & Chemical Drum Molds
10L–30L stackable jerry can extrusion blow molds with UN drop-test certified handle and bottom pinch-off.
200L Large Drum Blow Molds
Accumulator head blow tooling for 200L/220L tight-head L-Ring chemical drums with C17200 pinch blades.
Plastic Injection Molds Hub
Explore all 9 closure categories, preform tooling systems, and custom precision plastic injection tooling.

