Heavy-Duty Extrusion Blow Molding & EBM Tooling Solutions
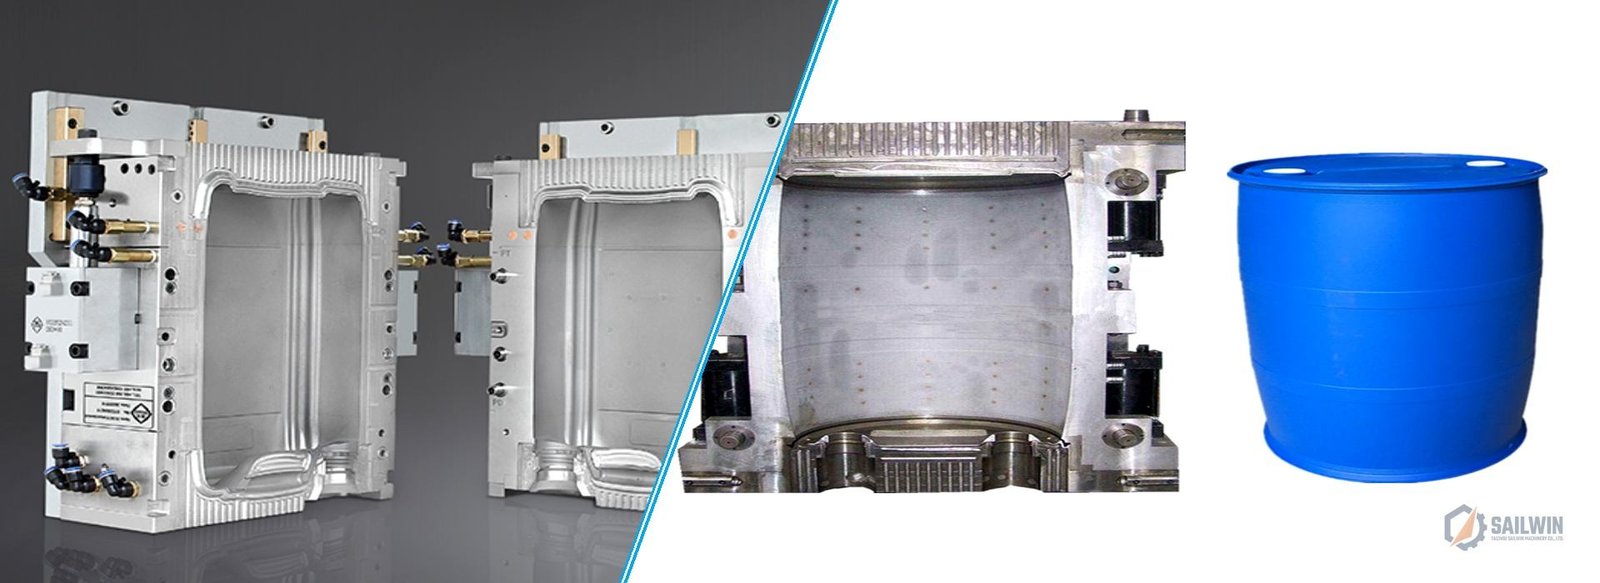
Industrial-grade extrusion blow mold engineering for HDPE, PP, and multi-layer EVOH containers. Covering 1L–30L chemical jerry cans, lube oil bottles with view stripes, 200L L-ring drums, and technical automotive ducts. Engineered with Japanese C17200 beryllium copper pinch-offs and pre-hardened P20/718H steel to deliver clean parting line shear and 5,000,000+ cycles.
Extrusion Blow Molds by Container Application
Precision-engineered for continuous shuttle and accumulator-head extrusion blow molding machinery. Equipped with beryllium copper pinch-offs and automated deflashing shears.
 1L – 30L JERRY CANS
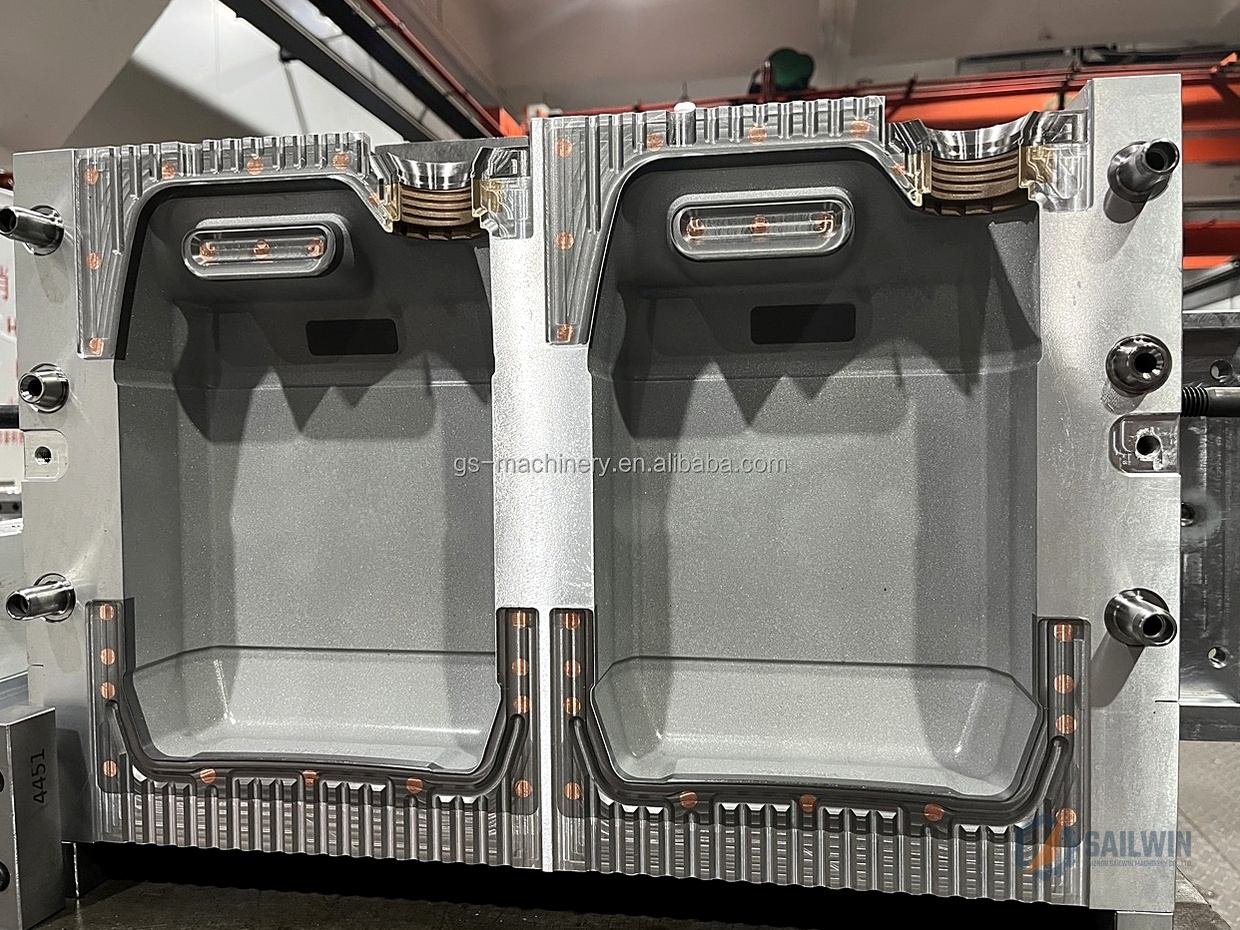
Jerry Cans & Stackable Chemical Jugs
Engineered for UN-certified chemical jerry cans and edible oil containers. Features high-hardness golden beryllium copper pinch-offs and hydraulic core-pulling handles.
- Volume: 1L, 5L, 10L, 20L, 25L, 30L
- Pinch-Off: Japanese C17200 Beryllium Copper
- Handle: In-mold sliding cores for hollow handles
- Deflashing: Automated neck and tail trim shears
 100ML – 5L BOTTLES
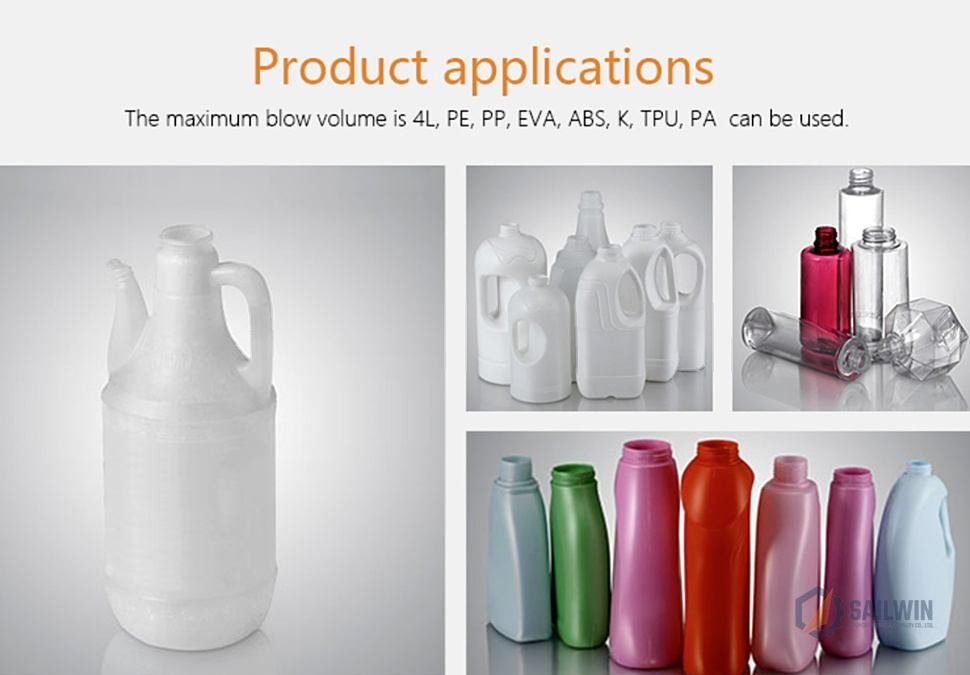
Motor Oil & Detergent HDPE Bottles
Multi-cavity high-efficiency tooling for motor oil bottles, laundry detergents, shampoo, and agrochemical bottles. Compatible with transparent view-stripe parisons.
- Volume: 100ml, 500ml, 1L, 4L, 5L Packs
- Features: Angled neck split rings & view-stripe alignment
- Material: Pre-hardened tool steel P20 / 718H / S136
- Cycle Time: Fast dry cycle with high-flow cooling
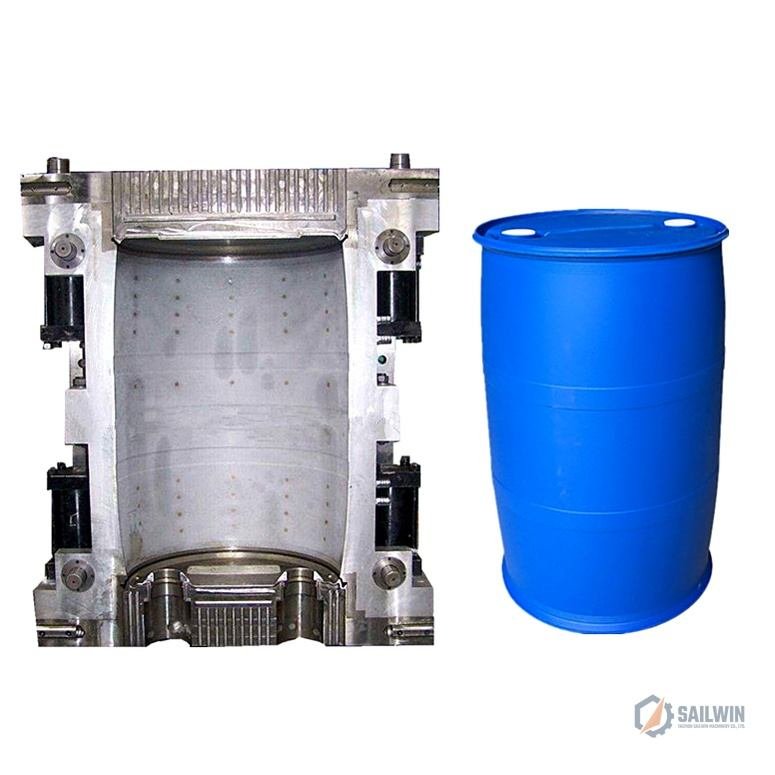 50L – 1,000L ACCUMULATOR
200L L-Ring Drums & Large Industrial Tanks
Heavy-duty accumulator head tooling for 200L L-ring and double-tight head chemical drums, IBC tank containers, floating docks, and automotive technical blow parts.
- Volume: 50L, 100L, 120L, 200L, 220L, 1,000L
- Clamping: Extreme high-rigidity structural frame
- Cooling: High-volume deep-gun-drilled water lines
- Standard: Passed UN drop, stack & hydrostatic tests
Extrusion Blow Mold Engineering: Pinch-Offs & Auto-Deflashing
Precision pinch-off blade geometry and cooling rate balance determine seam drop strength and cycle speed. Explore our four fundamental EBM engineering breakthroughs.
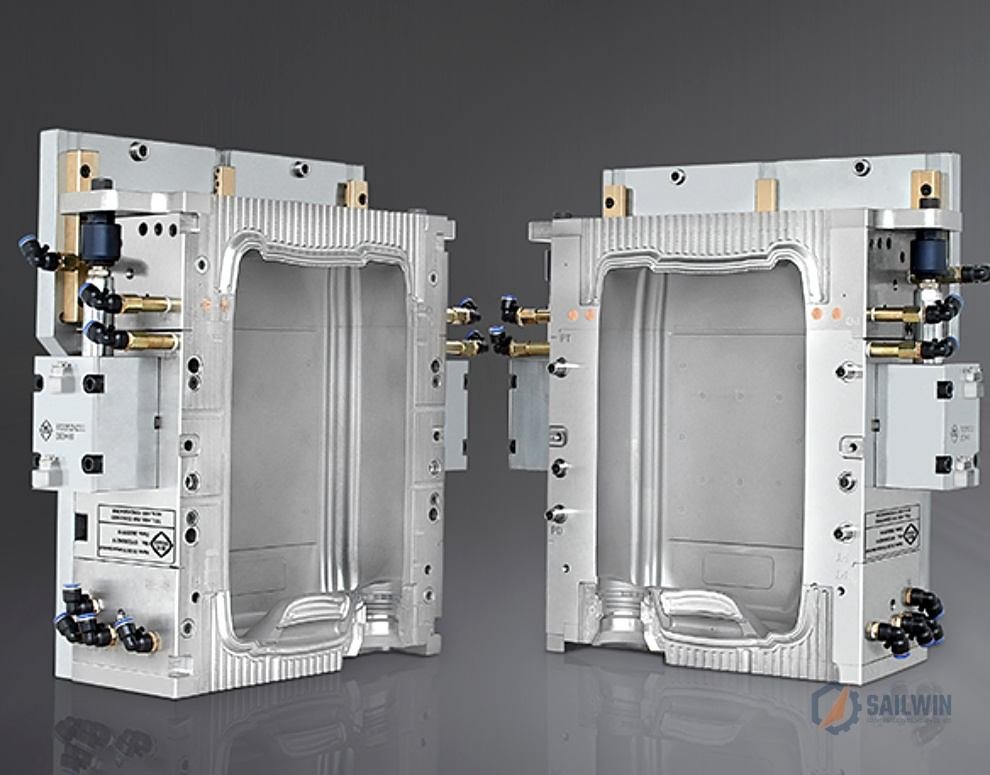 C17200 BERYLLIUM COPPER
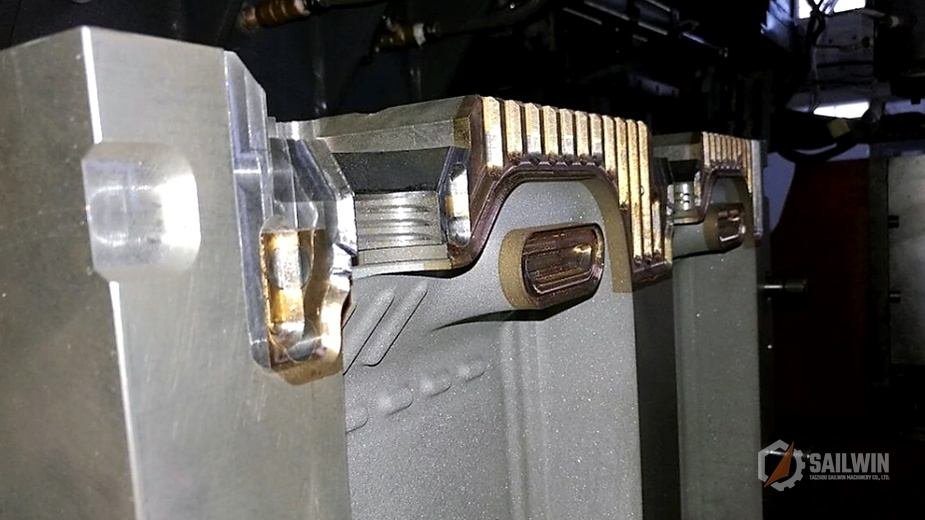
Japanese C17200 Beryllium Copper Pinch-Off Inserts
Thick parison weld seams around handles and bottle bottoms are prone to weak seam welding or slow cooling. We embed high-hardness Japanese C17200 beryllium copper along all pinch-off land areas.
- Thermal Conductivity: 350% higher than tool steel, eliminating weld seam burn
- Blade Hardness: HRC 38–42 prevents pinch-off blade edge chipping over millions of cycles
- Seam Welding: Dual-angle land angle design guarantees 100% burst-proof bottom seams
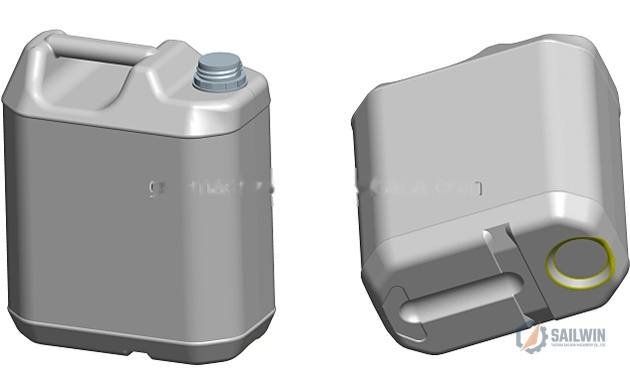 STACKABLE 3D CAD
Stackable Chemical Jerry Can 3D Design & FEA
Chemical drums must pass severe UN hazardous drop and 3-meter stacking load tests. Our parametric CAD designs incorporate top-to-bottom interlocking feet and side corner ribbing to prevent collapse.
- Interlocking Nests: Top handle nest interlocks with bottom base well for 3-tier warehouse stacking
- Corner Radii: Generous corner radii prevent parison corner thinning during blow expansion
- UN Drop Compliance: Certified to pass 1.8-meter zero-leak drop testing with antifreeze
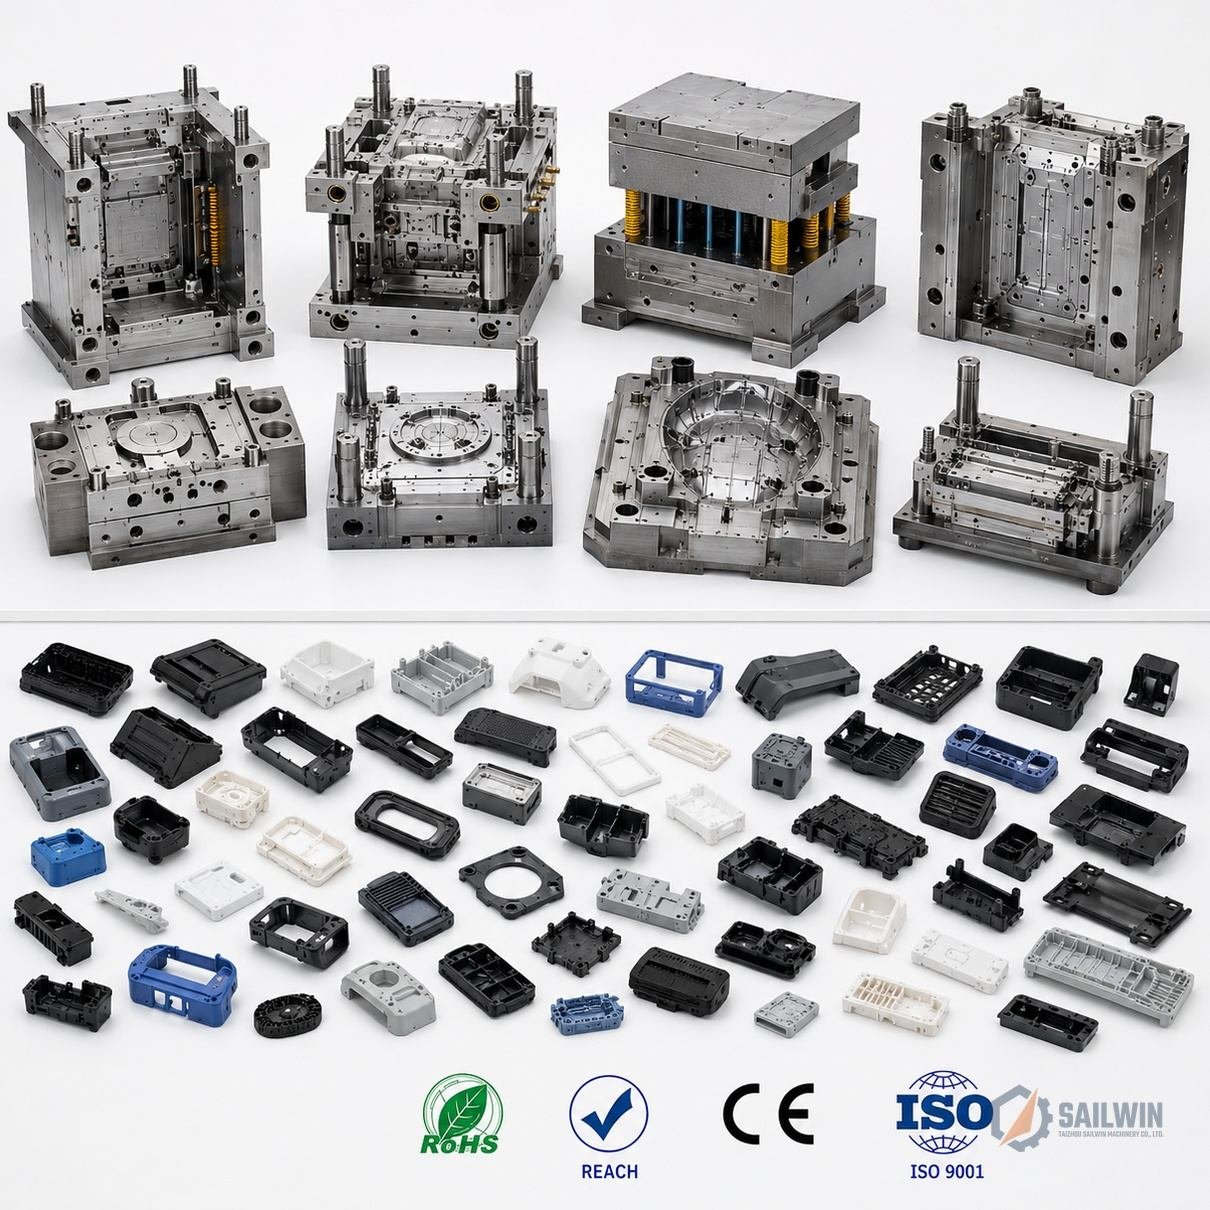 10-STEP QC PROTOCOL
10-Step Precision Mold Manufacturing & QC Flowchart
Every extrusion blow mold undergoes strict staged verification: 3D parison simulation, CNC roughing, deep gun-drill water circuits, manual fitment, and machine FAT dry trials.
- Step 1–3: 3D container styling, parison programming & steel spectroscopic analysis
- Step 4–7: High-speed CNC carving, vacuum heat treatment & CMM dimensional check
- Step 8–10: Prussian-blue parting line fitting, in-house parison blowing test & sample dispatch
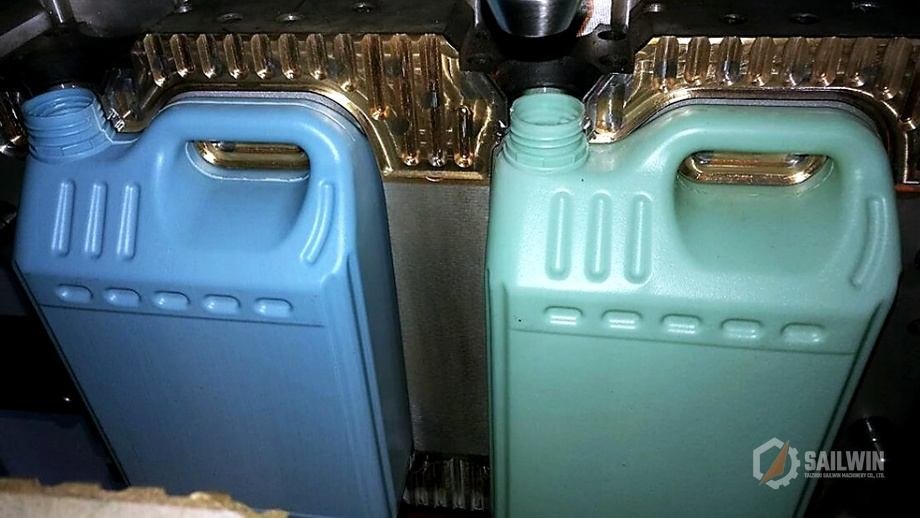 IN-MOLD DEFLASHING
In-Mold Automatic Deflashing & Hydraulic Slide Cores
Labor costs for manual deflashing are unsustainable. Our EBM molds feature integrated pneumatic or mechanical deflashing punches that automatically shear neck, handle, and tail flash inside the machine.
- Automated Trim: Clean 100% automated trimming of neck dome, handle slug, and bottom tail
- Hollow Handle: Hydraulic core-pulling slides create seamless ergonomic grip holes
- Downstream Ready: Finished containers drop directly onto packaging conveyors without manual touch
Hardened Tool Steels & EBM Machine Platen Interfaces
Extrusion blow molds experience violent parison shear and constant water line pressure. We utilize pre-hardened P20, 718H, and stainless S136 with customized machine tie-bar clearances.
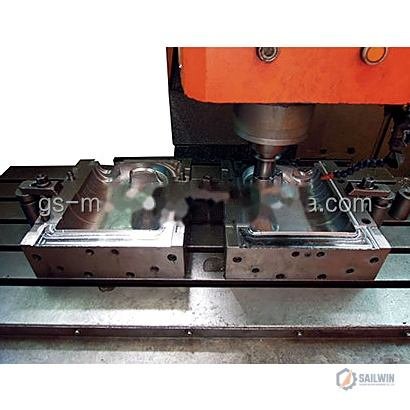 HIGH-GRADE MOLD STEEL
Pre-Hardened P20 & 718H Steel Cavities
Machined from forged billets vacuum-hardened to HRC 32–36. Eliminates internal stress deformation and maintains micron-level parting line parallelism across extreme continuous production cycles.
- Core Hardness: HRC 32–36 uniform hardness throughout the block
- Polishing Grade: Sandblasted texture or SPI A2 gloss finish
- Wear Plates: Bronze self-lubricating wear strips along moving slides
- Lifespan: Guaranteed 5,000,000+ continuous blow cycles
 PLUG-AND-PLAY PLATEN
Custom Machine Platen & Tie-Bar Matching
Designed to fit your specific extrusion blow molding machine platen pattern: Bekum, Kautex, Uniloy, Automa, Techne, and Chinese shuttle machines. Supplied with calibrated T-slot mounting patterns.
- Mounting Standards: Standard T-slots, locating ring centers, and crane eyebolts
- Blow Pin Calibration: Top and bottom calibration blow pin cutting sleeves
- Hydraulics: Quick-disconnect hydraulic couplers for sliding core cylinders
- Compatibility: 100% plug-and-play installation without field modifications
In-House EBM Tooling Workshop & Machine Trial Testing
Precision extrusion blow molds require massive structural stability and flawless hydraulic synchronization. Tour our specialized heavy tooling and testing bays.
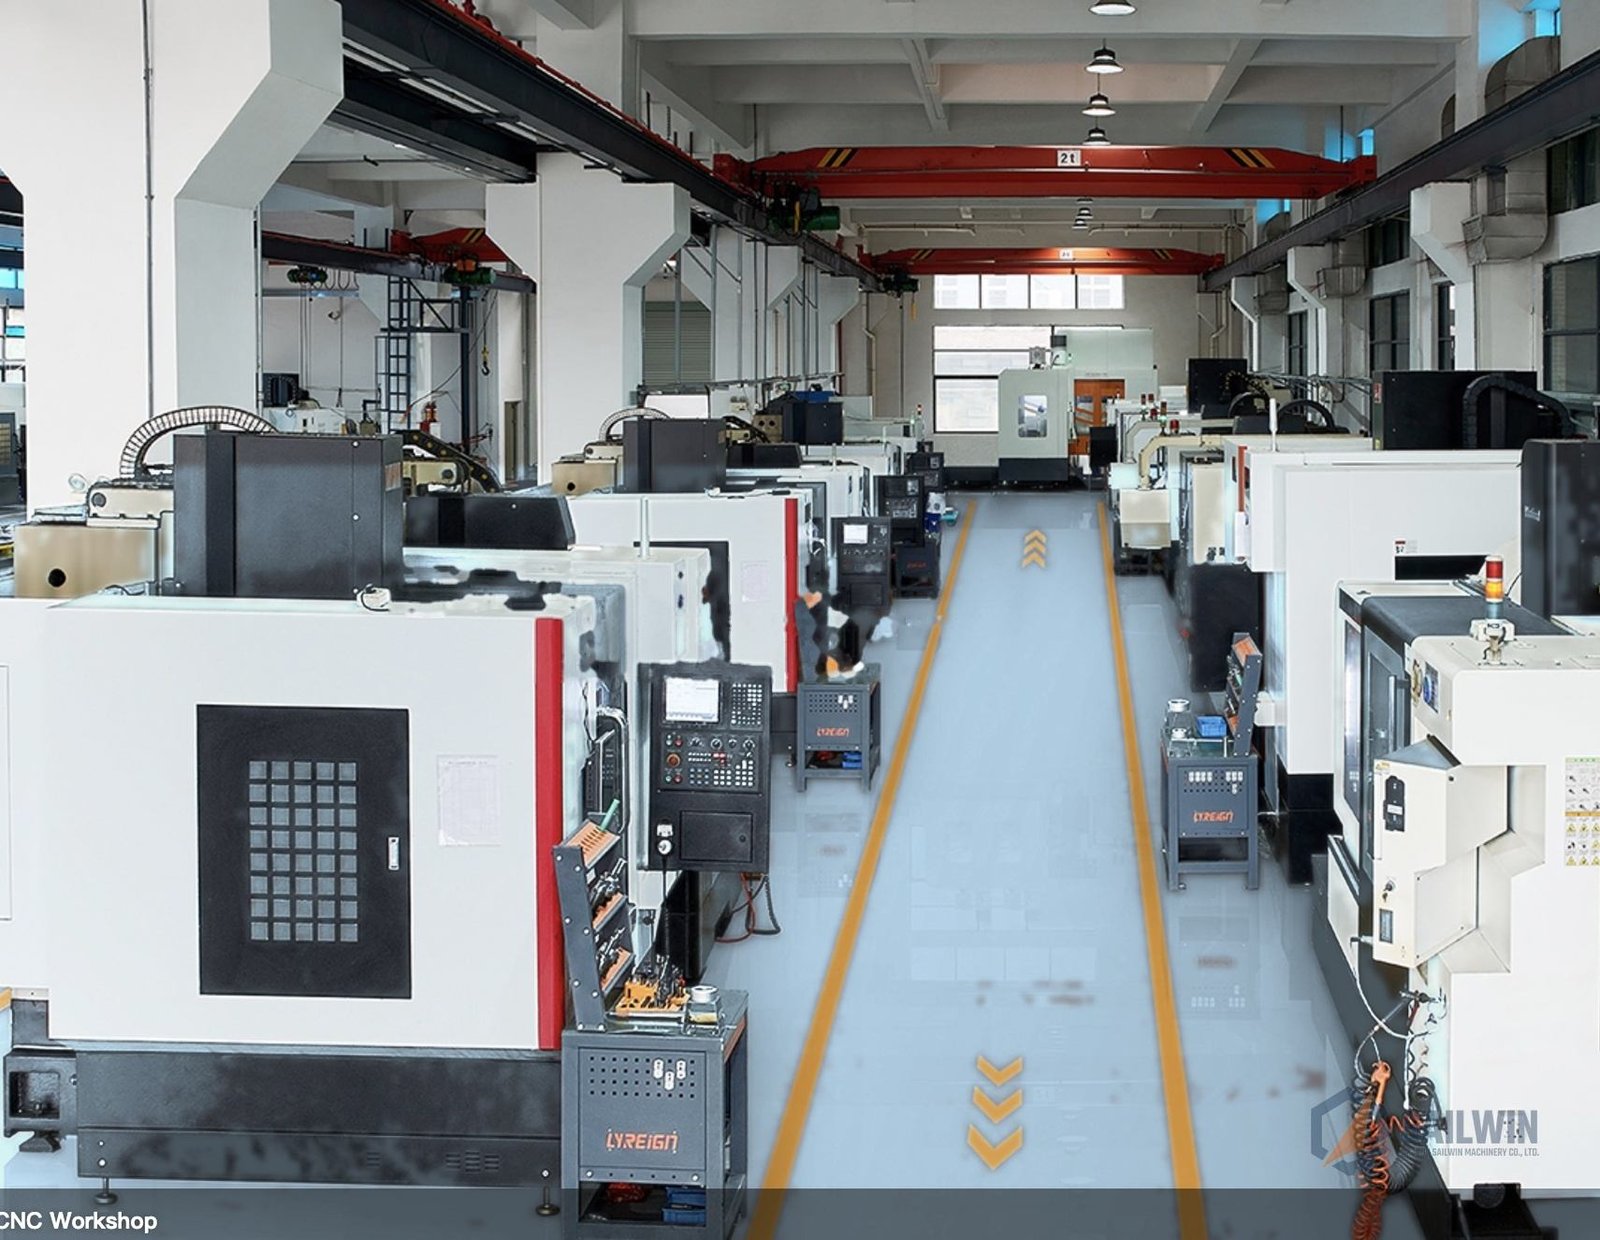
Heavy-Duty EBM CNC Tooling Centers
Large-scale gantry CNC milling machines dedicated to deep cavity roughing and finishing of high-tonnage jerry can and chemical drum mold blocks.
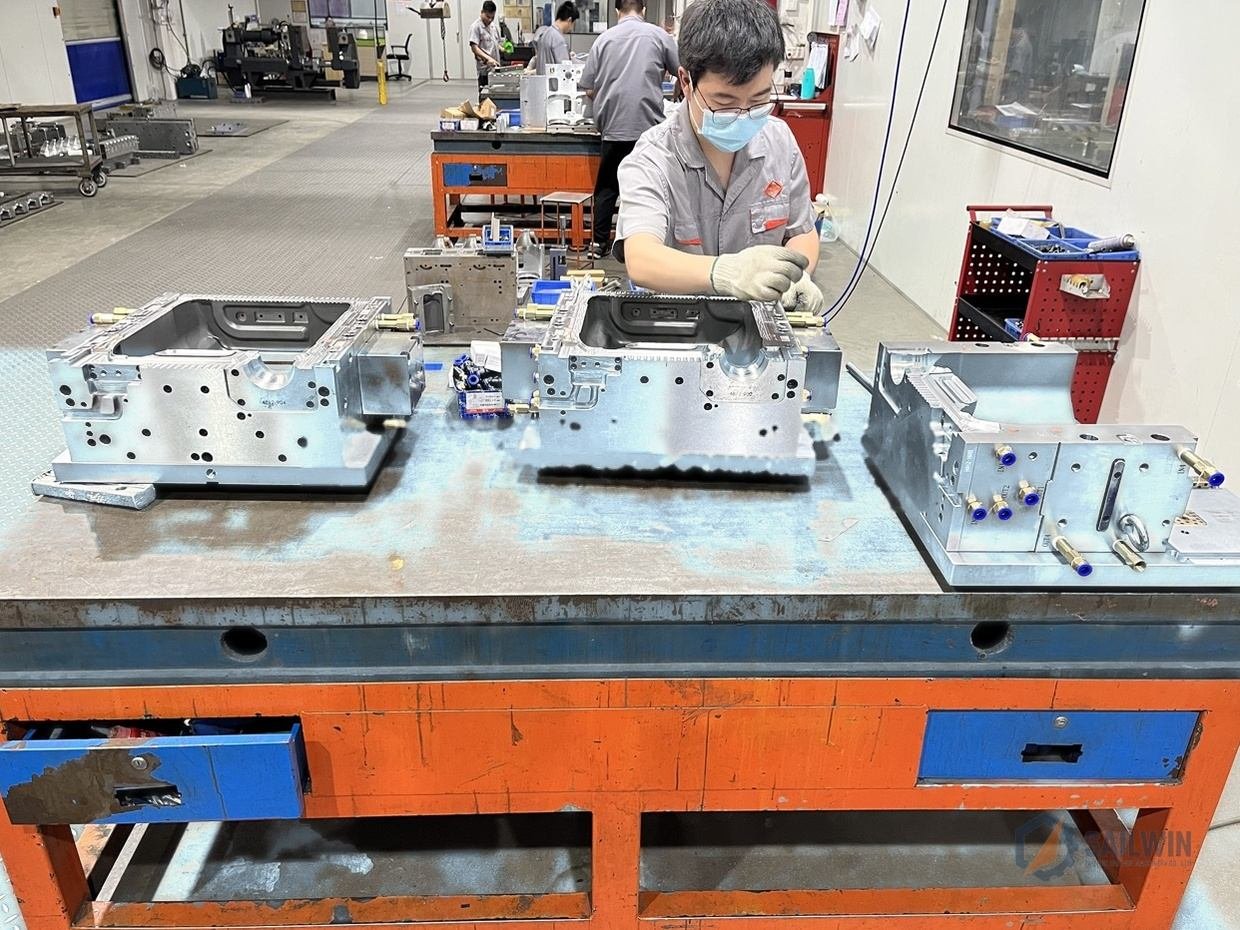
Master Tooling Bench-Fitting Specialists
Experienced mold craftsmen hand-fitting beryllium copper inserts, calibrating parting line pinch-off blade clearances, and verifying hydraulic core-puller stroke.
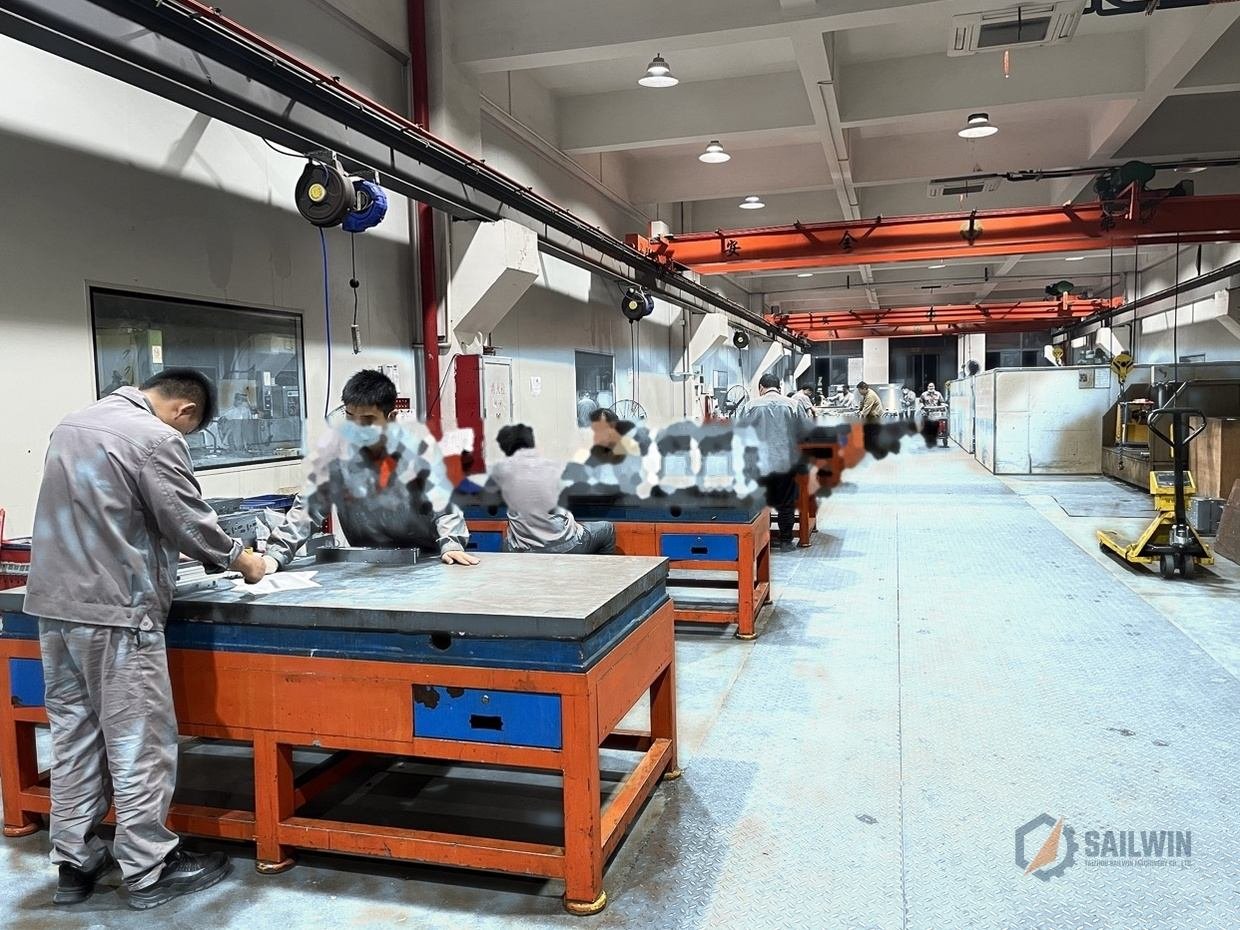
Crane-Equipped Heavy Assembly Bays
Heavy overhead cranes allow safe and smooth positioning of multi-ton accumulator drum molds, master clamping platens, and automated deflashing punch units.
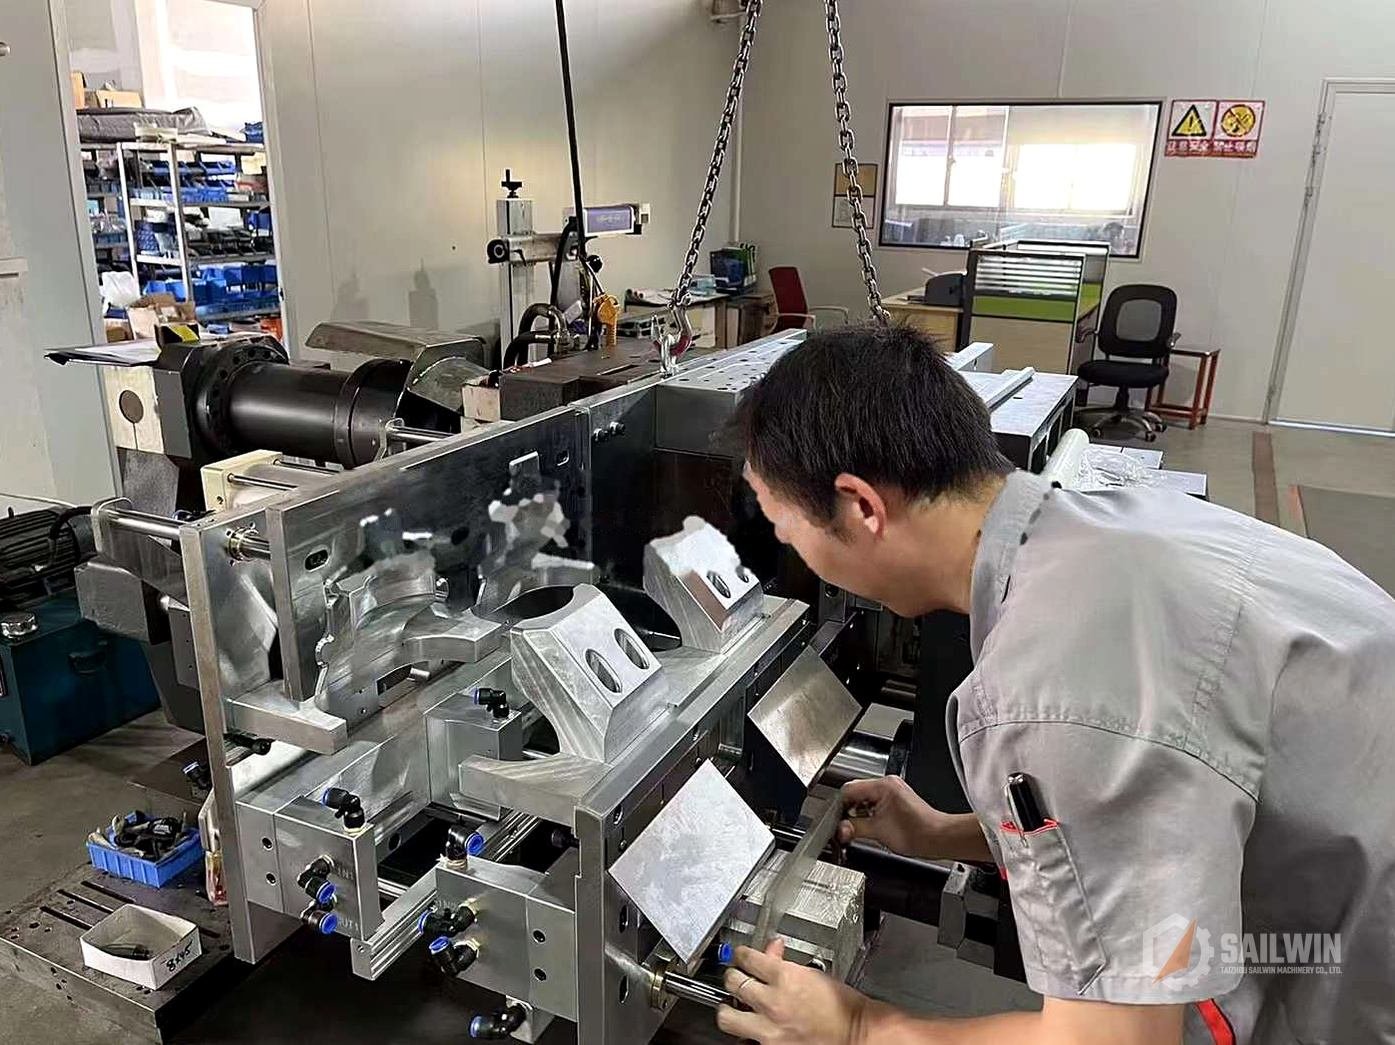
In-House Machine Commissioning & FAT Trials
Our senior field technicians test every EBM mold on our factory extrusion blow molding machines, fine-tuning parison drop synchronization and cooling times.
HDPE/PP Packaging Gallery & Cross-Tooling Navigation
Covering agrochemical jugs, automotive fluid bottles, industrial drums, and consumer packaging. Explore our comprehensive portfolio and detailed sub-pages.
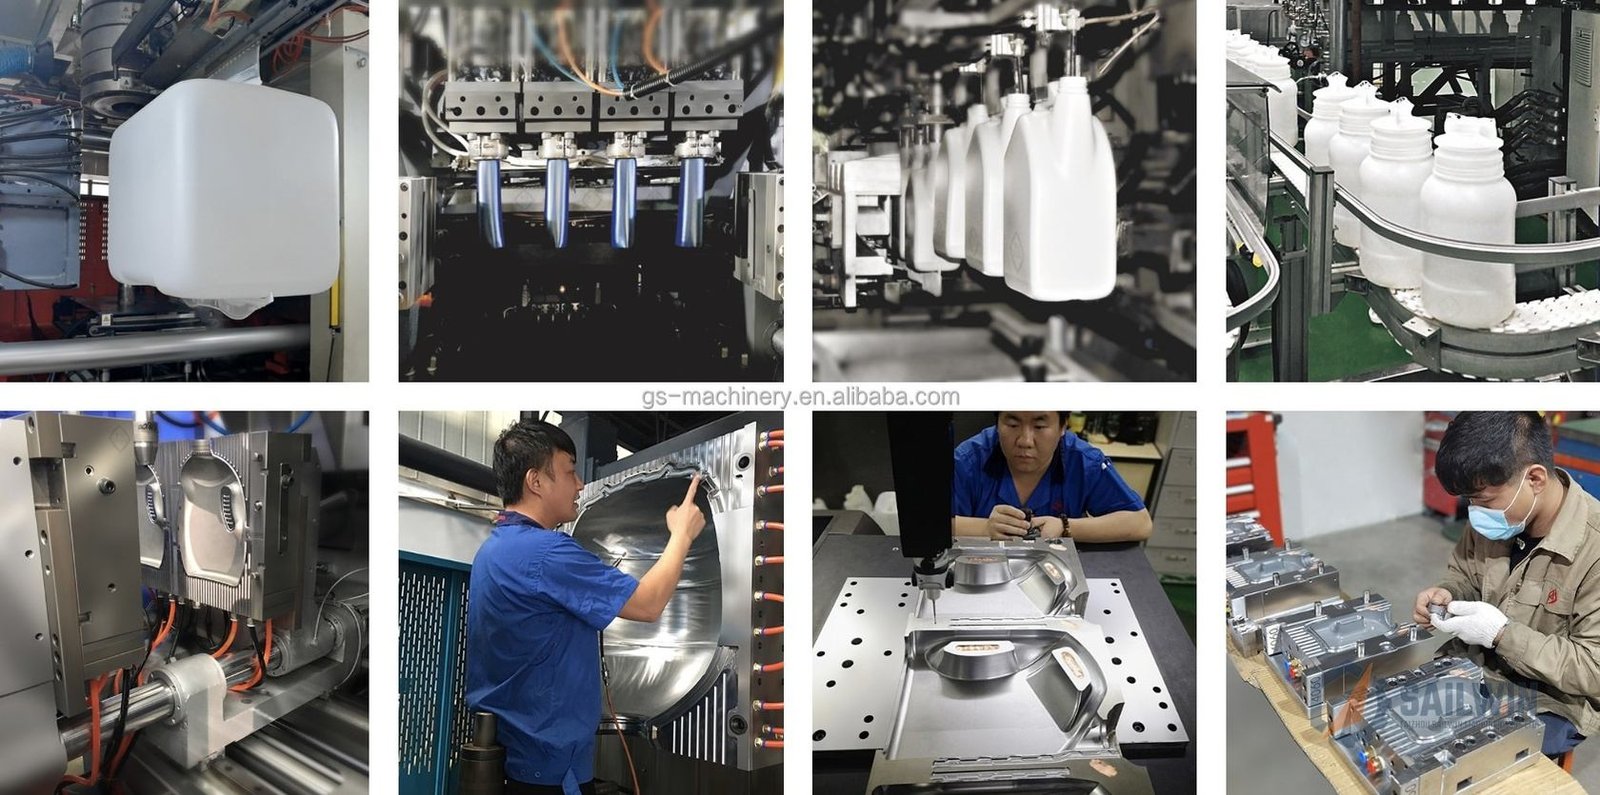
Turnkey Tooling for Industrial Hollow Parts
From multi-layer EVOH barrier agrochemical bottles with anti-permeation seals to heavy 200L L-ring drums passing strict UN drop and stacking regulations. Sailwin delivers calibrated parison wall thickness and clean in-mold deflashing shears.
Explore Specific EBM & Tooling Sub-Pages
View PET Blow Molds →Jerry Can & Chemical Drum Molds
1L to 30L stackable chemical jerry can tooling with golden beryllium copper pinch-offs and hydraulic core-pulling handles.
Lube Oil & Detergent Bottle Molds
High-efficiency multi-cavity tooling for motor oil bottles, laundry detergents, and shampoo packs with transparent view-stripes.
200L L-Ring Drums & Large Tanks
Heavy accumulator head tooling for 200L double-tight head chemical drums and IBC tank containers passing strict UN drop tests.
PET Bottle Stretch Blow Molds
Explore high-speed linear and rotary stretch blow molds (1–16 cavities) for mineral water, beverage bottles, and food jars.

