Heavy-Duty 200L L-Ring Chemical Drum Mold & Large Tank Tooling
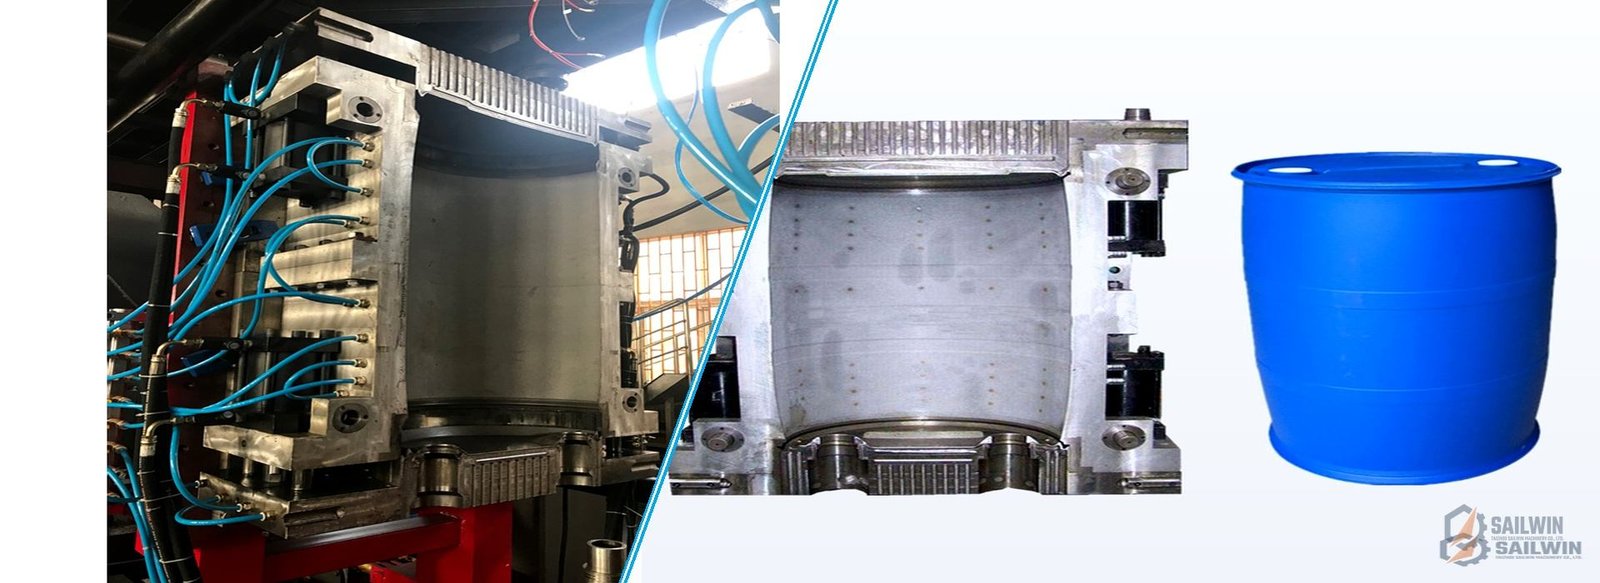
Specialized blow mold tooling engineering for 200L/220L tight-head double L-ring chemical barrels, open-top drums, and 1,000L IBC tank containers. Engineered for accumulator-head extrusion blow molding machinery with pre-hardened forged P20/718H steel, high-flow spiral cooling channels, and 150-to-300-ton hydraulic clamp rigidity to pass UN dangerous goods stacking and drop certification.
200L L-Ring HDPE Chemical Drum Mold Parameters
High-tonnage accumulator head extrusion blow molds engineered for 200L/220L tight-head chemical barrels and 1,000L IBC tank liners. Compliant with UN hazardous cargo packing groups I, II, and III.
| Technical Specification | Standard Parameter Range | Engineering Benefit for Chemical Packagers |
|---|---|---|
| Drum Volume Standards | 200L / 220L (55 Gallon), 120L, 1000L IBC | Full standard coverage for global chemical transit, bulk liquid storage, and maritime transport |
| Chime Ring Architecture | Single L-Ring & Double L-Ring Profiles | Upper and lower chime rings designed for universal parrot-beak forklift drum clamps |
| Bung Opening Standards | Dual 2-inch Top Bungs: G2 & S56x4 Buttress | Interchangeable threaded neck split inserts; compatible with Tri-Sure and standard plugs |
| Heavy Parison Shot Weight | 8.5 kg to 10.5 kg (High-Density Parison) | Optimized wall thickness programming transitions prevent corner thinning and bottom sag |
| Hydraulic Clamping Rigidity | 150 to 300 Tons Machine Clamping Force | Massive structural P20 steel frames eliminate mold breathing under accumulator shot surge |
| High-Flow Cooling Circuits | Gun-Drilled Spiral Water Channels (>300 L/min) | Accelerated heat extraction across 8mm thick drum chimes, cutting cycle time to <95 seconds |
| Hydraulic Bottom Lift Cylinder | Stroke >250mm Bottom Core Drop System | Pneumatic/hydraulic synchronized retraction prevents bottom ring scuffing during ejection |
| UN Dangerous Goods Cert | Certified for 1.8m Drop & 300 kPa Pressure | Zero weld seam rupture under 3-tier stacking loads and extreme sub-zero drop impacts |
| Total Mold Net Weight | 4,500 kg to 8,500 kg Solid Construction | Heavy structural plate frames with integrated lifting trunnions for safe crane handling |
| Guaranteed Mold Life | 5,000,000+ Continuous Cycles | Pre-hardened tool steel P20 / 718H with bronze wear gibs and replaceable pinch-off lands |
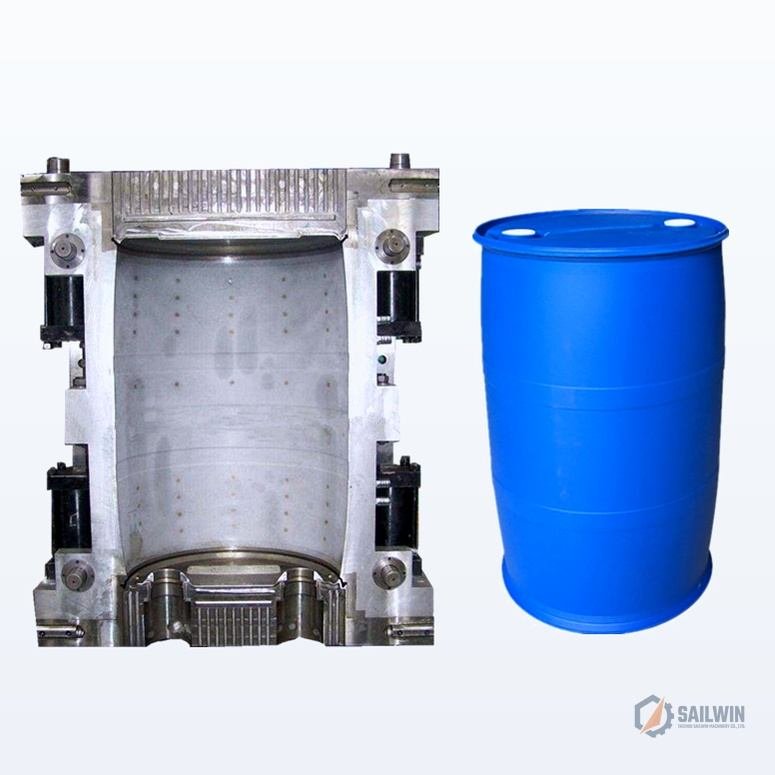 200L TIGHT HEAD · SINGLE L-RING
200L Tight-Head Single L-Ring Drum Mold
Engineered for standard 200L chemical and petrochemical drums. Features upper chime L-ring profile and dual 2-inch bung plugs for universal handling.
- Volume: 200 Liter / 55 US Gallons
- Weight: 8.5kg – 9.5kg Standard Drum
- Chime: Reinforced single L-ring profile
- UN Testing: Passed 1.8m water drop impact
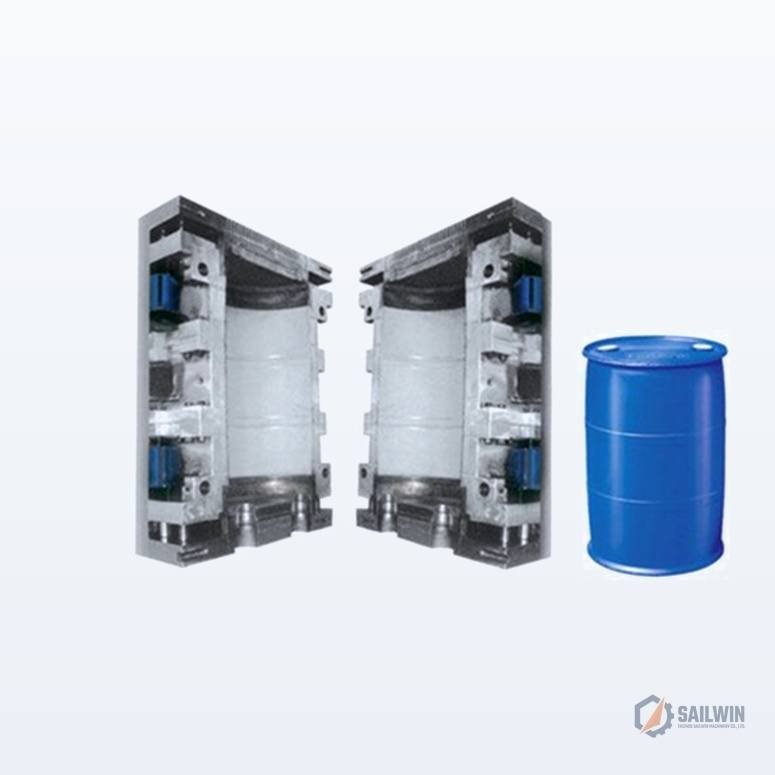 DOUBLE L-RING · DUAL CHIME
Double L-Ring Heavy Chemical Drum Mold
Top and bottom L-ring chime architecture engineered for automated rolling conveyors and double parrot-beak forklift clamps. Extreme stacking rigidity.
- Volume: 220 Liter Heavy Chemical Drum
- Weight: 9.5kg – 10.5kg Heavy Duty
- Chimes: Top and bottom dual L-rings
- Stacking: 3-tier full pallet warehouse stacking
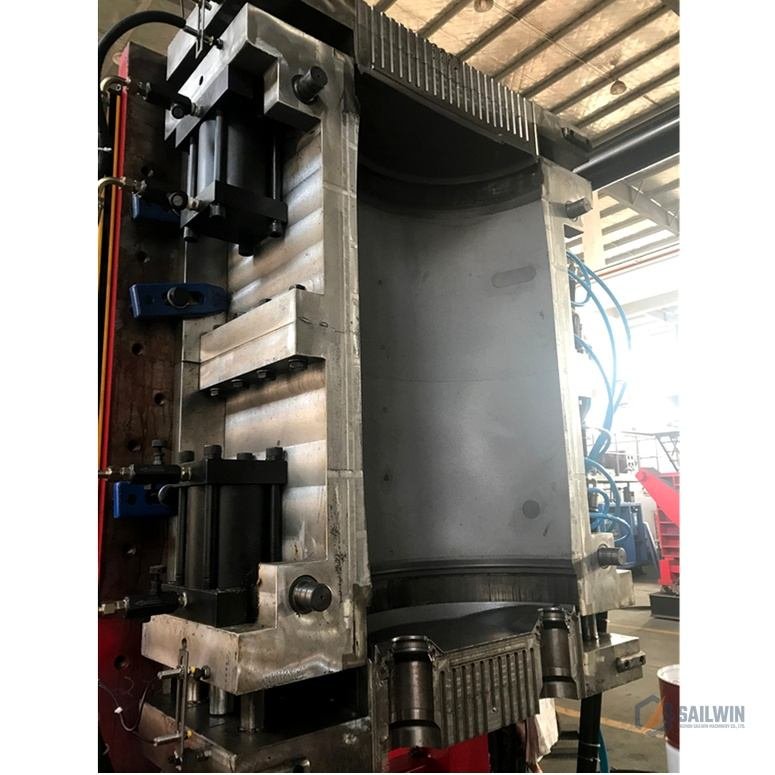 HYDRAULIC SYNCHRONIZATION
Accumulator-Head Drum Mold with Hydraulics
Equipped with heavy hydraulic bottom-mold retraction cylinders and side parting interlocks. Built for 50L–150L accumulator extrusion blow molders.
- Machine Interface: Kautex, Bekum, Jomar & Chinese accumulator EBM
- Bottom Cylinder: Integrated hydraulic bottom drop stroke
- Cooling: High-pressure deep gun-drilled channels
- Weight: 6,800kg Total Assembly Weight
Specialized 200L Drum Tooling: L-Ring & Accumulator Head
A 10kg parison shot delivered in seconds generates intense thermal and mechanical clamping dynamics. Explore our three fundamental 200L drum engineering breakthroughs.
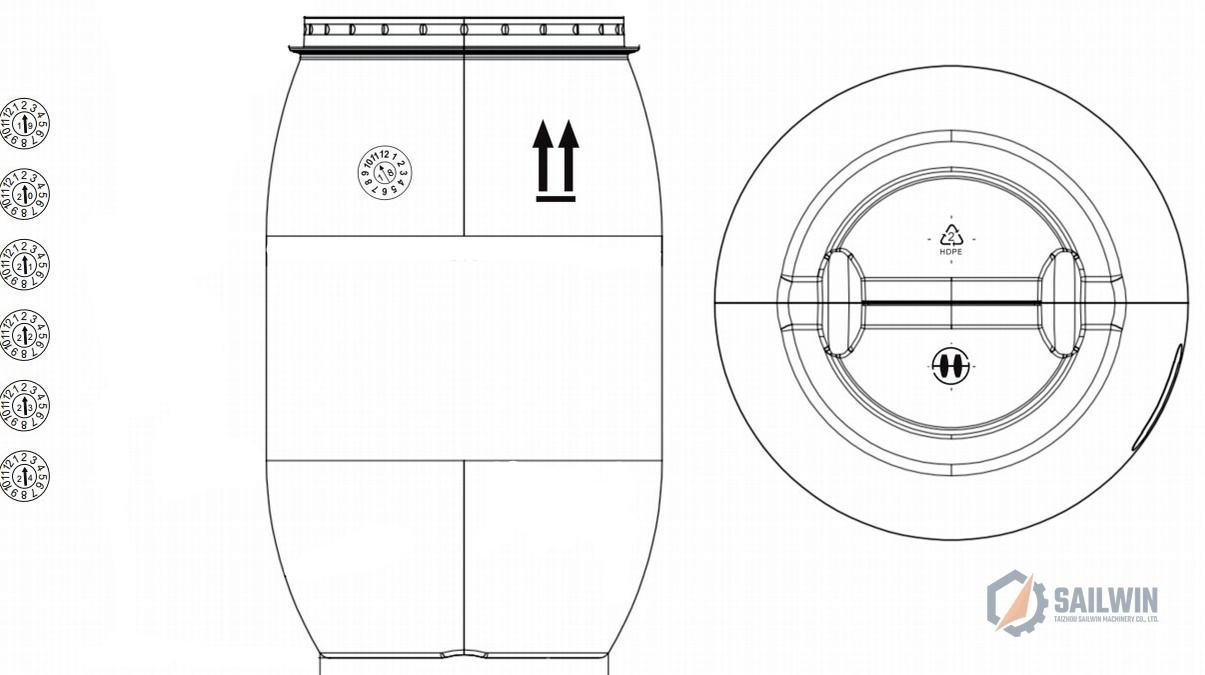 CAD SPECIFICATIONS
Parametric CAD Engineering & Parison Wall Control
Large 200L drums require calibrated wall thickness transitions. Our 3D CAD design balances axial parison elongation with radial stretch expansion, placing structural resin precisely into the top chime L-ring and bottom chime.
- Chime Thickness: Reinforced 8mm chime ring wall resists violent 1.8m diagonal drops
- Body Ribs: Rolling hoop geometry provides structural stiffness under 3-tier stacking
- Volumetric Tolerance: 200L capacity variance held strictly within ±0.5% (±1.0 Liter)
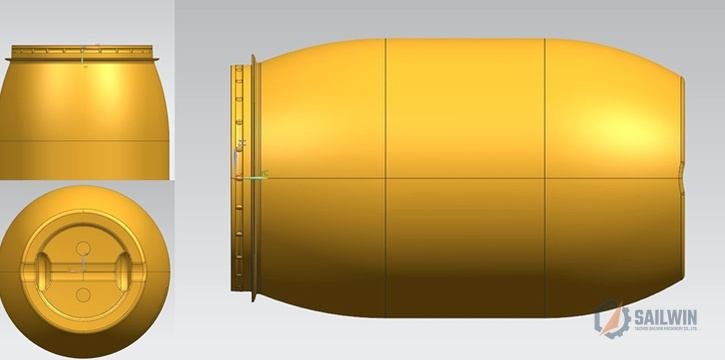 3D DIGITAL SURFACE
Double L-Ring Chime Geometry & FEA Stress Modeling
The top L-ring chime is the critical interface for universal forklift parrot-beak clamps and automated roll handling. Our 3D finite element stress simulations eliminate weak stress-concentration notches.
- Parrot-Beak Grip: Standardized ISO chime profile compatible with all international drum lifters
- Hydraulic Bung Plugs: Dual 2-inch top bungs (G2 fine & S56x4 coarse buttress threads)
- UN Drop Certification: Certified for 1.8-meter liquid drop impact at -18°C temperature
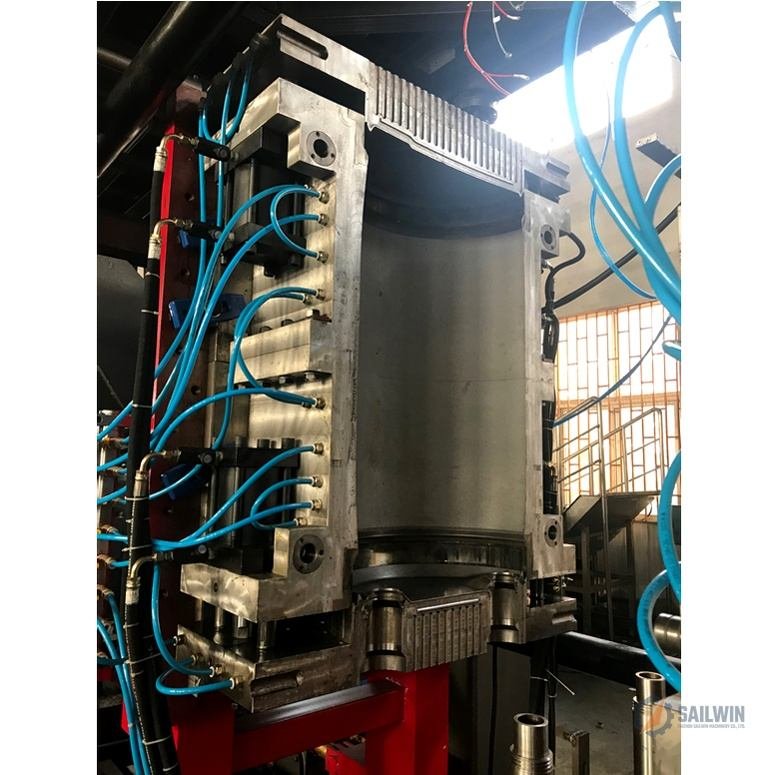 MACHINE PLATEN MOUNTING
High-Tonnage Machine Platen & Deep-Bore Cooling
Mounting an 8-ton mold block onto 150–300 ton accumulator blow molders requires rigid guide columns and high-velocity cooling water manifolds to maintain fast cycle times.
- Deep Gun-Drilling: Spiral cross-drilled cooling channels achieve >300 L/min flow rate
- Zero Mold Breathing: Pre-hardened P20 frame eliminates parting line flash under shot surge
- Bottom Cylinder: Integrated hydraulic cylinder drops bottom mold smoothly during ejection
Pre-Hardened P20 Steel & Hydraulic Drop Core System
Continuous parison clamping under 300 tons of hydraulic locking force requires massive structural steel integrity. Tour our specialized accumulator tooling features.
HYDRAULIC CORE DROPSynchronized Hydraulic Bottom Ejector System
Equipped with heavy hydraulic bottom-core cylinders mounted directly onto the mold base. Drops the bottom mold chime downward before mold opening, eliminating chime scuffing.
- Hydraulic Stroke: >250mm long-travel bottom core drop system
- Chime Protection: Completely prevents parting line shear during container demolding
- Hydraulic Rating: High-pressure hydraulic hoses with quick-disconnect couplers
- Cycle Time: Fast synchronized movement keeps total dry cycle under 15 seconds
FORGED TOOL STEEL BLOCKSPre-Hardened P20 & 718H Structural Cavities
Milled from monolithic vacuum-degassed forged blocks. Hardened to HRC 32–36 to withstand continuous 300-ton machine platen clamping loads without cavity distortion.
- Block Weight: Heavy structural alloy blocks weighing up to 8,500kg
- Gun-Drilled Water: Spiral high-flow water cooling channels drill through thick wall sections
- Wear Plates: Self-lubricating bronze wear strips along heavy sliding guide gibs
- Lifespan: Guaranteed 5,000,000+ continuous production cycles
Machine Clamping Rigidity & Factory Trial Testing
Mounting an 8-ton mold block onto accumulator extrusion machinery requires precision platen parallelism and complete pre-dispatch dry-cycle verification.
200L Heavy-Duty Machine Platen Assembly
Rigid mounting backplates engineered to match the tie-bar spacing and T-slot clamping patterns of large Kautex, Bekum, and Chinese accumulator extrusion blow molders.
In-House Trial Blown Sample Verification
Every 200L mold is mounted on our in-house accumulator blow molding test machine to blow 10–20 actual HDPE blue barrels, confirming zero parting line flash and uniform chime thickness.
UN Hazardous 200L Packaging & Cross-Tooling Navigation
Tested in demanding industrial chemical and petrochemical packaging facilities worldwide. Explore our proven 200L drum portfolio and related tooling sub-pages.
Zero-Leak Chimes & High Stacking Load Capacity
Hazardous liquid chemical barrels require 100% chime ring integrity and sturdy rolling hoops that withstand 3-meter stacking loads and 1.8-meter sub-zero drop tests. Our molds deliver optimized parison wall transitions and high-flow gun-drilled cooling channels that eliminate thick chime cooling bottlenecks.
Explore Related EBM & Tooling Sub-Pages
View All EBM Molds →Jerry Can & Chemical Drum Molds
1L to 30L stackable chemical jerry can tooling with golden beryllium copper pinch-offs and hydraulic core-pulling handles.
Motor Oil & Detergent Bottle Molds
High-efficiency multi-cavity tooling for engine oil bottles, laundry detergents, and shampoo packs with transparent view-stripes.
2-Inch Bung Plug & Flange Molds
High-precision multi-cavity injection molds for 2-inch G2 and S56x4 buttress bung plugs with EPDM sealing gaskets.
Complete Extrusion Blow Molds Series
Explore all continuous and accumulator head EBM mold configurations, C17200 beryllium copper pinch-offs, and machine adapters.

