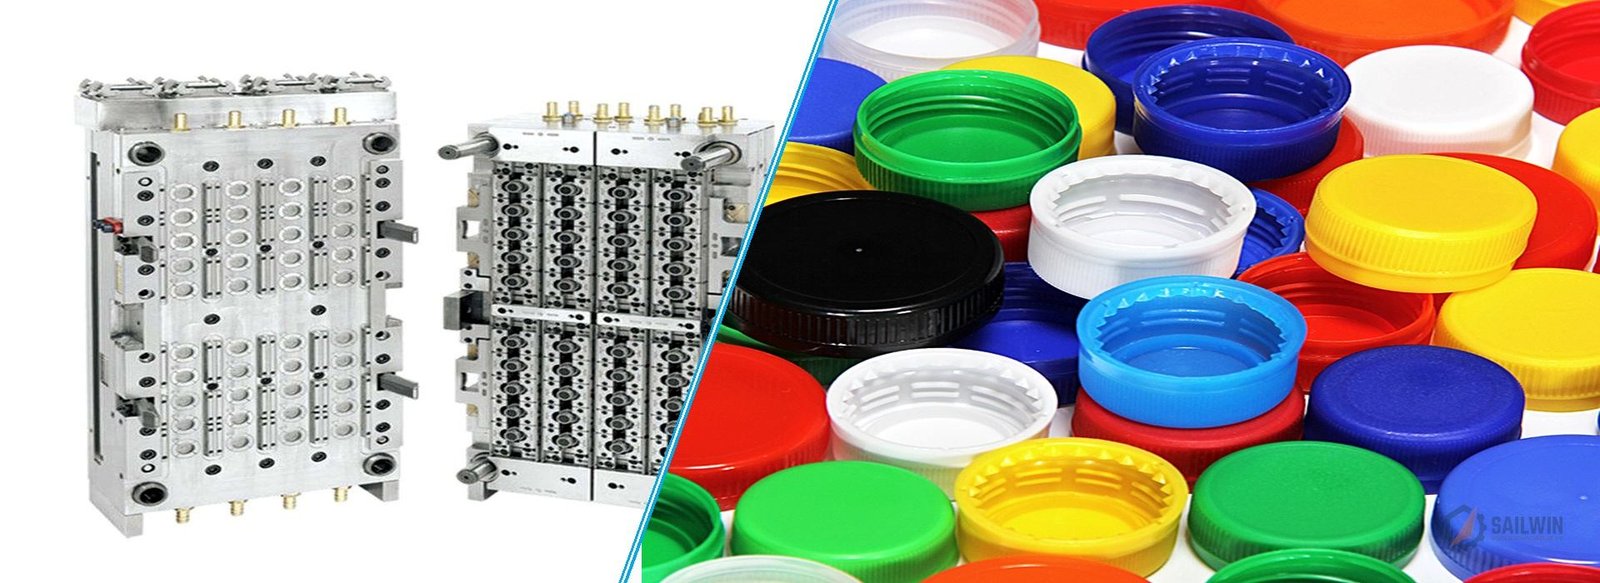
High-Speed Mineral Water Bottle Cap Mold Solutions
Engineered for high-volume still mineral water and carbonated beverage bottlers. Sailwin precision bottle cap molds feature imported Swedish ASSAB S136 stainless steel, high-conductivity beryllium copper conformal cooling tips, and balanced European valve-gate hot runners, delivering an industry-leading sub-3.8s fast cycle time and flawless tamper-evident band folding.
High-Speed Bottle Cap Mold Matrix (16 to 72 Cavity)
Engineered for 29/25, 30/25, and PCO 1881 standard water and beverage closures. Explore our high-cavity tooling platforms featuring sub-3.8s cycles, beryllium copper cooling inserts, and air-assisted stripper plate ejection.
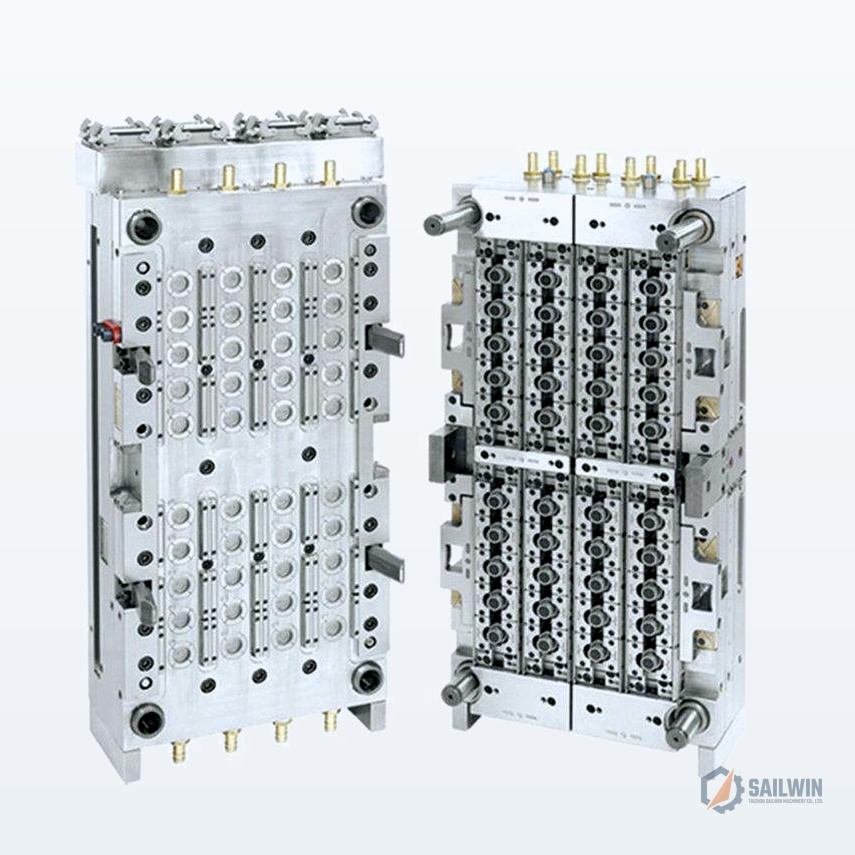 48 CAVITIES · ULTRA-FAST
48-Cavity High-Speed Water Cap Molds
The benchmark production tool for commercial mineral water plants running 36,000–45,000 caps per hour with automated take-out.
- Cap Standards: 29/25 Ultralight (0.95g–1.15g), 30/25 Still Water
- Cycle Time: 3.5s – 4.2s (with chiller ≤ 10°C)
- Gate System: Direct pinpoint hot tip valve gate
- Lifespan: 5,000,000+ shots with S136 cavity & core inserts
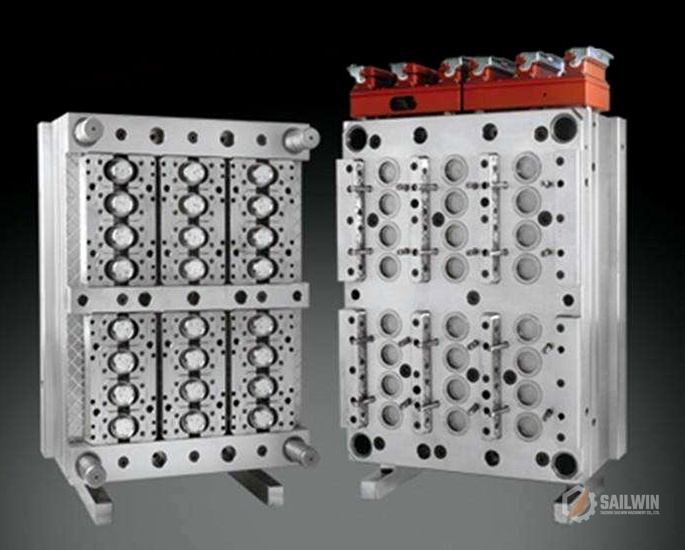 32 CAVITIES · BALANCED
32-Cavity Balanced Hot Runner Molds
Versatile high-output tooling for PCO 1881 CSD carbonated beverage and still water closures running on 160T–220T presses.
- Cap Standards: PCO 1881 (1.85g–2.15g) with gas-tight seal lip
- Cycle Time: 3.8s – 4.5s
- Hot Runner: Naturally balanced manifold with no dead corners
- Ejection: Stripper plate assisted by central pneumatic blow
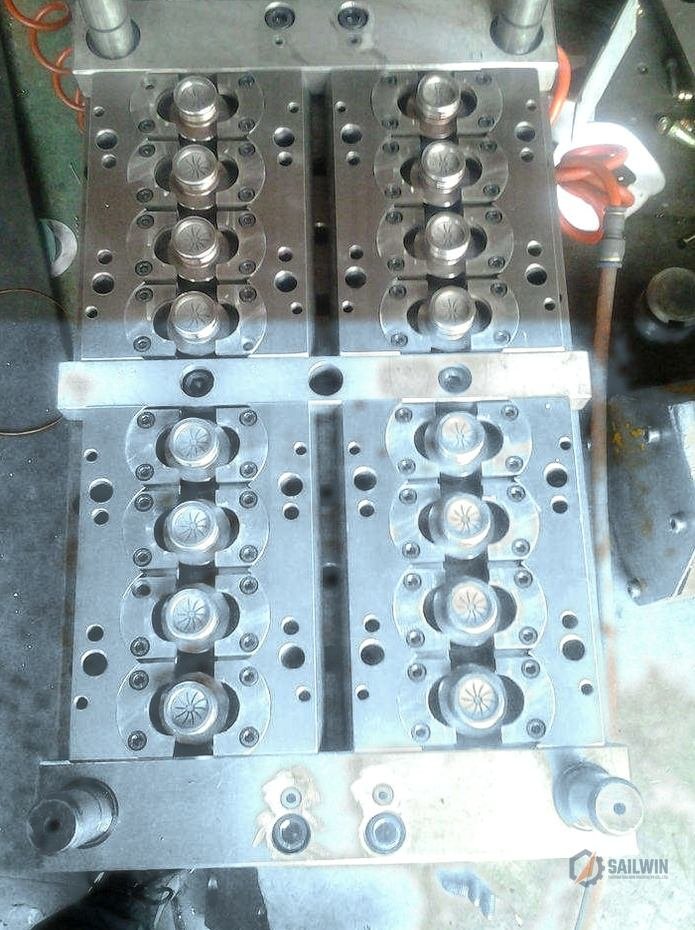 16 CAVITIES · COMPACT
16-Cavity Compact Water Cap Molds
Engineered for regional beverage facilities and smaller bottling operations running on standard 100T–150T servo injection presses.
- Cap Standards: 28mm PCO 1810 / 1881 / 30/25 Water
- Cycle Time: 4.5s – 5.5s
- Features: Quick-connect cooling manifolds on tool base
- Footprint: Compact mold base fits standard platen spacing
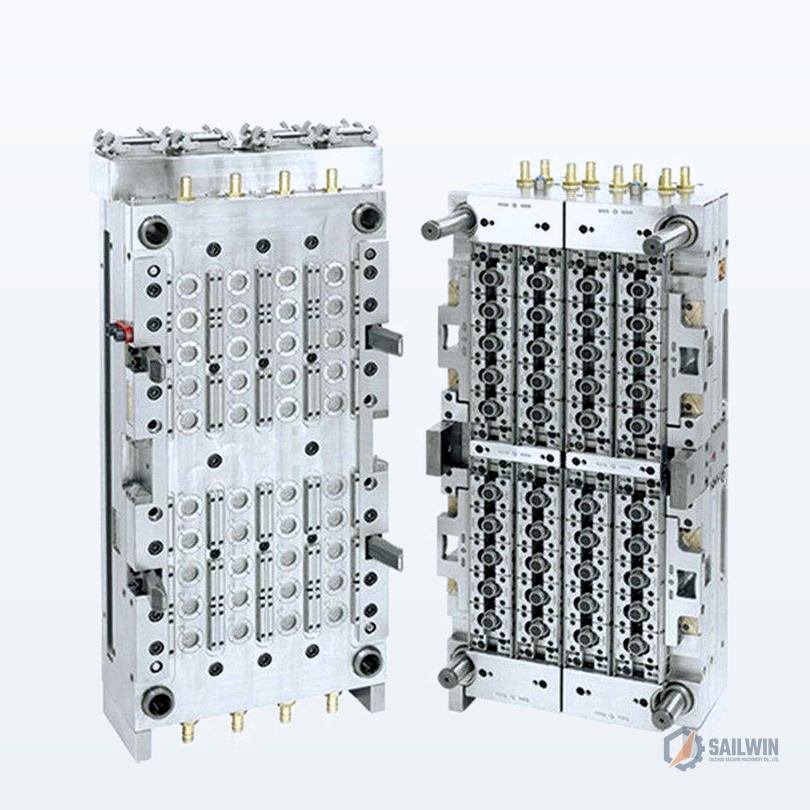 BERYLLIUM COPPER · SUB-3.5S
Dual-Plate Beryllium Copper Cap Molds
Equipped with Japanese Daido C17200 beryllium copper core inserts offering 400% higher thermal conductivity than standard tool steel.
- Cooling Tech: CuBe insert direct core contact chilling
- Cycle Time: Sub-3.5s for 1.0g lightweight closures
- Plates: Precision ground dual guide pin strippers
- Benefit: Zero thermal shrinkage ovality or thread binding
| Cavity Count | Target Cap Standard | Cap Weight Range | Cycle Time (s) | Rec. Machine Tonnage | Hourly Output (pcs) | Annual Output (8000h) | Action |
|---|---|---|---|---|---|---|---|
| 16 Cavities | PCO 1881 / 29/25 Water | 1.0g – 2.2g | 4.5s – 5.5s | 100T – 140T | 11,000 – 12,800 | 95 Million pcs | |
| 24 Cavities | 29/25 / 30/25 Still Water | 0.95g – 1.8g | 4.0s – 4.8s | 140T – 180T | 18,000 – 21,600 | 160 Million pcs | |
| 32 Cavities | PCO 1881 CSD & Still Water | 1.1g – 2.1g | 3.8s – 4.5s | 180T – 240T | 25,600 – 30,300 | 225 Million pcs | |
| 48 Cavities | Ultra-Light 29/25 Water Caps | 0.88g – 1.35g | 3.5s – 4.0s | 240T – 320T | 43,200 – 49,300 | 370 Million pcs | |
| 72 Cavities | 29/25 & 1881 High-Speed Bottling | 0.88g – 1.85g | 3.2s – 3.8s | 320T – 450T | 68,200 – 81,000 | 580 Million pcs |
Need Downstream Rotary Cap Slitting & Folding Automation?
Sailwin supplies integrated high-speed tamper-evident band slitting and folding machines running at up to 40,000 caps/hour.
Precision Closure Engineering: Tamper Band & Fast Ejection
Bottle closures operate in extreme high-volume environments where 0.1 second of cycle time or 0.02mm of thread shrinkage ovality determines plant profitability. Explore our specialized engineering disciplines.
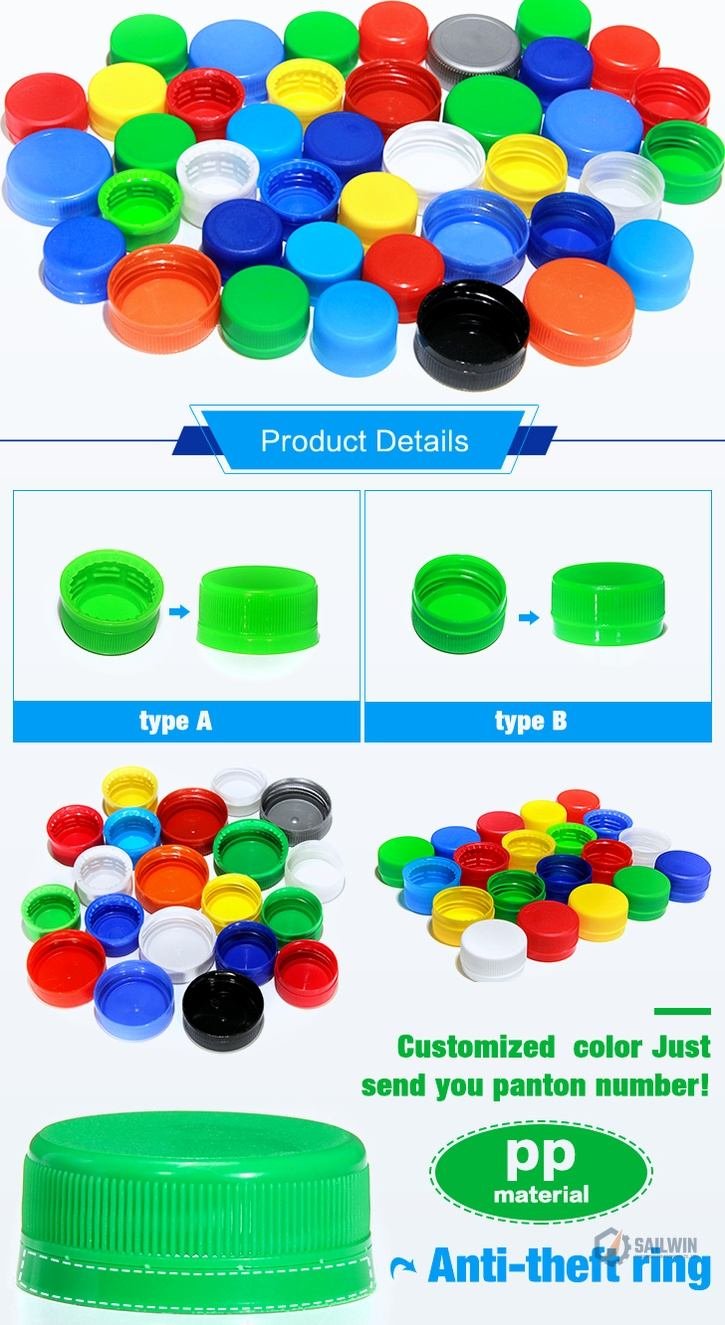 CLOSURE CAD BLUEPRINT
Type A & Type B 28mm Cap & Anti-Theft Ring Specs
Our precision tooling supports both global standards: Type A (integral in-mold mechanical folded retaining band) and Type B (slitted bridge retaining ring for downstream rotary folding). Each profile is engineered for consistent 0.8–1.6 N·m bridge-break torque.
- • Gas-Tight Bore Seal: Double seal plug lip guarantees zero carbonation leakage under 6–10 Bar internal pressure.
- • Tamper Bridge Integrity: Symmetrical 8 to 12 micro-bridge connectors break cleanly without shedding plastic debris into beverage bottles.
- • High-Speed Capping Fit: Knurling outer ribs engineered to prevent chuck slippage on 48,000 BPH Krones and Sidel capping turrets.
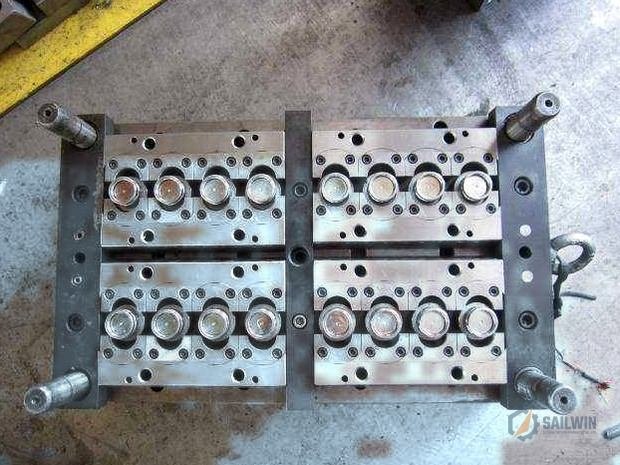 STRIPPER PLATE ASSEMBLY
Precision Ground Stripper Plate & Air-Assist Ejection
Bottle cap threads cannot withstand harsh mechanical pin punch-out without thread deformation. Sailwin incorporates full-contact stripper rings coupled with synchronized central pneumatic poppet valves, gently stripping closures off core threads in <0.3 seconds.
- • Dual Guide Pillars: Hardened guide bushings prevent stripper plate skewing (<0.005mm) across all cavities.
- • Central Air Poppet: High-pressure pneumatic blast breaks internal vacuum during stripper stroke.
- • Free Fall Demolding: Caps drop vertically into collecting chutes without robotic arm delays, maximizing cycle velocity.
BERYLLIUM COPPER COREDaido C17200 Beryllium Copper Core Inserts
HDPE and PP resin shrink non-uniformly if core temperatures fluctuate. Sailwin equips every cap core tip with Japanese Daido C17200 beryllium copper inserts, providing 130 W/m·K thermal conductivity to extract heat directly from the cap top dome and thread roots.
- • Rapid Heat Sinking: Lowers cap plastic demolding temperature by 25°C within 1.8 seconds.
- • Anti-Ovality Guarantee: Uniform cooling prevents cap skirt warping and ovality (diameter roundness within ±0.05mm).
- • Cycle Advantage: Enables sustained sub-3.8s cycles on high-speed servo injection molding presses.
Imported S136 Steel & Heavy Assembly Bays
High-cycle bottle cap tooling operates under continuous 180T–350T clamp pounding and aggressive water condensate. We combine vacuum-quenched stainless steel with overhead crane precision assembly.
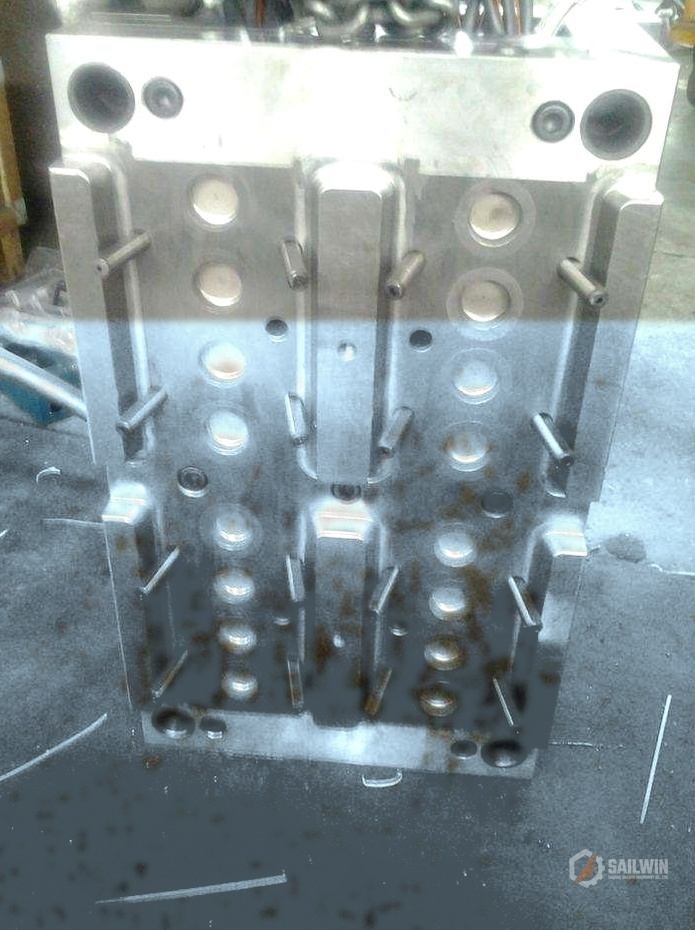
Heavy-Duty Crane Hoisting & Multi-Plate Fitting
Assembled in our heavy tooling hall equipped with dual 15-ton cranes. Veteran master toolmakers hand-fit core plates, runner manifolds, and stripper ejector bushings on granite leveling tables with sub-0.005mm parallel tolerance.
- Plate Parallelism: ≤ 0.012mm across 800mm span
- Assembly Cleanliness: Dedicated cleanroom fitting bays
- Interchangeability: Every core insert numbered and sub-micron matched
ASSAB S136 Stainless Steel
Premium electroslag remelted (ESR) stainless steel vacuum quenched to HRC 50–52. Delivers 100% rust-proof performance against chilled mold sweat and condensation.
- Vacuum Hardness: HRC 50 – 52
- Surface Polish: Ra 0.05 μm Mirror
- Guaranteed Shots: 5,000,000+ Cycles
- Corrosion Proof: 100% Acid & Sweat Resistant
Daido C17200 Beryllium Copper
High-conductivity copper-beryllium alloy embedded directly at cap core tips, pulling heat out of thick closure domes at 130 W/m·K thermal transfer velocity.
- Thermal Transfer: 130 W/m·K (4x of Tool Steel)
- Hardness: HRC 38 – 42 High Wear
- Cycle Reduction: Cuts Cooling by >30%
- Anti-Ovality: Uniform Skirt Solidification
High-Rigidity Mold Base Plates
Stress-relieved structural tool steel normalized against deformation under 350T clamp tonnage. Ground guide pillars with graphite-impregnated bronze bushings.
- Base Hardness: HRC 32 – 36
- Flatness Deviation: ≤ 0.015mm / Meter
- Guide Bushings: Self-Lubricating Bronze
- Deflection Resistance: Zero Plate Bowing
Multi-Color Bottle Closures & Tooling Navigation Hub
Field-tested across millions of commercial bottling runs. Explore our production closure gallery and matching downstream tooling sub-pages.
Production Water & Beverage Closures Gallery
28mm PCO 1881, 29/25, and 30/25 closures engineered for zero leakage and clean tamper break.
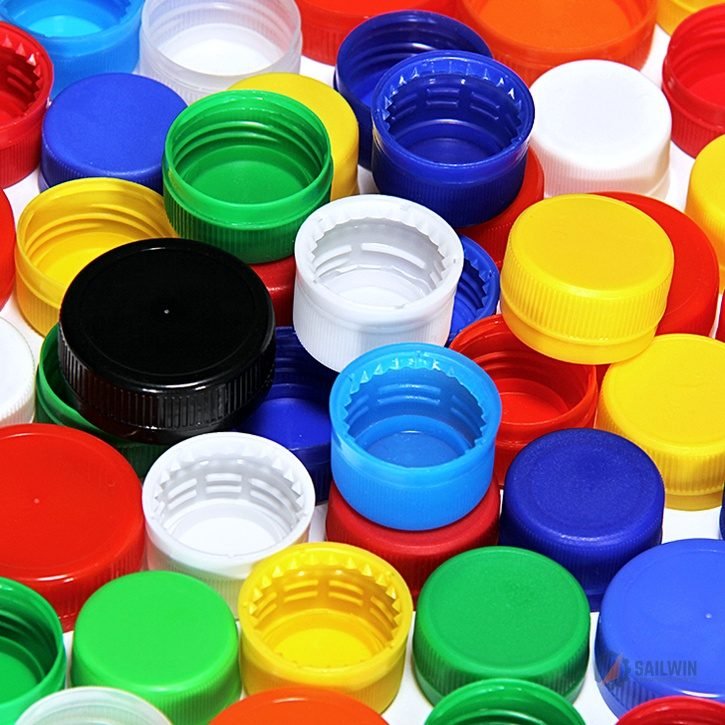
Multi-Color Water Closures with Ring
Molded in vibrant HDPE with internal retention flaps that break cleanly upon opening, giving visual proof of beverage integrity.
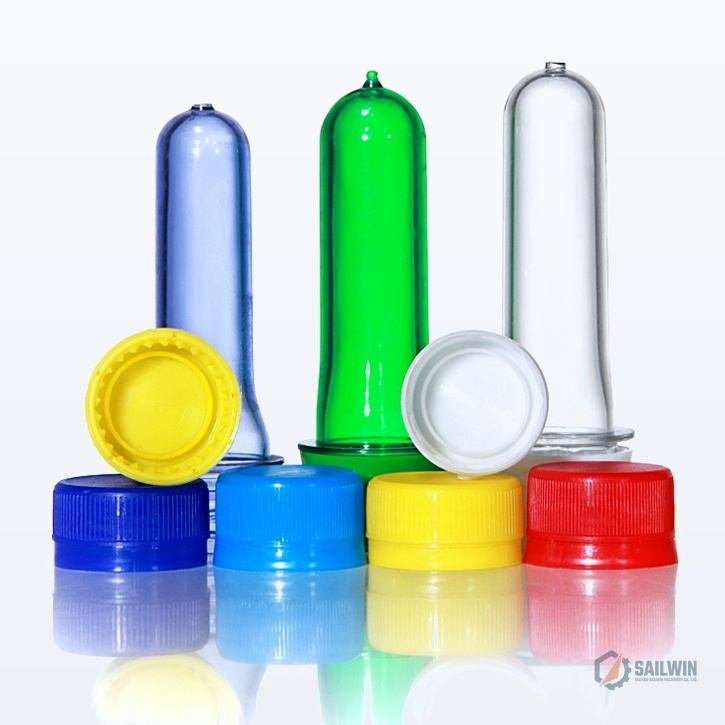
Matching Preforms & 28/30mm Closures
Engineered simultaneously with our PET preform molds, eliminating thread binding, excessive capping torque, or loose seal fitting.
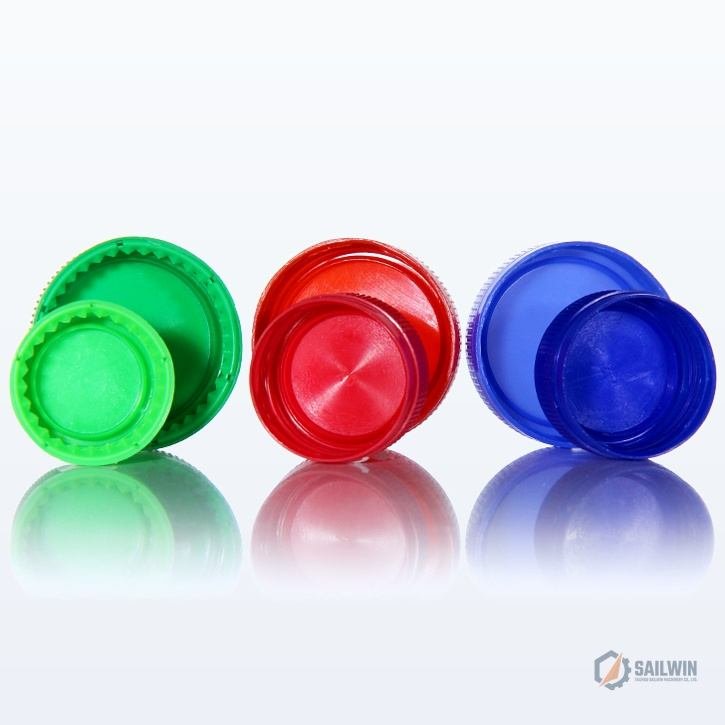
Internal Thread & Double Seal Plug
Wire-EDM thread core contours feature mirror polish, ensuring smooth spin-on engagement and 100% airtight liquid containment.
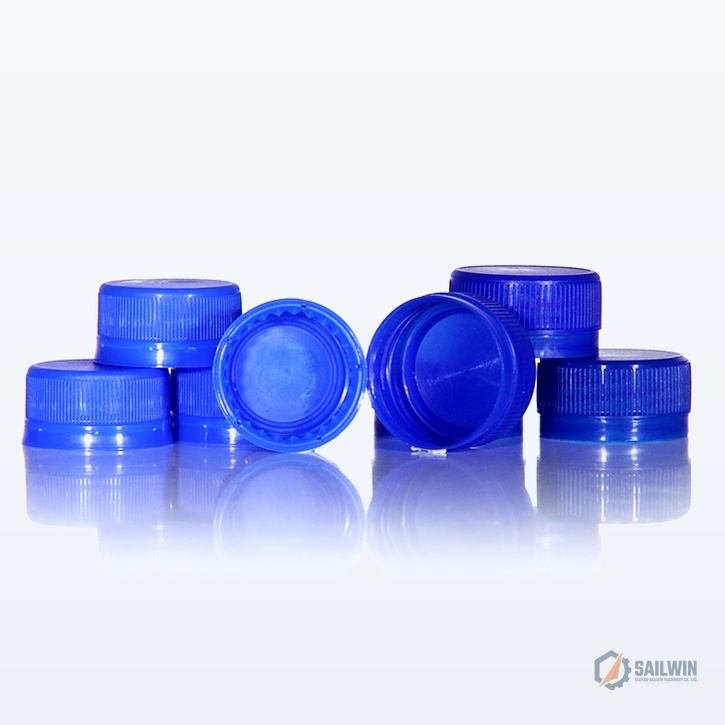
Royal Blue 28mm PCO 1881 Screw Caps
Precision outer knurling ribs provide excellent high-speed chuck grip, preventing cap slippage on 48,000 BPH automated bottling lines.
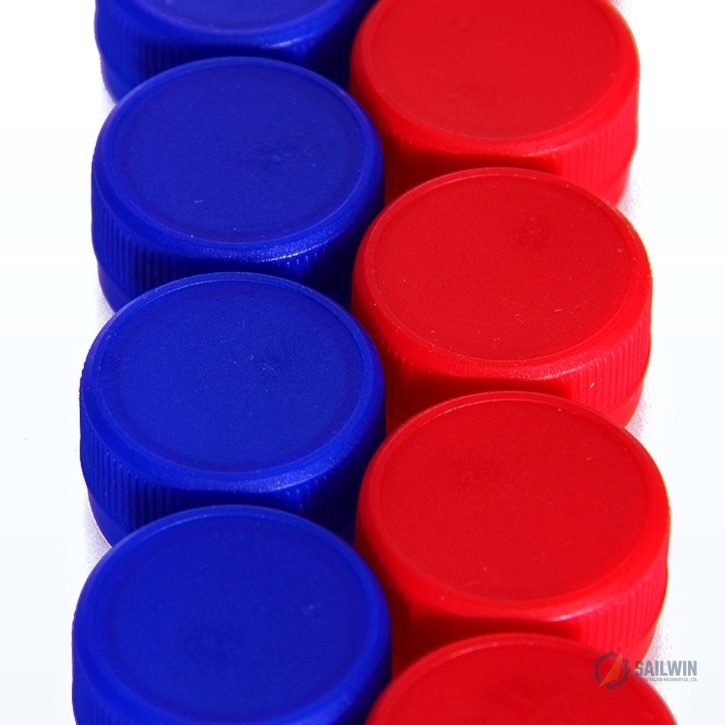
Dual-Row Blue & Red Water Caps
Featherweight 29/25 and 30/25 short-height closures (weight ≤ 1.05g), saving over 20% resin material costs for mineral water bottlers.
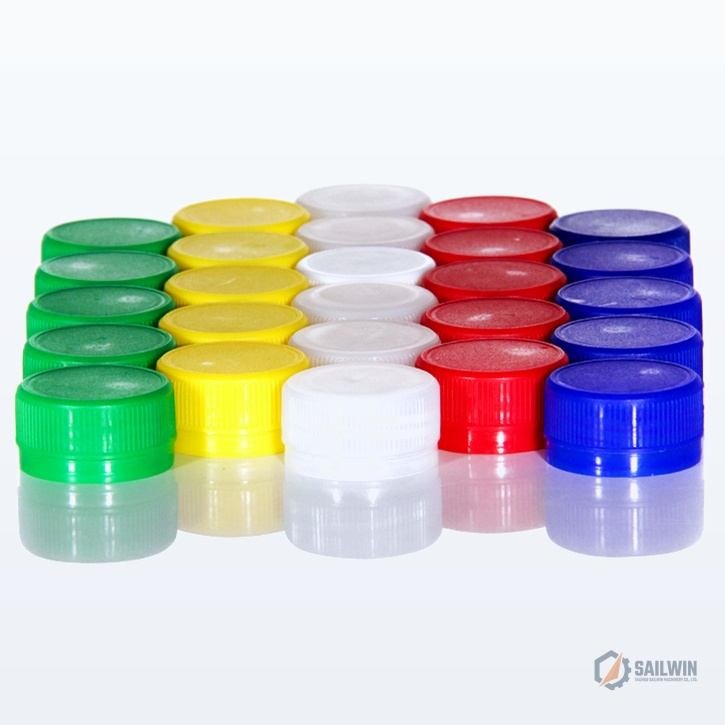
5x5 Grid Array of Beverage Closures
Balanced multi-cavity injection ensures uniform color dispersion, zero gate blushing, and identical dimensions across all production batches.
Matching Turnkey Tooling Sub-Pages
Explore matching blow molds, preform tooling, and parent category collection hubs.
Water & Beverage Bottle Blow Molds
Alloy 7075-T6 stretch blow molds engineered with matching neck lock rings for 2,200 BPH/cavity high-speed lines.
PET Preform Injection Molds
8 to 96 cavity valve-gate hot runner preform molds engineered with dual-taper self-locking for sub-0.05mm eccentricity.
Plastic Injection Molds Hub
Explore our complete injection mold engineering portfolio covering 9 specialized cap types, preforms, and technical housings.
PET Bottle Blow Molds Hub
Comprehensive stretch blow mold catalog for water, CSD, wide-mouth jars, cosmetic containers, and 5-gallon bottles.

